
How Much Oil Does a 60 Gallon Air Compressor Take: Practical Guide for 2026
Find out how much oil does a 60 gallon air compressor take, exact crankcase capacities, oil types, and oil change steps for October 2026.
 By Tony Carrick
Updated October 8, 2026

Workshop mechanics and garage fabricators rely on stationary air compressors to deliver continuous CFM for impact wrenches, plasma cutters, and paint spray guns. However, new owners often get confused when refilling lubricant, mistakenly wondering how much oil does a 60 gallon air compressor take after seeing the massive volume listed on the tank label. The tank capacity measures air storage volume rather than liquid fluid capacity, meaning the pump crankcase actually holds a small fraction of that total number. Confusing air volume with crankcase capacity can lead to severe equipment damage or messy fluid overflows.
Adding excessive fluid can blow out seals and contaminate air delivery lines, while starving the pump causes catastrophic bearing failure and cylinder scoring. Using the correct viscosity and consulting a reliable compressor oil selection guide ensures cast-iron pump assemblies operate at stable temperatures without breaking down under continuous load. Understanding exact crankcase requirements protects your workshop investment and keeps pneumatic equipment running reliably for thousands of operating hours.
| Award | Product | ACR Score About ACR ScoreThe ACR Score is our own rating from 0 to 10, based on performance, design and build, ease of use, and value. It reflects independent research and is never influenced by manufacturers, retailers, or affiliate commissions. Learn more › | |
|---|---|---|---|
| Best Overall |
Mag 1 1-Gallon Air Compressor Oil
|
9.2/10 | Buy |
| Best Budget |
 Triax Kompressor ISO 46 SAE 20 Full Synthetic Air |
9.1/10 | Buy |
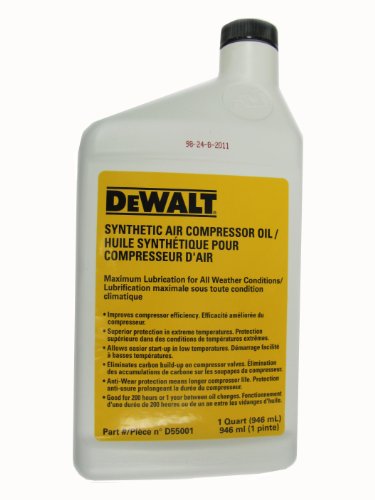 DeWalt D55001 1-Quart Compressor Oil |
9.1/10 | Buy | |
| Best Premium |
 Triax Kompressor ISO 100 SAE 30 Oil (5 Gal) |
9.1/10 | Buy |
 Campbell Hausfeld 60-Gallon Air Compressor |
8.9/10 | Buy | |
| Best Value |
 Milton 1002 SAE 30W Compressor Oil, 1 Gallon |
8.8/10 | Buy |
 TRIAX Kompressor ISO 46 SAE 20 Full Synthetic Air |
8.8/10 | Buy | |
 TRIAX Kompressor ISO 68 Full Synthetic Air |
8.6/10 | Buy | |
 Triax Kompressor ISO 46 Compressor Oil (5 Gal) |
8.3/10 | Buy | |
 MAG 1 Air Compressor Oil 16 oz |
7.8/10 | Buy |
Mag 1 1-Gallon Air Compressor Oil
Formulated for reliable workshop maintenance, Mag 1 Air Compressor Oil uses refined petroleum base stocks paired with anti-foam additives to maintain stable lubrication. The generous one-gallon volume makes it a practical choice for keeping reciprocating or stationary compressors running smoothly over time.
Pros
- Anti-foam additives maintain steady lubrication
- Refined petroleum stocks promote smooth operation
- Formula helps extend compressor service life
- Generous 1-gallon volume handles multiple refills
Cons
- Jug weighs 7.25 pounds and can be heavy to pour
- One-gallon size may exceed small top-off needs
Triax Kompressor ISO 46 SAE 20 Full Synthetic Air
Triax Kompressor ISO 46 SAE 20 is a commercial-grade, full synthetic non-detergent compressor oil engineered for oil-lubricated reciprocating, rotary screw, and vane pumps operating in temperatures from -49°F to over 140°F. It provides exceptional thermal protection and extended component life for garage mechanics and shop owners maintaining heavy-duty pneumatic systems.
Pros
- Extreme all-weather operating range from -49°F to 140°F+ prevents cold-start motor stalling and high-heat viscosity breakdown
- Non-detergent full synthetic formula protects internal bearings and provides up to 20,000 hours of service longevity
- Lowers operating pump temperatures by 30% and actively sheds condensation to prevent internal crankcase rust
- Compatible with oil-lubricated reciprocating, rotary screw, and rotary vane compressor pumps from major manufacturers
Cons
- Not suitable for oil-free or maintenance-free dual-piston compressor designs that do not use crankcase oil
- Explicitly prohibited for use in breathing air systems, oxygen compressors, or liquid natural gas (LNG) units
- Single-quart volume may require purchasing multiple bottles for larger stationary 60-gallon or 80-gallon shop pump crankcases
DeWalt D55001 1-Quart Compressor Oil
Formulated for regular air compressor maintenance, the DeWalt D55001 comes in a handy one-quart bottle to keep pump components operating smoothly. It is a solid choice for workshops and job sites running oil-lubricated compressors that require dedicated manufacturer-grade fluid.
Pros
- Convenient 1-quart size for routine maintenance
- OEM formulation from an established tool brand
- Compact bottle design stores easily
Cons
- Not applicable for oil-free compressor models
- May require multiple bottles for high-capacity industrial tanks
Triax Kompressor ISO 100 SAE 30 Oil (5 Gal)
Engineered for rotary, vane, screw, and reciprocating systems, this industrial-grade synthetic fluid provides up to 20,000 hours of continuous service across extreme temperatures. Its non-detergent formula lowers operating heat by 30 percent while guarding vital bearings against friction and moisture.
Pros
- Extended 20,000-hour life span minimizes maintenance cycles
- Reliable all-season operation across wide temperature swings
- Substantially reduces operating temperatures and oil burnoff
- Non-detergent blend prevents bearing wear and vibration
Cons
- Not compatible with oxygen air or LNG compressors
- Large 5-gallon volume exceeds small workshop requirements
Campbell Hausfeld 60-Gallon Air Compressor
Built for demanding garage and workshop tasks, this stationary compressor combines a 3.7 HP motor with a two-stage cast-iron pump reaching 175 PSI. It provides steady airflow to support high-demand air tools like sprayers, grinders, and sanders.
Pros
- High 175 PSI maximum output pressure
- Durable cast-iron pump rated for longevity
- Large 60-gallon capacity supports sustained pneumatic tool use
- Vertical tank design saves workshop floor space
Cons
- Requires a dedicated 230V to 240V electrical connection
- Heavy 255-pound stationary build is difficult to move
Milton 1002 SAE 30W Compressor Oil, 1 Gallon
Milton 1002 is a non-detergent ISO-100 SAE 30W conventional lubricant engineered specifically for reciprocating air compressors. The one-gallon capacity makes it a sensible option for regular workshop equipment upkeep.
Pros
- Non-detergent formula tailored for reciprocating compressors
- Standard ISO-100 SAE 30W viscosity rating
- Generous one-gallon volume covers multiple refills
Cons
- Conventional mineral formula instead of synthetic blend
- Heavy container can be awkward to pour directly
TRIAX Kompressor ISO 46 SAE 20 Full Synthetic Air
TRIAX Kompressor ISO 46 SAE 20 is a commercial-grade, full-synthetic non-detergent lubricant engineered for oil-lubricated reciprocating, rotary screw, and vane air compressors. It provides reliable extreme-temperature wear protection and multi-viscosity all-season performance, making it an excellent maintenance choice for auto shops, contractors, and home garage workshops.
Pros
- Full synthetic non-detergent formulation extends pump life across severe operating conditions
- True all-season multi-viscosity rating maintains fluid flow from -49 deg F up to 140 deg F+
- Formulated to lower operating temperatures by up to 30% and eliminate oil vapor odor
- Compatible with a wide array of compressor pumps including reciprocating and rotary screw designs
Cons
- Not formulated for oil-free air compressors, breathing air systems, oxygen setups, or LPG gas pipelines
- Users must verify whether their pump manufacturer specifically calls for ISO 46 (SAE 20) rather than heavier ISO 68 or ISO 100 weights
- Requires careful manual crankcase draining and filling without an included pour spout
TRIAX Kompressor ISO 68 Full Synthetic Air
TRIAX Kompressor ISO 68 is a commercial-grade, full synthetic compressor lubricant engineered for oil-lubricated reciprocating, rotary screw, and vane pumps operating between -49°F and 140°F+. It is an excellent maintenance solution for auto mechanics, shop owners, and contractors seeking lower pump operating temperatures and up to 20,000 hours of service life.
Pros
- Extended 20,000-hour service life minimizes routine maintenance intervals on high-demand shop compressors
- All-season stability from -49°F to 140°F+ prevents cold-morning motor drag and high-heat viscosity breakdown
- Non-detergent formulation separates condensation cleanly to safeguard internal crankcase bearings
- Broad compatibility across major reciprocating, rotary screw, and rotary vane compressor manufacturers
Cons
- Not suitable for maintenance-free oil-free compressor designs or oxygen and Liquid Natural Gas (LNG) systems
- One-gallon container size exceeds the immediate refill capacity of small single-stage DIY splash-lube pumps
Triax Kompressor ISO 46 Compressor Oil (5 Gal)
Formulated for severe commercial applications, this full-synthetic ISO 46 lubricant delivers up to 20,000 service hours across rotary, screw, and reciprocating compressors. It maintains a stable protective film in temperatures ranging from sub-zero cold to extreme heat while actively repelling water.
Pros
- Service life rated for over 20,000 operational hours
- Wide operating range from -49°F to over 140°F
- Compatible with major commercial compressor pump designs
- Water-repelling non-detergent formula reduces internal friction
Cons
- Not suitable for oxygen or LNG compression systems
- Heavy 37-pound container can be awkward to pour
MAG 1 Air Compressor Oil 16 oz
MAG 1 Air Compressor Oil is a specialized 16-ounce petroleum lubricant formulated with anti-foam agents and rust inhibitors to protect oil-lubricated compressor pumps under heavy operating conditions. It offers essential wear protection and thermal stability for home garage hobbyists, auto mechanics, and shop owners maintaining oil-lubricated pneumatic equipment.
Pros
- Formulated specifically for compressor pump crankcases rather than generic detergent automotive motor oils
- Anti-foam chemistry helps prevent oil foaming and maintains steady lubrication under rapid piston strokes
- Helps protect internal metal components against rust and oxidation caused by ambient moisture buildup
- Convenient 16-ounce bottle size fits easily into garage maintenance cabinets and tool chests
Cons
- Not suitable for maintenance-free oil-free air compressors
- A 16-ounce volume may require multiple bottles for larger stationary multi-stage shop compressors with high crankcase capacities
Essential Oil Capacity and Lubrication Guide for 60-Gallon Compressors
Stationary workshops depend on heavy-duty reciprocating pumps to feed consistent air volume to demanding pneumatic tools. When determining how much oil does a 60 gallon air compressor take, understanding pump architecture is critical because the air tank capacity does not dictate lubricant volume. Most heavy cast-iron pumps attached to 60-gallon tanks require between 16 and 48 fluid ounces of oil, depending on cylinder configuration and crankcase displacement.
Tank Capacity Versus Crankcase Volume: The Core Distinction
First-time owners of stationary compressors frequently confuse air storage ratings with pump fluid reservoirs. A 60-gallon rating refers exclusively to the internal volume of the steel pressure vessel designed to store compressed air. The cast-iron reciprocating pump mounted to the top plate of the tank features its own independent crankcase that functions similarly to an engine block. That crankcase holds only enough fluid to submerge the lower tips of the connecting rods during their rotational stroke.
Pouring gallons of lubricant into an air compressor would either flood the compressed air cylinder or overflow the breather vent, creating severe operational hazards. In reality, the crankcase reservoir is relatively compact, designed to lubricate the crankshaft, connecting rod journals, and wrist pins via splash lubrication. Maintaining the proper fluid level ensures splash dippers can atomize oil across the cylinder walls without creating excessive hydrodynamic drag. Proper oil distribution coats the cylinder sleeve evenly, reducing friction and preserving the integrity of the piston rings under high heat.
Single-Stage Versus Two-Stage 60-Gallon Oil Capacities
Pump architecture plays the largest role in determining exact fluid capacity on a stationary workshop machine. Many entry-level 60-gallon compressors feature single-stage twin-cylinder pumps designed to reach 135 to 150 PSI maximum pressure. These compact single-stage cast-iron pumps typically require between 16 and 24 fluid ounces (roughly 0.5 to 0.75 quarts) of oil to reach the proper operating mark. Smaller single-stage crankcases circulate less total fluid because the rotational assembly experiences lower overall compression resistance.
Heavy-duty commercial units, such as the Campbell Hausfeld 60-Gallon 2-Stage Air Compressor, utilize larger two-stage pump assemblies engineered for 175 PSI maximum working pressure. Because two-stage configurations feature distinct low-pressure and high-pressure cylinders, their heavy-duty crankcases and oversized crankshaft journals require more fluid volume. Comparing two-stage and single-stage compressor pump configurations reveals that two-stage units generally hold between 32 and 48 fluid ounces (1 to 1.5 quarts) of lubricant. The larger fluid volume helps buffer the intense mechanical friction created by compounding pressure across sequential cylinders.
Larger pump castings require this additional fluid reserve to manage the higher operating temperatures produced during second-stage air compression. A larger oil sump also allows contaminants and minute wear particles to settle safely at the bottom of the pan away from moving bearings. Before pouring oil into any pump, checking the manufacturer technical plate on the shroud or pump casting provides the precise model-specific fluid specification.
Visual Verification: Sight Glasses and Dipstick Readings
While manufacturer specification sheets list fluid capacity in ounces, visual verification is the only reliable method for preventing fill errors. Most modern cast-iron pumps incorporate a clear brass-threaded sight glass located near the base of the crankcase. The optimal oil level aligns directly with the center of the glass, usually indicated by an embossed red dot or reference circle. Allowing the oil level to drift above or below this central indicator compromises pump efficiency and increases maintenance frequency.
Some industrial compressors employ a traditional threaded dipstick integrated into the crankcase breather cap instead of a sight glass. When reading a dipstick, thread engagement matters because threading the plug fully down versus resting it on the collar alters the level reading. Always wipe the dipstick with a lint-free cloth, insert it according to manufacturer guidelines, and ensure the oil film rests squarely between the minimum and maximum crosshatch indicators. Confirming the oil level on a level surface eliminates angle distortion that could cause inaccurate fluid assessments.
The Severe Mechanical Risks of Overfilling and Underfilling
Overfilling an air compressor crankcase is a widespread mistake that causes immediate mechanical complications. When fluid rises above the sight glass centerline, the spinning crankshaft counterweights strike the oil surface with excessive force. This aggressive churning whips air into the oil, creating foam that destroys fluid film strength and starves connecting rod bearings of effective lubrication. Foamed lubricant cannot support hydrodynamic loads, resulting in premature wear on precision-machined journal surfaces.
Aerated oil also expands dramatically in volume, forcing liquid lubricant upward past the compression rings and into the valve plate assembly. Once oil enters the compression chamber above the piston, it atomizes directly into the compressed air discharge line. This heavy oil blow-by ruins paint spray finishes, gums up pneumatic nailers, and clogs sensitive pressure regulator diaphragms downstream. If you accidentally pour too much lubricant into the crankcase, open the lower drain plug immediately and drain the excess until the sight glass indicates the correct middle level.
Operating a stationary compressor with insufficient crankcase fluid leads to rapid thermal degradation and catastrophic mechanical seizure. Because splash-lubricated pumps rely on dippers mounted on connecting rod caps, low oil levels prevent these dippers from reaching the fluid pool. Without consistent splashing, wrist pins, cylinder walls, and main bearings experience immediate dry friction and severe heat buildup. Inspecting the crankcase level prior to every extensive workshop session is the single most effective way to prevent premature pump failure.
Selecting the Right Lubricant Viscosity and Formula
Air compressor pumps operate under distinct thermal conditions that make standard automotive engine oils completely inappropriate. Automotive motor oils contain detergent packages designed to suspend combustion soot, which causes moisture and carbon to emulsify in a compressor crankcase. Compressor pumps require non-detergent lubricants that allow moisture to separate cleanly and settle to the sump floor where it cannot harm internal iron components. Detergent additives also promote carbon formation on reed valves, which leads to valve leakage and reduced pump efficiency over time.
Viscosity selection depends heavily on ambient garage temperatures and pump duty requirements. For temperate workshop environments between 40 and 100 degrees Fahrenheit, an ISO 100 or SAE 30 non-detergent oil, such as Milton 1002 High Performance Conventional Oil, provides excellent hydrodynamic film strength. In cold-weather settings where garages drop below freezing, lighter ISO 46 or SAE 20 formulations, such as TRIAX Kompressor Full Synthetic, allow easy electric motor startup without overloading the breaker. Heavy-load applications operating in hot ambient environments often benefit from ISO 68 formulations that maintain viscosity under continuous run cycles.
Synthetic compressor oils provide superior resistance to thermal breakdown, carbon buildup on discharge valves, and sludge formation compared to standard mineral basestocks. Formulations like Mag 1 Air Compressor Oil or TRIAX Kompressor ISO 100 feature anti-foam and anti-wear additives tailored for reciprocating compressors. High-grade synthetic oils also resist vaporization, significantly reducing oil carryover into downstream shop air systems and extending pump service life.
Step-by-Step Oil Change Procedure for Stationary Compressors
Executing a proper oil change requires basic preparation to avoid spills and ensure complete fluid removal. Begin by running the compressor under light load for five to ten minutes to warm the crankcase lubricant, which suspends accumulated particulates and lowers viscosity for easier drainage. Once warm, disconnect the primary 230V electrical breaker or unplug the unit, and depressurize the air tank completely through the bottom drain valve. Disconnecting power guarantees the motor will not unexpectedly cycle on while your hands are working near the pulleys or drain ports.
Position a shallow drain pan beneath the crankcase drain plug, which is typically situated directly below the oil sight glass. Thread out the square-head brass drain plug carefully using an appropriate wrench, allowing warm oil to drain completely into the catch container. Inspect the magnetic tip of the plug, if equipped, for fine metallic debris, wiping it clean before reinstalling and securing the plug snugly into the pump casting. Applying a fresh wrap of PTFE thread sealant prevents slow oil seepage around the drain threads once the crankcase is refilled.
Remove the top breather cap or fill plug and insert a clean, narrow-neck funnel into the fill port. Slowly pour the specified non-detergent lubricant into the crankcase, pausing periodically to let the oil settle and observe the sight glass. Stop pouring as soon as the fluid reaches the halfway mark on the sight glass, reinstall the breather cap securely, and wipe down any incidental drips from the pump housing.
Break-In Schedules and Long-Term Service Intervals
New 60-gallon compressors require a dedicated break-in protocol to allow piston rings and cylinder hone patterns to mate properly. During initial assembly, minute cast-iron machining dust and wear particles naturally slough off internal surfaces and mix with the factory oil. Operating the compressor with an open tank drain for thirty minutes allows the pump to seat without building backpressure, after which the initial oil charge should be changed after roughly 20 to 50 operating hours. Performing that initial flush removes metallic debris before it can circulate through the connecting rod bearings and cause micro-grooving.
Following the initial break-in period, conventional petroleum compressor oils generally require replacement every 200 to 300 operating hours or every six months, whichever arrives first. Premium full synthetic lubricants, by contrast, feature robust oxidation resistance that can extend change intervals up to 500 or even 1,000 hours in clean workshop environments. In unheated garages with high seasonal humidity swings, changing fluid semi-annually prevents water condensation from causing crankcase corrosion. Routine oil sampling or visual inspection through the sight glass helps identify oil breakdown before service intervals lapse.
Regular maintenance must also include inspecting the intake air filters, because abrasive shop dust entering the cylinder contaminates the crankcase oil rapidly. Combining routine oil maintenance with draining water from air delivery lines preserves both the mechanical pump and your downstream pneumatic tools. Keeping a written log on the compressor belt guard tracking operating hours and oil change dates ensures the machine remains properly protected throughout its operational lifespan.
Diagnosing Discolored, Milky, or Rapidly Consumed Oil
Monitoring the appearance of pump oil through the sight glass provides crucial insight into the mechanical health of your stationary compressor. Fresh compressor oil should appear clear to light amber in color, allowing you to see through the sight glass easily. If the oil takes on a milky, cloudy, or mayonnaise-like appearance, moisture has condensed inside the crankcase and emulsified with the lubricant. This moisture buildup happens when warm compressed air cools inside an unheated crankcase, creating internal condensation during humid weather.
Milky oil typically occurs when a compressor runs for very short cycles in a cold garage, never reaching sufficient operating temperatures to evaporate internal condensation. To remedy this issue, drain the emulsified fluid immediately, refill with fresh non-detergent oil, and run the compressor under load long enough to achieve normal operating temperature. If the oil turns dark black or smells burnt, excessive heat or carbon blow-by is breaking down the lubricant, signaling worn piston rings or restricted cooling fins. Dark, oxidized oil loses its protective boundary layer quickly, necessitating an immediate flush to protect the pump crankshaft.
Rapid oil consumption, where the fluid level drops noticeably between weekly checks, indicates severe blow-by, failed crankcase seals, or an overfilled sump. Inspect the exterior of the pump for seeping gaskets around the end plates and check the air discharge line for excessive liquid oil pooling. Addressing oil loss promptly prevents sudden dry seizures and ensures your 60-gallon workshop compressor delivers clean, dependable pneumatic power for years to come.
Keeping a 60-gallon air compressor properly lubricated comes down to respecting the small crankcase volume rather than the large air tank rating. Measuring out between 16 and 48 fluid ounces of high-quality non-detergent compressor oil and verifying the sight glass midpoint prevents both oil foaming and dry pump seizures. Establishing a consistent routine of checking fluid levels, purging tank condensation, and changing oil on schedule ensures your stationary equipment provides dependable workshop air for decades.
About the author
Tony Carrick is an experienced product researcher and writer specializing in tools, home improvement, automotive maintenance, and consumer equipment. With extensive experience reviewing tools and tackling hands-on renovation projects, he brings a buyer-focused perspective to compressor performance, usability, and overall value.