
How Oil Free Air Compressor Works: Practical Guide for 2026
Learn how oil free air compressor works to deliver clean air for pneumatic tools without pump maintenance this October 2026.
 By Glenda Taylor
Updated October 8, 2026

Pneumatic tools require a dependable supply of pressurized air to drive fasteners, inflate tires, and operate spray equipment, but traditional workshop setups often introduce maintenance headaches. Understanding how oil free air compressor works helps DIY enthusiasts and finish carpenters select equipment that operates cleanly without the threat of lubricant mist ruining wood finishes or paint surfaces. Unlike heavy cast-iron pumps that depend on an internal oil bath, oil-free designs utilize advanced synthetic coatings and pre-lubricated components to generate compression. This design eliminates routine oil changes and prevents messy spills when moving a portable unit between jobsites or storing it in a residential garage.
While contractors frequently debate the trade-offs between zero-maintenance convenience and long-term industrial durability, modern dry-compression systems have narrowed that gap considerably. Modern compact units deliver impressive pressure ratings while minimizing operational sound through precision-machined cylinders and dual-piston configurations. Exploring the differences between dry pumps and traditional oil-lubricated compressor designs highlights why maintenance-free pumps have become the primary choice for mobile finish trim crews and home hobbyists alike. Understanding these internal mechanics ensures you operate your compressor within its proper duty cycle while getting the most airflow out of every cycle.
| Award | Product | ACR Score About ACR ScoreThe ACR Score is our own rating from 0 to 10, based on performance, design and build, ease of use, and value. It reflects independent research and is never influenced by manufacturers, retailers, or affiliate commissions. Learn more › | |
|---|---|---|---|
| Best Overall |
Baococo 4-Gallon 0.5 HP Air Compressor
|
9.2/10 | Buy |
| Best Value |
 BairDplusL 8 Gallon Ultra Quiet Air Compressor |
9.2/10 | Buy |
 Goodyear 6-Gallon 150 PSI Portable Oil-Free |
9.2/10 | Buy | |
| Best Premium |
 Stealth SAQ-1234 2-Gallon Air Compressor |
9.2/10 | Buy |
| Best Budget |
 Limodot 8-Gallon Quiet Air Compressor |
9.1/10 | Buy |
 Metabo HPT 6-Gallon Pancake Air Compressor Review |
8.6/10 | Buy | |
 FORNAX 6-Gallon Pancake Air Compressor |
8.4/10 | Buy | |
 VEVOR 2HP Oil-Free Air Compressor Motor |
8.4/10 | Buy | |
 DEWALT DWFP55130 2.5-Gallon 200 PSI Quiet Trim Air |
8.4/10 | Buy | |
 VELPAX 2.4-Gallon Quiet Air Compressor |
8.1/10 | Buy |
Baococo 4-Gallon 0.5 HP Air Compressor
Built for light household maintenance and quick inflation tasks, this compact 4-gallon unit pairs a quiet 0.5 HP motor with an automatic overpressure safety shut-off. Its modest air delivery handles small nailers and tire filling without creating excessive workshop noise.
Pros
- Quiet operation suitable for residential spaces
- Automatic overpressure shut-off enhances operational safety
- Compact footprint stores easily in tight spaces
- Stable base minimizes movement during use
Cons
- Low airflow output limits heavy pneumatic tool use
- Maximum pressure capped at 110 PSI
- Modest 0.5 HP motor lacks heavy-duty capability
BairDplusL 8 Gallon Ultra Quiet Air Compressor
The BairDplusL 8-Gallon Ultra Quiet Air Compressor features a 1.5 HP oil-free motor and dual silencers to deliver a listed 8.75 CFM at 115 PSI while keeping operational noise at a modest 70 dB. It offers quick 45-65 second recovery times, making it a reliable option for DIYers and woodworkers running nailers, screwdrivers, and light spray equipment.
Pros
- Noticeably quiet 70 dB operation helps reduce auditory fatigue in enclosed garage or basement workspaces
- Quick 45 to 65 second tank recovery minimizes waiting during cyclic pneumatic tool operations
- Oil-free 1.5 HP pump design eliminates routine oil changes and avoids lubricant mist in downstream air lines
- Compact 35-pound weight and 10 x 22 x 22 inch footprint make it easy to transport and store
Cons
- Maximum operating pressure tops out at 115 PSI, which may fall short for tools requiring 125 to 150 PSI
- The product description lists both 8-gallon and 9-gallon tank capacities, creating slight sizing ambiguity
- Coupler style, regulator port sizes, and discharge fitting standards are not specified in the manufacturer documentation
Goodyear 6-Gallon 150 PSI Portable Oil-Free
The Goodyear 6-gallon pancake air compressor delivers 3 SCFM at 90 PSI and 150 max PSI powered by a reliable 1 HP induction motor. At 32 pounds with an oil-free pump, it provides dependable portable air for trim carpenters, DIY home projects, and garage tire inflation.
Pros
- Produces 3 SCFM at 90 PSI, offering solid airflow for sequential finish nailing and light framing tasks
- Equipped with a durable 1 HP induction motor for dependable and consistent pressure build-up
- Oil-free pump mechanism requires zero ongoing lubrication maintenance and prevents oil contamination in air lines
- Two clearly visible analog pressure gauges make monitoring regulated line pressure straightforward
- Compact 32-pound pancake design is easy to lift, load into vehicles, and store on shop shelves
Cons
- Airflow rating of 3 SCFM is not designed to support continuous rotary air tools like orbital sanders or paint sprayers
- Comes with a single 1/4-inch quick-connect coupler rather than dual outlets for running two tools simultaneously
- Sold as a bare compressor without an included air hose, tire inflator chuck, or pneumatic nail guns
Stealth SAQ-1234 2-Gallon Air Compressor
Operating at under 60 decibels, this compact unit provides exceptionally quiet performance for garage DIY tasks, brad nailing, and tire inflation. Its oil-free motor reaches up to 125 PSI while keeping routine maintenance to a minimum.
Pros
- Quiet operation suitable for indoor workspaces
- Maintenance-free oil-free pump design
- Durable steel tank with rubber vibration dampening
- Reliable pressure recovery for intermittent nailing
Cons
- Relatively heavy to carry at nearly 42 pounds
- Small two-gallon tank limits continuous tool use
- Modest 1.8 CFM flow rate at 90 PSI
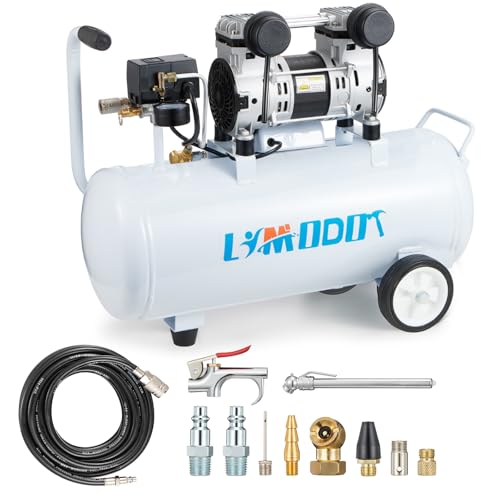
Limodot 8-Gallon Quiet Air Compressor
Limodot pairs an 8-gallon capacity with a quiet 68-decibel motor, keeping noise disruption low during indoor trim or workshop jobs. Delivering 2.8 CFM at 90 PSI alongside a quick 30-second recovery time, it provides steady airflow for DIY pneumatic tools without messy oil maintenance.
Pros
- Low 68 dB output prevents loud workshop disruption
- Fast 30-second pressure recovery keeps projects moving
- Oil-free pump eliminates messy oil changes
- Comprehensive 11-piece accessory kit included out of the box
- Integrated wheels make moving the 8-gallon tank easy
Cons
- 2.8 CFM output limits high-demand continuous tools
- Included PVC hose is stiffer than rubber alternatives
Metabo HPT 6-Gallon Pancake Air Compressor Review
The Metabo HPT EC711S is a portable 6-gallon pancake air compressor delivering 2.8 CFM at 90 PSI with a 165 PSI tank ceiling and an operating sound level of 73 dB. With its quick 46-second recovery cycle and dual quick couplers, it is an excellent choice for finish carpenters, punch-list contractors, and DIYers running pneumatic nailers.
Pros
- 73 dB operational sound rating is substantially quieter than standard job-site pancake units
- 165 PSI maximum pressure provides ample air storage with a swift 46-second recovery cycle
- Two 1/4-inch universal quick couplers support multi-tool setups right out of the box
- Sturdy steel roll cage protects gauges and the manifold assembly against knocks and drops
- Oil-free 1.0 HP motor ensures low maintenance and reliable cold-weather motor startup
Cons
- At 38.5 lbs, it is slightly heavier than ultra-compact 1-to-3-gallon trim compressors
- Airflow of 2.8 CFM at 90 PSI is designed for intermittent fastening, not continuous rotary tools or paint sprayers
- Bare-tool configuration means air hoses and pneumatic fastening tools must be purchased separately
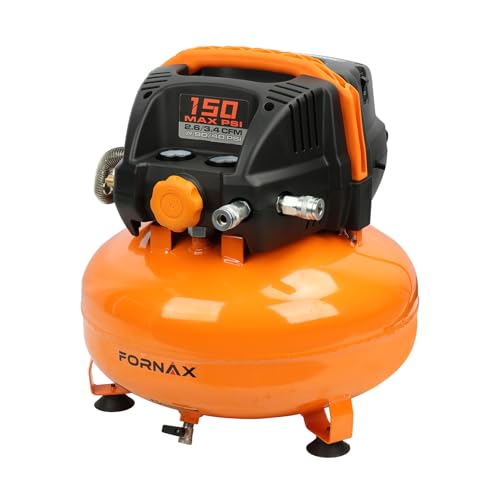
FORNAX 6-Gallon Pancake Air Compressor
The FORNAX 6-Gallon Pancake Air Compressor delivers 2.6 CFM at 90 PSI and up to 150 PSI of maximum pressure, featuring dual couplers and a lightweight 28.8-pound portable footprint. It is a practical pneumatic power source for DIY homeowners, finish carpenters, and garage hobbyists driving nailers or managing tire inflation.
Pros
- Dual quick-connect couplers allow two nailers to operate simultaneously without adding an external splitter manifold
- Generous 6-gallon air tank capacity with a 150 PSI maximum pressure ceiling provides a dependable air reserve
- Lightweight 28.8-pound profile simplifies one-handed carrying up stairs and transport into work vans
- Maintenance-free oil-free pump eliminates oil checks, oil changes, and mess around finished work surfaces
Cons
- Operating sound output rated at 95 dBA is loud and makes hearing protection necessary, especially in closed rooms
- Airflow output of 2.6 CFM at 90 PSI cannot support continuous-demand tools like sanders, grinders, or paint sprayers
- Supplied as a bare-tool compressor without an included air hose, tire inflator chuck, or pneumatic nailers
VEVOR 2HP Oil-Free Air Compressor Motor
Delivering 5.2 CFM at 90 PSI with a 1680 RPM motor, this oil-free VEVOR pump head provides clean, low-maintenance air output for garage shops and pneumatic tools. Its cold-rolled steel build and dedicated cooling fans make it a dependable drop-in motor for woodworking, spray painting, and automotive repairs.
Pros
- Low-maintenance oil-free operation
- Generates 5.2 CFM at 90 PSI
- Sturdy steel and aluminum construction
- Effective cooling via built-in fans and heat sinks
Cons
- Heavier unit at over 36 pounds to install
- Single-stage design limits peak pressure to 145 PSI
- At 78 dB, operating volume is still noticeable indoors
DEWALT DWFP55130 2.5-Gallon 200 PSI Quiet Trim Air
The DEWALT DWFP55130 delivers a capable 3.0 SCFM at 90 PSI with a 200 max PSI 2.5-gallon tank, running at a quiet 71.5 dBA on an efficient 12-amp motor. It is an ideal pneumatic power source for trim carpenters, punch-list contractors, and DIYers working on residential circuits.
Pros
- Delivers 3.0 SCFM at 90 PSI with a high 200 max PSI ceiling for rapid pressure recovery during sequential fastening
- Quiet 71.5 dBA sound output makes indoor trim carpentry and remodeling far less disruptive to homeowners
- Low 12-amp draw reduces breaker trips when running on shared 15-amp household circuits
- Integrated roll cage and console protect critical components while supporting horizontal or vertical operation
- Dual quick couplers allow two trim carpenters to connect and work off a single compressor
Cons
- Bare-tool configuration means you must supply your own air hoses, couplers, and pneumatic nail guns
- At 36 pounds, it is heavier to haul up flights of stairs than ultra-compact 1-gallon finish compressors
- Air output of 3.0 SCFM is built for intermittent finish fastening and will not support continuous tools like rotary sanders or sprayers
VELPAX 2.4-Gallon Quiet Air Compressor
Operating at roughly 60 decibels, this portable compressor provides steady air pressure for garage tasks, tire inflation, and trim carpentry without excessive noise. Its oil-free 1.5 HP motor keeps routine upkeep minimal while the integrated handle makes transport between work areas easy.
Pros
- Very quiet operation at roughly 60 dB
- Maintenance-free oil-less pump design
- Compact build with convenient carry handle
- Integrated overload protection and safety release valve
Cons
- Small 2.4-gallon tank limits continuous high-demand tool use
- Modest 115 PSI ceiling restricts heavy industrial applications
Inside the Mechanics: The Engineering Behind Oil-Free Air Compression
At its core, an oil-free air compressor functions by drawing ambient atmospheric air into a cylinder, compressing that air with a reciprocating piston, and forcing it into a steel storage tank without using liquid oil for lubrication. Traditional reciprocating compressors rely on an oil sump in the crankcase where splash lubrication coats the cylinder walls, crankshaft journals, and wrist pins to mitigate friction and manage operating temperatures. In contrast, an oil-free pump eliminates the liquid oil reservoir entirely by incorporating self-lubricating synthetic materials directly onto the mechanical friction surfaces. This structural shift transforms how the pump manages friction, controls extreme compression heat, and delivers clean, particulate-free air to downstream pneumatic equipment.
Self-Lubricating Piston Sleeves and Low-Friction Rings
Reciprocating pistons generate immense mechanical friction and heat as they cycle up and down thousands of times each minute inside the cylinder. In an oil-free system, the traditional cast-iron cylinder sleeve and steel compression rings are replaced with specialized materials engineered to slide smoothly without fluid lubrication. Most modern oil-free compressor pumps feature a cylinder sleeve coated with a low-friction surface, paired with a piston ring made from polytetrafluoroethylene, commonly known as PTFE or Teflon. This PTFE ring is flexible, heat-resistant, and intentionally designed to wear at an ultra-slow, predictable rate while maintaining an airtight dynamic seal against the cylinder wall.
As the electric motor drives the piston upward during the compression stroke, the PTFE ring expands outward slightly against the cylinder bore to trap air above the piston crown. Because PTFE possesses an exceptionally low coefficient of friction, the piston moves smoothly without galling or seizing against the metal sleeve. Unlike standard automotive-style split rings that allow a tiny fraction of blow-by, oil-free piston rings are often formed as a continuous cup or beveled ring that flexes to maintain constant wall contact. This dry-sealing capability allows portable pancake and hot dog compressors to achieve maximum operating pressures reaching 135 to 200 PSI without requiring a single drop of lubricant.
Sealed Precision Bearings and Crankcase Isolation
Eliminating the crankcase oil bath introduces another engineering challenge because the crankshaft journals, connecting rod bushings, and motor shaft bearings still experience severe rotational loads. To solve this problem without an open oil reservoir, oil-free air compressors utilize permanently sealed, grease-packed precision ball bearings. These bearings are fitted with rubber or metallic shields that encapsulate high-temperature synthetic grease, preventing the lubricant from leaking into the air stream while locking out external ambient dust. Because the grease remains permanently sealed inside the bearing races, the crankcase operates completely dry throughout the life of the machine.
The connecting rod in an oil-free pump is frequently manufactured from lightweight aluminum and often integrates the wrist pin bearing directly into the piston assembly. In many compact designs, the piston head and connecting rod are cast as a single articulated piece, relying on the natural rocking motion of the flexible PTFE cup to accommodate the eccentric motion of the crankshaft. This simplified structural layout dramatically reduces the total number of moving parts inside the crankcase. With fewer joints to lubricate and no oil level sight glasses to monitor, the pump mechanism remains lightweight, compact, and completely immune to oil leaks when tipped over during transport.
The Air Induction and Compression Cycle Explained
The thermodynamic compression cycle inside an oil-free pump operates on a classic two-stroke reciprocating rhythm consisting of an intake stroke and a compression stroke. During the downward intake stroke, the piston descends inside the cylinder bore, creating a partial vacuum in the chamber above the piston crown. This negative pressure causes the flexible intake flapper or reed valve to lift off its precision valve seat, allowing ambient air to rush through the intake filter and fill the expanding cylinder volume. The intake reed valve is typically crafted from thin spring steel or stainless steel, allowing it to open and close hundreds of times per second with minimal mechanical resistance.
Once the piston reaches bottom dead center and reverses direction, the upward compression stroke begins. The rapidly rising air pressure inside the cylinder instantly snaps the intake reed valve shut against its seat, preventing the trapped air from escaping back out through the intake port. As the piston continues its upward travel, the trapped air is compressed into a progressively smaller volume, which causes both its pressure and internal temperature to skyrocket. When the internal cylinder pressure exceeds the pressure inside the discharge tube, the exhaust flapper valve is forced open, channeling the compressed air through a high-pressure discharge line, past a one-way tank check valve, and into the steel storage reservoir.
Thermal Dissipation and Air Cooling Strategies
Because oil serves as a vital heat-transfer fluid in conventional lubricated pumps, oil-free compressors must dissipate intense compression heat entirely through air cooling and conduction. When air is compressed rapidly, the physical laws of thermodynamics dictate that gas temperature rises in direct proportion to the pressure increase. Without an oil bath to carry heat away from the piston crown and cylinder walls, dry pumps rely on deep external cooling fins cast directly into the aluminum cylinder head and pump housing. These thin aluminum fins maximize external surface area, allowing surrounding air to draw heat away from the critical cylinder surfaces.
To accelerate heat rejection, oil-free compressors incorporate high-output radial cooling fans mounted directly onto the motor shaft. These fans pull cool ambient air through dedicated louvered openings in the protective housing and blast it across the finned cylinder heads and discharge tubes. In models like the VEVOR Air Compressor Motor, specialized multi-hole heat sinks and aluminum pump heads work in harmony with cooling fans to prevent heat buildup. Controlling these peak operating temperatures is vital because excessive heat can cause PTFE piston rings to soften or degrade prematurely, leading to lost compression and extended recovery cycles.
High-Speed Universal Motors Versus Low-Noise Dual-Piston Pumps
Oil-free compressors historically earned a reputation for loud, jarring noise levels because early models utilized high-speed universal motors spinning at over 3,000 RPM. Units like the FORNAX pancake compressor operate at 3,550 RPM and reach sound levels around 95 dB(A), which is common for lightweight single-piston designs prioritizing raw portability over acoustic comfort. In these traditional models, the rapid slapping of high-speed reed valves combined with universal motor brush noise creates a harsh acoustic signature that can cause operator fatigue in enclosed garages. However, modern engineering has introduced low-noise dual-piston designs that operate on an entirely different mechanical profile.
Quiet compressors, such as the Stealth 2 Gallon model rated under 60 dB and the BairDplusL 8 Gallon unit rated at 70 dB, use multi-pole induction motors that spin at lower speeds between 1,680 and 3,400 RPM. Instead of forcing a single small piston to cycle furiously, these ultra-quiet pumps utilize two opposing cylinders operating in parallel or alternating stroke patterns. By dividing the workload between dual balanced pistons, the pump achieves rapid air delivery while dramatically lowering vibration and mechanical clatter. Thick sound-dampening intake filter housings, integrated mufflers, and precision counterweights allow these modern oil-free units to operate at sound levels comparable to a normal conversation.
Air Purity and Receiver Tank Condensation Dynamics
One of the most significant operational advantages of an oil-free compressor is the delivery of air that is completely free from oil aerosols. In an oil-lubricated compressor, microscopic droplets of lubricating oil inevitably slip past the piston rings during operation, creating an oil mist that travels down the air hose. While oil mist is harmless for heavy construction framing nailers, it can ruin delicate automotive spray paint jobs, contaminate woodworking finishes, and gum up precision tools. An oil-free pump eliminates oil carryover completely, providing pristine compressed air right out of the factory discharge port.
However, operating an oil-free pump does not eliminate atmospheric moisture from accumulating inside the air receiver. As ambient air is drawn in and compressed, the moisture vapor naturally suspended in the air is squeezed out as liquid water droplets when the hot air cools inside the steel tank. Whether you are using a 6-gallon pancake tank or an 8-gallon wheeled reservoir, water will collect at the lowest point of the vessel. Users must purge this liquid daily through the underside drain valve to prevent internal tank corrosion and keep water droplets from spraying out of pneumatic tools. Proper moisture management also preserves line pressure and prevents premature failure of downstream tool seals.
Cold-Weather Startup Reliability and Electrical Circuit Draw
Starting an air compressor in an unheated garage during sub-freezing winter weather is a common pain point for workshop owners. In an oil-lubricated compressor, conventional ISO 68 or ISO 100 compressor oil thickens significantly as ambient temperatures drop toward freezing. This viscous oil creates tremendous rotational drag on the crankshaft and piston wrist pins, demanding massive startup inrush current that frequently trips standard 15-amp household circuit breakers. If the motor stalls under this initial load, the thermal overload switch can pop, forcing the operator to wait for the motor windings to cool down.
Oil-free compressors completely bypass this cold-weather starting hurdle because dry synthetic PTFE seals and sealed grease bearings maintain consistent friction profiles regardless of ambient temperature. Without thick oil to churn through, electric motors on units like the Metabo HPT pancake compressor and DEWALT trim compressor spin up instantly, even when stored in freezing service trucks. When sizing your electrical supply, reviewing how many watts a portable air compressor uses clarifies why low-draw motors with low starting amps offer superior jobsite versatility. The lack of viscous fluid resistance allows these pumps to achieve full operating RPM within fractions of a second.
Lifespan Expectations, Duty Cycles, and Component Wear
While oil-free air compressors offer exceptional convenience, they are engineered around specific duty cycle limitations and service life expectations that differ from commercial cast-iron units. The primary consumable component in an oil-free pump is the PTFE piston ring. Over hundreds of hours of operation, microscopic layers of the PTFE material slowly transfer onto the cylinder wall, creating a sacrificial self-lubricating boundary layer. Eventually, after 500 to 1,000 or more hours of active runtime depending on motor quality and operating temperature, the ring wears thin enough that air slips past the piston crown, causing tank fill times to lengthen.
To maximize the lifespan of an oil-free pump, operators must respect the manufacturer duty cycle, which is typically around 50 percent for consumer and prosumer models. This means the pump should run for no more than 5 minutes out of every 10-minute period to allow cooling airflow to keep internal cylinder temperatures below critical thresholds. Running an oil-free compressor continuously under heavy demand, such as running a high-demand rotary sander on a small tank, generates extreme heat that accelerates piston ring degradation. Understanding the mechanical relationship between pressure volume and tool draw by understanding air compressor PSI versus CFM ratings helps you avoid overtaxing your pump beyond its engineered capacity.
Essential Maintenance Protocols for Dry Compression Pumps
The phrase oil-free does not mean an air compressor is completely maintenance-free, though daily care requires far less effort than managing an oil-lubricated crankcase. The most critical daily maintenance routine is opening the tank drain valve at the conclusion of every work session. Steel tanks on models like the Goodyear pancake or BairDplusL 8-gallon unit store pressurized air that condenses moisture continuously, and failing to drain this liquid causes internal rust scale that can clog check valves and regulator orifices. Draining the tank with the system depressurized prevents corrosion and ensures the full volume of the vessel remains available for air storage.
Beyond moisture management, operators should regularly inspect the foam or paper intake air filter to prevent airborne dust, sawdust, and drywall powder from being pulled into the cylinder. Because oil-free pumps rely on precise tolerances between the PTFE ring and the polished cylinder sleeve, abrasive dust entering the intake port acts like sandpaper, rapidly scoring the cylinder walls and destroying the compression seal. Operators should also test the ASME safety relief valve periodically by gently pulling the brass ring while the tank is partially pressurized to confirm the spring-loaded plunger moves freely without sticking.
Matching Oil-Free Air Output to Pneumatic Tool Demands
Selecting the right oil-free compressor requires matching the pump delivery rating to the specific air consumption pattern of your pneumatic tools. Air delivery is measured in Standard Cubic Feet per Minute (SCFM) at specific pressure points, usually 90 PSI for fastening and impact tools, and 40 PSI for paint spraying or fluid transfer. Intermittent tools such as brad nailers, finish nailers, and tire inflators require very little continuous air volume, making compact 2 to 6-gallon pancake models delivering 2.6 to 3.0 CFM at 90 PSI exceptionally well-suited for trim carpentry and household repair.
Conversely, continuous-use pneumatic tools like dual-action rotary sanders, air cut-off tools, and HVLP paint sprayers consume continuous volumes between 6 and 12 CFM at 90 PSI. A small oil-free compressor will quickly exhaust its stored air buffer when powering continuous tools, forcing the motor to run non-stop while line pressure plummets below functional working thresholds. For heavier tasks, units equipped with larger 8-gallon tanks and multi-horsepower dual-piston pump heads provide the recovery speed and airflow buffer needed to maintain stable regulated pressure. Evaluating your tool requirements against the certified CFM output and storage volume ensures your dry compressor performs reliably across every project.
Understanding the internal operation of an oil-free compressor clarifies both its distinct engineering strengths and its practical operational boundaries. By replacing oil sumps with self-lubricating PTFE rings, sealed precision bearings, and efficient dual-piston cooling configurations, modern oil-free compressors provide pristine air delivery, dependable sub-freezing starts, and zero lubrication maintenance. Keeping intake air filters clean, respecting duty cycle cooling intervals, and purging tank condensation daily guarantees that your oil-free compressor will deliver dependable pneumatic power for years of workshop and jobsite productivity.
About the author
Glenda Taylor has extensive experience in residential construction, remodeling, home improvement, and tool use. Her practical approach to equipment evaluation focuses on usability, performance, safety, and value—helping DIYers and workshop users make better-informed decisions about compressors and related tools.