
What Kind of Oil to Use in Air Compressor: Essential Pump Lubrication Guide for 2026
Learn what kind of oil to use in air compressor options, viscosity grades, and maintenance practices to protect your pump for October 2026.
 By Glenda Taylor
Updated October 8, 2026

Operating an air compressor pump with depleted or incorrect lubrication creates severe friction that accelerates thermal wear and damages internal mechanical components. Knowing what kind of oil to use in air compressor pumps is vital for maintaining proper crankcase protection across various garage and jobsite settings. Standard automotive motor oils contain chemical detergents that can scour compressor cylinder walls and foul sensitive valve plates. Choosing a dedicated non-detergent petroleum formulation or an industrial-grade full synthetic lubricant ensures your pump maintains a resilient hydrodynamic film under demanding compression cycles.
Many equipment owners mistakenly assume that any workshop fluid can lubricate a reciprocating air pump. However, frequent questions arise regarding using air tool oil in an air compressor pump, which actually lacks the thermal viscosity and film strength required inside high-temperature compression chambers. Lubricating an oil-bath compressor correctly prevents crankcase sludge accumulation, limits oil carryover into downstream pneumatic hoses, and protects internal wrist pins from catastrophic failure. Reviewing viscosity grades, base stock compositions, and equipment specifications will help keep your pneumatic machinery running smoothly during demanding projects.
| Award | Product | ACR Score About ACR ScoreThe ACR Score is our own rating from 0 to 10, based on performance, design and build, ease of use, and value. It reflects independent research and is never influenced by manufacturers, retailers, or affiliate commissions. Learn more › | |
|---|---|---|---|
| Best Overall |
Mag 1 1-Gallon Air Compressor Oil
|
9.2/10 | Buy |
| Best Budget |
 Triax Kompressor ISO 46 SAE 20 Full Synthetic Air |
9.1/10 | Buy |
| Best Premium |
 Triax Kompressor ISO 100 SAE 30 Oil (5 Gal) |
9.1/10 | Buy |
| Best Value |
 Milton 1002 SAE 30W Compressor Oil, 1 Gallon |
8.8/10 | Buy |
 TRIAX Kompressor ISO 46 SAE 20 Full Synthetic Air |
8.8/10 | Buy | |
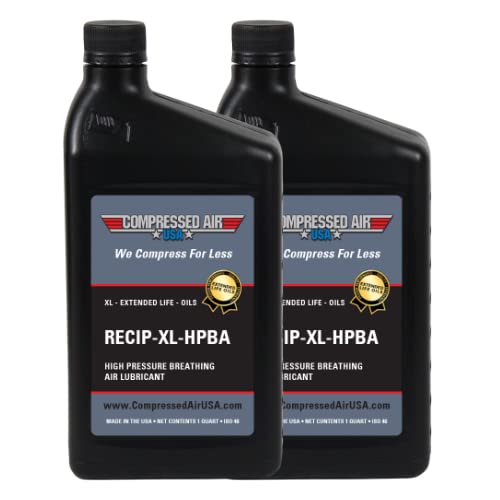 Compressed Air USA Breathing Safe Oil, 2 Quart |
8.8/10 | Buy | |
 Campbell Hausfeld ST1253 Compressor Oil (16 oz) |
8.6/10 | Buy | |
 TRIAX Kompressor ISO 68 Full Synthetic Air |
8.6/10 | Buy | |
 Milton 1002-32 ISO-100 Compressor Oil, 32 oz |
8.4/10 | Buy | |
 MAG 1 Air Compressor Oil 16 oz |
7.8/10 | Buy |
Mag 1 1-Gallon Air Compressor Oil
Formulated for reliable workshop maintenance, Mag 1 Air Compressor Oil uses refined petroleum base stocks paired with anti-foam additives to maintain stable lubrication. The generous one-gallon volume makes it a practical choice for keeping reciprocating or stationary compressors running smoothly over time.
Pros
- Anti-foam additives maintain steady lubrication
- Refined petroleum stocks promote smooth operation
- Formula helps extend compressor service life
- Generous 1-gallon volume handles multiple refills
Cons
- Jug weighs 7.25 pounds and can be heavy to pour
- One-gallon size may exceed small top-off needs
Triax Kompressor ISO 46 SAE 20 Full Synthetic Air
Triax Kompressor ISO 46 SAE 20 is a commercial-grade, full synthetic non-detergent compressor oil engineered for oil-lubricated reciprocating, rotary screw, and vane pumps operating in temperatures from -49°F to over 140°F. It provides exceptional thermal protection and extended component life for garage mechanics and shop owners maintaining heavy-duty pneumatic systems.
Pros
- Extreme all-weather operating range from -49°F to 140°F+ prevents cold-start motor stalling and high-heat viscosity breakdown
- Non-detergent full synthetic formula protects internal bearings and provides up to 20,000 hours of service longevity
- Lowers operating pump temperatures by 30% and actively sheds condensation to prevent internal crankcase rust
- Compatible with oil-lubricated reciprocating, rotary screw, and rotary vane compressor pumps from major manufacturers
Cons
- Not suitable for oil-free or maintenance-free dual-piston compressor designs that do not use crankcase oil
- Explicitly prohibited for use in breathing air systems, oxygen compressors, or liquid natural gas (LNG) units
- Single-quart volume may require purchasing multiple bottles for larger stationary 60-gallon or 80-gallon shop pump crankcases
Triax Kompressor ISO 100 SAE 30 Oil (5 Gal)
Engineered for rotary, vane, screw, and reciprocating systems, this industrial-grade synthetic fluid provides up to 20,000 hours of continuous service across extreme temperatures. Its non-detergent formula lowers operating heat by 30 percent while guarding vital bearings against friction and moisture.
Pros
- Extended 20,000-hour life span minimizes maintenance cycles
- Reliable all-season operation across wide temperature swings
- Substantially reduces operating temperatures and oil burnoff
- Non-detergent blend prevents bearing wear and vibration
Cons
- Not compatible with oxygen air or LNG compressors
- Large 5-gallon volume exceeds small workshop requirements
Milton 1002 SAE 30W Compressor Oil, 1 Gallon
Milton 1002 is a non-detergent ISO-100 SAE 30W conventional lubricant engineered specifically for reciprocating air compressors. The one-gallon capacity makes it a sensible option for regular workshop equipment upkeep.
Pros
- Non-detergent formula tailored for reciprocating compressors
- Standard ISO-100 SAE 30W viscosity rating
- Generous one-gallon volume covers multiple refills
Cons
- Conventional mineral formula instead of synthetic blend
- Heavy container can be awkward to pour directly
TRIAX Kompressor ISO 46 SAE 20 Full Synthetic Air
TRIAX Kompressor ISO 46 SAE 20 is a commercial-grade, full-synthetic non-detergent lubricant engineered for oil-lubricated reciprocating, rotary screw, and vane air compressors. It provides reliable extreme-temperature wear protection and multi-viscosity all-season performance, making it an excellent maintenance choice for auto shops, contractors, and home garage workshops.
Pros
- Full synthetic non-detergent formulation extends pump life across severe operating conditions
- True all-season multi-viscosity rating maintains fluid flow from -49 deg F up to 140 deg F+
- Formulated to lower operating temperatures by up to 30% and eliminate oil vapor odor
- Compatible with a wide array of compressor pumps including reciprocating and rotary screw designs
Cons
- Not formulated for oil-free air compressors, breathing air systems, oxygen setups, or LPG gas pipelines
- Users must verify whether their pump manufacturer specifically calls for ISO 46 (SAE 20) rather than heavier ISO 68 or ISO 100 weights
- Requires careful manual crankcase draining and filling without an included pour spout
Compressed Air USA Breathing Safe Oil, 2 Quart
Formulated for critical breathing air applications like SCUBA, firefighting, and medical systems, this ISO 100 oil delivers robust wear protection under extreme temperatures and pressures. Its non-toxic composition and high flash point ensure dependable safety for specialized reciprocating compressors.
Pros
- Safe formulation suitable for SCUBA and medical air systems
- High flash and auto-ignition points enhance operational safety
- Resists carbon and varnish buildup under extreme temperatures
- Non-toxic formula provides strong wear and rust protection
Cons
- Restricted to reciprocating units rather than rotary screw systems
- ISO 100 rating unsuitable for low-viscosity compressor setups
Campbell Hausfeld ST1253 Compressor Oil (16 oz)
Formulated for workshop and industrial setups, this 30-weight lubricant protects compressor pumps against rust, sludge, and component wear. The compact 16-ounce bottle makes routine top-offs and crankcase servicing straightforward.
Pros
- Formulated specifically for compressor pumps and motors
- 30-weight viscosity helps minimize component wear
- Inhibits rust, sludge, and internal corrosion
- Compact bottle enables controlled, mess-free pouring
Cons
- 16-ounce volume may require multiple bottles for large units
- Single 30-weight viscosity is not suitable for all models
TRIAX Kompressor ISO 68 Full Synthetic Air
TRIAX Kompressor ISO 68 is a commercial-grade, full synthetic compressor lubricant engineered for oil-lubricated reciprocating, rotary screw, and vane pumps operating between -49°F and 140°F+. It is an excellent maintenance solution for auto mechanics, shop owners, and contractors seeking lower pump operating temperatures and up to 20,000 hours of service life.
Pros
- Extended 20,000-hour service life minimizes routine maintenance intervals on high-demand shop compressors
- All-season stability from -49°F to 140°F+ prevents cold-morning motor drag and high-heat viscosity breakdown
- Non-detergent formulation separates condensation cleanly to safeguard internal crankcase bearings
- Broad compatibility across major reciprocating, rotary screw, and rotary vane compressor manufacturers
Cons
- Not suitable for maintenance-free oil-free compressor designs or oxygen and Liquid Natural Gas (LNG) systems
- One-gallon container size exceeds the immediate refill capacity of small single-stage DIY splash-lube pumps
Milton 1002-32 ISO-100 Compressor Oil, 32 oz
Formulated specifically for oil-lubricated reciprocating compressors, this ISO-100 non-detergent lubricant shields pumps against wear and deposit buildup. It separates easily from moisture and remains fluid down to -15°F for dependable cold-weather starts.
Pros
- Protects internal components against wear and corrosion
- Non-detergent formula resists foaming and separates water
- Inhibits sludge and carbon deposit formation
- Maintains fluidity in temperatures down to -15°F
Cons
- Designed strictly for reciprocating pump mechanisms
- Conventional oil base rather than full synthetic
MAG 1 Air Compressor Oil 16 oz
MAG 1 Air Compressor Oil is a specialized 16-ounce petroleum lubricant formulated with anti-foam agents and rust inhibitors to protect oil-lubricated compressor pumps under heavy operating conditions. It offers essential wear protection and thermal stability for home garage hobbyists, auto mechanics, and shop owners maintaining oil-lubricated pneumatic equipment.
Pros
- Formulated specifically for compressor pump crankcases rather than generic detergent automotive motor oils
- Anti-foam chemistry helps prevent oil foaming and maintains steady lubrication under rapid piston strokes
- Helps protect internal metal components against rust and oxidation caused by ambient moisture buildup
- Convenient 16-ounce bottle size fits easily into garage maintenance cabinets and tool chests
Cons
- Not suitable for maintenance-free oil-free air compressors
- A 16-ounce volume may require multiple bottles for larger stationary multi-stage shop compressors with high crankcase capacities
Essential Guidelines on Compressor Lubrication and Pump Oil Selection
Selecting the correct lubricant for an air compressor crankcase requires balancing mechanical design, ambient operating temperatures, and chemical additive packages. Using an incompatible fluid can quickly ruin cast-iron cylinder walls, destroy compression rings, and cause reed valves to stick with gummy carbon residue. Dedicated air compressor oils provide high thermal stability and foam resistance without relying on harsh automotive additives. Understanding the precise lubrication requirements of your pump will protect your equipment investment and maintain reliable air delivery.
The Critical Difference Between Detergent and Non-Detergent Oils
Automotive engine oils are blended with heavy detergent additives, primarily calcium and magnesium sulfonates, designed to clean combustion byproducts. In a car engine, these detergents hold soot, metallic particles, and carbon deposits in liquid suspension so that an oil filter can trap them. Because typical reciprocating air compressor pumps lack oil filters and pressurized circulating pumps, suspended particulates continuously circulate through the crankcase. This abrasive slurry scours cylinder bores, connecting rod journals, and wrist pins, causing premature mechanical failure.
Non-detergent compressor oils function differently by allowing metallic wear particles and heavy contaminants to settle harmlessly at the bottom of the oil sump. As the splash dipper spins through the oil bath, it picks up clean fluid from the upper layer while leaving heavy debris undisturbed below. Formulations like Milton conventional compressor oil and Campbell Hausfeld pump oil specifically utilize non-detergent chemistry to prevent internal scoring. Using a non-detergent lubricant ensures that dirt stays out of critical friction zones throughout the service life of the pump.
Thermal breakdown presents another major reason to avoid automotive motor oils in pneumatic equipment. Compressor discharge temperatures at the cylinder head frequently reach high levels during extended recovery cycles. Detergent additives tend to carbonize quickly when exposed to these hot valve plates, forming crusty black deposits on intake and exhaust reed valves. Once reed valves become fouled with carbon buildup, they fail to seat properly, resulting in severe compression loss, continuous pump cycling, and motor overheating.
Understanding ISO Viscosity Grades and Equivalent SAE Ratings
Compressor lubricants are graded primarily using the International Organization for Standardization (ISO) viscosity scale, which correlates directly with common Society of Automotive Engineers (SAE) weight ratings. An ISO 100 compressor oil corresponds closely to an SAE 30-weight oil, which serves as the standard factory recommendation for most single-stage and two-stage piston compressors. Lubricants such as Milton 1002 and Mag 1 provide the heavy film strength needed to protect cast-iron cylinders operating in ambient workshop temperatures between 40 degrees Fahrenheit and 100 degrees Fahrenheit.
Lighter viscosity grades become necessary when operating pneumatic equipment in unheated garages, mobile service trailers, or outdoor winter environments. An ISO 68 lubricant corresponds to an intermediate 20-weight to 30-weight range, while an ISO 46 oil corresponds to a light SAE 20-weight fluid. Products like TRIAX Kompressor ISO 46 flow smoothly in freezing environments down to sub-zero conditions, preventing heavy viscous drag on the pump crankshaft during cold startups. Using oil that is too thick in cold weather can cause the electric motor to hum, overload the start capacitor, and trip standard household circuit breakers.
Choosing the correct viscosity rating also depends on continuous operating loads and duty cycle demands. Single-stage compressors generating up to 135 PSI produce less internal compression heat than industrial two-stage units generating 175 PSI. Two-stage cast-iron pumps typically require an ISO 100 fluid to maintain an adequate hydrodynamic wedge between the piston rings and cylinder walls under high pressure. Matching the ISO viscosity to both your local ambient climate and pump staging specifications guarantees reliable starting and sustained mechanical protection.
Synthetic Formulations Versus Conventional Petroleum Base Stocks
Conventional petroleum compressor oils, such as Mag 1 Air Compressor Oil, are refined from premium mineral base stocks and fortified with anti-foam and rust-inhibiting chemical packages. These conventional lubricants provide dependable lubrication for DIY home mechanics, intermittent workshop chores, and light-duty pneumatic nailing tasks. Mineral-based oils are economical and perform reliably as long as operating temperatures remain moderate and oil change intervals are strictly observed. However, conventional mineral stocks break down more rapidly when subjected to continuous industrial duty cycles.
Full synthetic compressor oils utilize synthesized hydrocarbon molecules or ester bases that deliver exceptional thermal and oxidative resistance. Advanced products like TRIAX Kompressor multi-viscosity synthetic oils maintain high shear stability and provide multi-viscosity performance across extreme temperature spreads. Synthetic fluids resist thermal cracking, prevent lacquer and varnish formation on internal bearings, and significantly reduce operational pump temperatures. Commercial shops and auto restoration bays running continuous tools like dual-action sanders or paint sprayers benefit greatly from the thermal stability of synthetic fluids.
Extended drain intervals represent another meaningful distinction between synthetic and mineral base stocks. Conventional petroleum oils generally require replacement every 200 to 500 operating hours to prevent viscosity breakdown and sludge formation. High-performance synthetic lubricants can safely operate for thousands of continuous service hours under clean operating conditions. While synthetic formulations require a greater initial investment, their ability to reduce friction, lower running temperatures, and minimize mechanical wear makes them advantageous for heavy-use environments.
Lubrication Demands Across Different Pump Architectures
Reciprocating piston compressors typically utilize a splash-lubrication mechanism powered by a mechanical dipper attached to the bottom of the connecting rod cap. As the crankshaft rotates, this dipper plunges into the oil reservoir and throws an oil mist across the crankcase cavity. Understanding how reciprocating air compressors operate helps clarify why splash dippers require an exact oil level to coat the wrist pins and cylinder skirts without flooding the combustion chamber. Splash-lubricated pumps demand non-foaming fluids to ensure that splashing creates an oil mist rather than aerated froth.
Rotary screw and rotary vane compressors operate under entirely different mechanical principles that require specialized fluid performance. In a rotary screw pump, fluid is injected directly into the compression chamber to seal the small clearances between helical rotors, absorb the heat of compression, and lubricate the roller bearings. Examining the mechanical differences between reciprocating and rotary compressors reveals why rotary units demand oils with superior demulsibility and rapid air release. Multi-viscosity synthetics formulated for both reciprocating and rotary screw units, like the TRIAX Kompressor series, provide the thermal stability necessary for continuous rotor contact.
Oil-free compressors, such as compact pancake models and quiet dual-piston units, do not utilize liquid crankcase oil of any kind. These machines rely on self-lubricating polytetrafluoroethylene (PTFE) piston ring sleeves and permanently sealed, grease-packed bearings to manage friction. Introducing liquid lubricant into an oil-free compressor will instantly destroy the dry PTFE seals, attract abrasive dust, and foul the cylinder sleeves. Equipment owners must always confirm whether their air compressor features an oil-lubricated cast-iron pump before attempting to add fluid to the machine.
Specialized Applications: High-Pressure Breathing Air Systems
Standard industrial compressor lubricants must never be used in compressors designated for human respiration, such as SCUBA diving, firefighting SCBA tanks, or medical air systems. Conventional petroleum oils break down at high compression pressures and release dangerous volatile organic compounds, hydrocarbon mists, and toxic carbon monoxide into the breathing air stream. Breathing air compressors operate at extreme pressures, often between 3,000 PSI and 5,000 PSI, requiring specialized non-toxic synthetic lubricants designed specifically for life-support pneumatic hardware.
Products like Compressed Air USA Breathing Safe Lubricating Oil are engineered specifically for high-pressure reciprocating breathing air units. These specialized ISO 100 lubricants feature exceptionally high flash points and auto-ignition thresholds to prevent dangerous crankcase vapor ignition under severe compression heat. They are formulated to be non-toxic and non-hazardous, producing minimal carbon residue across multi-stage valve assemblies. Utilizing dedicated breathing air lubricants ensures that downstream air purification filters do not become prematurely fouled with hazardous volatile hydrocarbons.
Operating a breathing air compressor also requires adhering to strict purity standards and certified filtration routines alongside specialized oil use. Even when running non-toxic synthetic oils, condensation separators and molecular sieve filter cartridges must be maintained according to strict schedules. Verifying that your high-pressure pump utilizes an approved breathing air fluid protects internal mechanical components while safeguarding human life during emergency, diving, and medical operations.
Managing Foaming, Moisture Condensation, and Emulsification
Air compressors draw in ambient atmospheric air, which naturally contains moisture in the form of relative humidity. As the pump compresses air, internal temperatures rise dramatically, vaporizing incoming moisture before it passes into the storage tank. However, when the compressor shuts down and cools, moisture vapor condenses on the cold internal walls of the crankcase and trickles into the oil reservoir. Quality compressor oils feature advanced demulsifying additives that actively separate water from the oil base rather than allowing it to form a creamy, emulsified sludge.
If a low-grade lubricant emulsifies with condensed moisture, the resulting mixture loses its ability to lubricate critical bearing journals. Water trapped within emulsified oil causes rapid internal corrosion, rust pitting on polished crankshaft surfaces, and premature bearing seizure. Formulations like Milton 1002 and TRIAX Kompressor are engineered to repel water, allowing free moisture to settle at the very bottom of the crankcase drain port. Periodically loosening the crankcase drain plug allows accumulated condensation to escape before it compromises pump lubrication.
Anti-foaming additives provide another critical layer of mechanical defense inside splash-lubricated crankcases. When a connecting rod dipper strikes the oil reservoir thousands of times per minute, untreated oil can whip into a thick, frothy foam. Air bubbles trapped in oil cannot support heavy mechanical loads, which leads to direct metal-to-metal contact on connecting rod bearings. Petroleum formulas like Mag 1 Air Compressor Oil incorporate specialized anti-foam agents that collapse surface bubbles immediately, ensuring a continuous film of pure liquid lubricant across every moving part.
Step-by-Step Compressor Oil Maintenance and Draining Procedures
Establishing a consistent oil inspection and maintenance routine is the most reliable way to prevent expensive pump failures. Before starting any work session, inspect the oil level through the transparent crankcase sight glass or by removing the dipstick. On a circular sight glass, the oil meniscus should rest precisely in the center of the red alignment dot when the compressor sits on a level surface. Operating a pump with an oil level below the sight glass dot risks severe oil starvation, while filling above the dot causes high crankcase pressure.
Newly purchased oil-lubricated compressors require an initial break-in fluid change to flush out microscopic machining debris. As new piston rings seat against cast-iron cylinder walls during the first 20 to 50 hours of operation, small metallic particles wear away and accumulate in the crankcase. Draining the initial factory oil after this initial break-in period removes abrasive break-in debris before it can damage crankshaft journals. After the initial break-in service, standard petroleum lubricants should normally be changed every 250 operating hours or at least once every calendar year.
To perform an oil change safely, run the compressor for five minutes to warm the lubricant slightly, which helps suspended particles drain freely. Disconnect the electrical power cord or lock out the breaker, and depressurize the air tank completely by pulling the ring on the ASME safety relief valve. Position a suitable catch container beneath the crankcase drain plug, remove the plug along with the upper oil fill breather cap, and let the old fluid drain out completely. Reinstall the drain plug securely, apply fresh Teflon pipe sealant if required, and refill the crankcase slowly with clean non-detergent or synthetic compressor oil until the fluid reaches the center of the sight glass.
Operational Risks of Underfilling and Overfilling the Crankcase
Underfilling a compressor crankcase quickly leads to catastrophic mechanical failure due to localized oil starvation. When the fluid level drops below the reach of the connecting rod dipper, the pump mechanism loses its ability to splash oil onto the upper cylinder walls and wrist pins. Dry piston rings rubbing against unlubricated cast-iron cylinders generate extreme frictional heat, causing the rings to score the cylinder walls or seize entirely. Once a connecting rod seizes on the crankshaft journal from lack of lubrication, it frequently snaps, punching a hole directly through the aluminum crankcase housing.
Overfilling the crankcase introduces an entirely different set of operational problems that can degrade performance and foul pneumatic tools. When the oil level is too high, the rotating crankshaft counterweights slam continuously into the oil pool, creating severe hydraulic resistance and violent fluid churning. This churning generates extreme crankcase pressures that can rupture crankshaft oil seals and force liquid oil past the piston compression rings. Excessive oil carryover then migrates through the discharge line into the air tank, contaminating air lines, ruining automotive paint finishes, and gumming up pneumatic nailers.
Seasonal Selection Strategy and Final Practical Takeaways
Selecting the ideal oil for your air compressor ultimately comes down to understanding your operating environment, equipment design, and usage frequency. For heated garages, indoor workshops, and warm summer weather, a conventional or synthetic ISO 100 SAE 30-weight non-detergent oil remains the dependable standard. For cold-weather jobsite applications where sub-freezing morning starts are common, switching to an ISO 46 or ISO 68 multi-viscosity synthetic fluid prevents hard starting and protects electric motors from pulling excessive inrush current on standard 15-amp household circuits.
Always inspect your compressor oil sight glass regularly, drain tank moisture daily through the bottom drain valve, and avoid automotive detergent oils entirely. Investing in high-performance non-detergent mineral oil or full synthetic multi-viscosity fluid preserves compression efficiency and prevents valve carbonization. By matching the correct lubricant viscosity and base stock to your specific pneumatic pump, your air compressor will continue to provide smooth, dependable power across years of heavy workshop service.
About the author
Glenda Taylor has extensive experience in residential construction, remodeling, home improvement, and tool use. Her practical approach to equipment evaluation focuses on usability, performance, safety, and value—helping DIYers and workshop users make better-informed decisions about compressors and related tools.