
What Kind of Oil Does an Air Compressor Take: Practical Workshop Guide for 2026
Review %what kind of oil does an air compressor take% for reliable pump protection in October 2026, covering ISO viscosities and non-detergent formulas.
 By Tony Carrick
Updated October 8, 2026

Operating a cast-iron or aluminum air compressor pump under heavy workshop duty cycles generates substantial friction and intense thermal stress along the cylinder walls. Pouring an unapproved fluid into the crankcase risks rapid valve carbonization, seal deterioration, and premature piston seizure before a project reaches completion. Determining %what kind of oil does an air compressor take% requires looking beyond automotive shelf stock to identify lubricants engineered specifically for pneumatic compression dynamics. Reviewing manufacturer recommendations and acceptable compressor crankcase lubricants ensures your pump maintains compression efficiency without burning fluid or creating hazardous vapor deposits.
Air compressor crankcases operate under entirely different mechanical principles than internal combustion engines, lacking pressurized oil filters while constantly confronting ambient moisture condensation. Dedicated compressor formulations utilize non-detergent base stocks and specialized anti-foam agents that allow water to separate cleanly rather than emulsifying into corrosive sludge. Selecting the right viscosity, whether a conventional 30-weight mineral oil or an all-season synthetic, keeps internal reed valves clean and preserves bearing tolerances across extended runtimes. Understanding these fundamental fluid distinctions protects both your pneumatic tools downstream and your initial equipment investment.
| Award | Product | ACR Score About ACR ScoreThe ACR Score is our own rating from 0 to 10, based on performance, design and build, ease of use, and value. It reflects independent research and is never influenced by manufacturers, retailers, or affiliate commissions. Learn more › | |
|---|---|---|---|
| Best Overall |
Mag 1 1-Gallon Air Compressor Oil
|
9.2/10 | Buy |
| Best Budget |
 Triax Kompressor ISO 46 SAE 20 Full Synthetic Air |
9.1/10 | Buy |
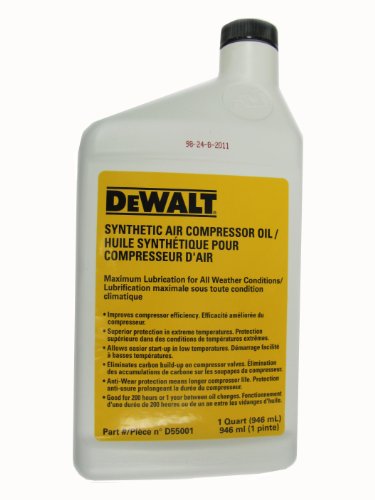 DeWalt D55001 1-Quart Compressor Oil |
9.1/10 | Buy | |
| Best Premium |
 Triax Kompressor ISO 100 SAE 30 Oil (5 Gal) |
9.1/10 | Buy |
 Milton 1002 SAE 30W Compressor Oil, 1 Gallon |
8.8/10 | Buy | |
 TRIAX Kompressor ISO 46 SAE 20 Full Synthetic Air |
8.8/10 | Buy | |
 Campbell Hausfeld ST1253 Compressor Oil (16 oz) |
8.6/10 | Buy | |
| Best Value |
 TRIAX Kompressor ISO 68 Full Synthetic Air |
8.6/10 | Buy |
 Ingersoll Rand All Season Select Lubricant, 1L |
8.6/10 | Buy | |
 Milton 1002-32 ISO-100 Compressor Oil, 32 oz |
8.4/10 | Buy |
Mag 1 1-Gallon Air Compressor Oil
Formulated for reliable workshop maintenance, Mag 1 Air Compressor Oil uses refined petroleum base stocks paired with anti-foam additives to maintain stable lubrication. The generous one-gallon volume makes it a practical choice for keeping reciprocating or stationary compressors running smoothly over time.
Pros
- Anti-foam additives maintain steady lubrication
- Refined petroleum stocks promote smooth operation
- Formula helps extend compressor service life
- Generous 1-gallon volume handles multiple refills
Cons
- Jug weighs 7.25 pounds and can be heavy to pour
- One-gallon size may exceed small top-off needs
Triax Kompressor ISO 46 SAE 20 Full Synthetic Air
Triax Kompressor ISO 46 SAE 20 is a commercial-grade, full synthetic non-detergent compressor oil engineered for oil-lubricated reciprocating, rotary screw, and vane pumps operating in temperatures from -49°F to over 140°F. It provides exceptional thermal protection and extended component life for garage mechanics and shop owners maintaining heavy-duty pneumatic systems.
Pros
- Extreme all-weather operating range from -49°F to 140°F+ prevents cold-start motor stalling and high-heat viscosity breakdown
- Non-detergent full synthetic formula protects internal bearings and provides up to 20,000 hours of service longevity
- Lowers operating pump temperatures by 30% and actively sheds condensation to prevent internal crankcase rust
- Compatible with oil-lubricated reciprocating, rotary screw, and rotary vane compressor pumps from major manufacturers
Cons
- Not suitable for oil-free or maintenance-free dual-piston compressor designs that do not use crankcase oil
- Explicitly prohibited for use in breathing air systems, oxygen compressors, or liquid natural gas (LNG) units
- Single-quart volume may require purchasing multiple bottles for larger stationary 60-gallon or 80-gallon shop pump crankcases
DeWalt D55001 1-Quart Compressor Oil
Formulated for regular air compressor maintenance, the DeWalt D55001 comes in a handy one-quart bottle to keep pump components operating smoothly. It is a solid choice for workshops and job sites running oil-lubricated compressors that require dedicated manufacturer-grade fluid.
Pros
- Convenient 1-quart size for routine maintenance
- OEM formulation from an established tool brand
- Compact bottle design stores easily
Cons
- Not applicable for oil-free compressor models
- May require multiple bottles for high-capacity industrial tanks
Triax Kompressor ISO 100 SAE 30 Oil (5 Gal)
Engineered for rotary, vane, screw, and reciprocating systems, this industrial-grade synthetic fluid provides up to 20,000 hours of continuous service across extreme temperatures. Its non-detergent formula lowers operating heat by 30 percent while guarding vital bearings against friction and moisture.
Pros
- Extended 20,000-hour life span minimizes maintenance cycles
- Reliable all-season operation across wide temperature swings
- Substantially reduces operating temperatures and oil burnoff
- Non-detergent blend prevents bearing wear and vibration
Cons
- Not compatible with oxygen air or LNG compressors
- Large 5-gallon volume exceeds small workshop requirements
Milton 1002 SAE 30W Compressor Oil, 1 Gallon
Milton 1002 is a non-detergent ISO-100 SAE 30W conventional lubricant engineered specifically for reciprocating air compressors. The one-gallon capacity makes it a sensible option for regular workshop equipment upkeep.
Pros
- Non-detergent formula tailored for reciprocating compressors
- Standard ISO-100 SAE 30W viscosity rating
- Generous one-gallon volume covers multiple refills
Cons
- Conventional mineral formula instead of synthetic blend
- Heavy container can be awkward to pour directly
TRIAX Kompressor ISO 46 SAE 20 Full Synthetic Air
TRIAX Kompressor ISO 46 SAE 20 is a commercial-grade, full-synthetic non-detergent lubricant engineered for oil-lubricated reciprocating, rotary screw, and vane air compressors. It provides reliable extreme-temperature wear protection and multi-viscosity all-season performance, making it an excellent maintenance choice for auto shops, contractors, and home garage workshops.
Pros
- Full synthetic non-detergent formulation extends pump life across severe operating conditions
- True all-season multi-viscosity rating maintains fluid flow from -49 deg F up to 140 deg F+
- Formulated to lower operating temperatures by up to 30% and eliminate oil vapor odor
- Compatible with a wide array of compressor pumps including reciprocating and rotary screw designs
Cons
- Not formulated for oil-free air compressors, breathing air systems, oxygen setups, or LPG gas pipelines
- Users must verify whether their pump manufacturer specifically calls for ISO 46 (SAE 20) rather than heavier ISO 68 or ISO 100 weights
- Requires careful manual crankcase draining and filling without an included pour spout
Campbell Hausfeld ST1253 Compressor Oil (16 oz)
Formulated for workshop and industrial setups, this 30-weight lubricant protects compressor pumps against rust, sludge, and component wear. The compact 16-ounce bottle makes routine top-offs and crankcase servicing straightforward.
Pros
- Formulated specifically for compressor pumps and motors
- 30-weight viscosity helps minimize component wear
- Inhibits rust, sludge, and internal corrosion
- Compact bottle enables controlled, mess-free pouring
Cons
- 16-ounce volume may require multiple bottles for large units
- Single 30-weight viscosity is not suitable for all models
TRIAX Kompressor ISO 68 Full Synthetic Air
TRIAX Kompressor ISO 68 is a commercial-grade, full synthetic compressor lubricant engineered for oil-lubricated reciprocating, rotary screw, and vane pumps operating between -49°F and 140°F+. It is an excellent maintenance solution for auto mechanics, shop owners, and contractors seeking lower pump operating temperatures and up to 20,000 hours of service life.
Pros
- Extended 20,000-hour service life minimizes routine maintenance intervals on high-demand shop compressors
- All-season stability from -49°F to 140°F+ prevents cold-morning motor drag and high-heat viscosity breakdown
- Non-detergent formulation separates condensation cleanly to safeguard internal crankcase bearings
- Broad compatibility across major reciprocating, rotary screw, and rotary vane compressor manufacturers
Cons
- Not suitable for maintenance-free oil-free compressor designs or oxygen and Liquid Natural Gas (LNG) systems
- One-gallon container size exceeds the immediate refill capacity of small single-stage DIY splash-lube pumps
Ingersoll Rand All Season Select Lubricant, 1L
Engineered as an all-weather OEM fluid, this synthetic lubricant protects reciprocating compressors during continuous duty while resisting carbon buildup on critical valves. It is a solid pick for equipment owners who want fewer oil changes and reliable year-round operation.
Pros
- Maintains stable viscosity in hot and cold seasons
- Lasts four times longer than petroleum oil
- Keeps valves and rings free of carbon deposits
- Protects bearings under continuous duty cycles
Cons
- Formulated specifically for reciprocating compressor systems
- One-liter bottle requires buying multiples for large pumps
Milton 1002-32 ISO-100 Compressor Oil, 32 oz
Formulated specifically for oil-lubricated reciprocating compressors, this ISO-100 non-detergent lubricant shields pumps against wear and deposit buildup. It separates easily from moisture and remains fluid down to -15°F for dependable cold-weather starts.
Pros
- Protects internal components against wear and corrosion
- Non-detergent formula resists foaming and separates water
- Inhibits sludge and carbon deposit formation
- Maintains fluidity in temperatures down to -15°F
Cons
- Designed strictly for reciprocating pump mechanisms
- Conventional oil base rather than full synthetic
Technical Criteria for Selecting Air Compressor Pump Lubricants
Selecting the correct lubricant requires evaluating mechanical pump architecture, ambient shop temperatures, and the chemical composition of modern machine oils. Because pneumatic equipment generates high localized heat without the fuel dilution seen in engines, the oil must resist oxidation and thermal breakdown under continuous mechanical pressure. Matching your specific compressor design to an approved viscosity grade keeps moving components operating smoothly while preventing expensive head rebuilds. The following sections analyze fluid specifications, operational tradeoffs, and servicing protocols to keep your shop compressor performing reliably.
Standard Requirements for Reciprocating and Rotary Compressor Pumps
Most reciprocating air compressors require a specialized, non-detergent machine oil typically rated at ISO 100 or SAE 30 weight. These fluids lack the aggressive detergent additive packages found in automotive motor oils, which are intended to keep combustion soot suspended in a pressurized circulation loop. Dedicated mineral options like Mag 1 Air Compressor Oil and Milton 1002 High Performance Conventional Air provide the straightforward lubrication required by single-stage and two-stage cast iron pumps. Rotary screw and severe-duty commercial units frequently specify specialized synthetic blends with distinct viscosity curves tailored for continuous circulation.
Understanding why conventional automotive engine oil fails in air compressor crankcases prevents expensive shop repairs down the road. Standard passenger car motor oils contain detergent compounds designed to hold carbon particles in suspension until the fluid passes through an automotive oil filter. Air compressor pumps lack pressurized oil filters, meaning suspended contaminants circulate continuously across wrist pins, connecting rods, and splash dippers. If you are curious about running motor oil like 15W-40 in a compressor, recognizing this fundamental filtration difference illustrates why automotive blends accelerate mechanical wear in splash-lubricated pumps.
Thermal breakdown at the valve plate represents another severe limitation when using automotive lubricants in a pneumatic system. Compression chambers generate intense localized heat during the final stage of piston travel, often exceeding temperatures found in standard automotive oil pans. Detergents and viscosity index improvers contained in regular motor oils bake onto reed valves and discharge ports, forming hardened carbon crusts. This carbon buildup prevents the valves from seating flat against the valve plate, leading to lost air delivery, continuous pump cycling, and severe thermal overheating.
The Critical Function of Non-Detergent Base Stocks and Demulsibility
Splash-lubricated compressor pumps rely on mechanical agitation to disperse lubricant across internal bearings and cylinder walls. As the connecting rod swings through the lower crankcase, a machined dipper splashes oil upward into the cylinder bore and wrist pin bushings. Non-detergent formulas ensure this vigorous splashing action does not create micro-foaming within the crankcase reservoir. Anti-foam additives present in products like Mag 1 maintain a solid liquid film between moving metal components, preventing friction spikes and localized galling under heavy load.
Demulsibility is the chemical property that allows an oil to separate cleanly from water, and it represents a mandatory requirement in pneumatic systems. Every cubic foot of ambient air ingested by the pump contains moisture vapor that condenses into liquid water inside the cooler crankcase during routine operation. Detergent oils hold this moisture in suspension, transforming the lubricant into a milky, acidic emulsion that strips away corrosion protection. Non-detergent compressor oils allow condensed water to drop straight to the bottom of the sump, where it remains separated from circulating friction surfaces.
Regular moisture draining from the pump crankcase complements the daily condensation purging required for air storage tanks. When water drops out of suspension in a non-detergent reservoir, operators can inspect the sight glass to identify separation layers during routine inspections. If excessive water pools at the bottom of the crankcase, it can be drained through the oil drain plug before restarting the machine. Neglecting this separation leads to internal rust formation along cast iron cylinder walls, damaged wrist pins, and premature bearing destruction.
Viscosity Ratings and Temperature Matching: ISO 100, ISO 68, and ISO 46
Industrial compressor lubricants utilize the International Organization for Standardization (ISO) viscosity grading system rather than standard automotive multi-grade numbers. ISO 100 corresponds roughly to a single-grade SAE 30 weight oil, serving as the universal standard for workshop reciprocating pumps operating at room temperature. Products such as Campbell Hausfeld ST1253 Air Compressor Oil and Milton 1002-32 High Performance Conventional Air utilize this 30-weight baseline to maintain film strength under continuous compression loads. This viscosity provides sufficient body to seal piston rings against cylinder walls while preventing excessive rotational drag on electric drive motors.
Colder operating environments necessitate a thinner fluid to ensure easy startup and rapid splash distribution. An ISO 46 lubricant, equivalent to an SAE 20 weight, flows freely in unheated garages and winter jobsite conditions where heavier 30-weight oil turns sluggish. TRIAX Kompressor ISO 46 SAE 20 demonstrates this cold-weather utility by reducing startup friction and helping prevent electric motor overload trips. When thick oil resists splash dispersal during a freezing startup, cylinder walls run starved of lubrication during the critical initial minutes of operation.
Intermediate applications often benefit from an ISO 68 viscosity grade, which sits neatly between light winter oils and heavy summer lubricants. Formulations such as TRIAX Kompressor ISO 68 provide balanced thermal stability across moderate seasonal shifts without requiring multiple fluid changes throughout the year. Choosing the wrong viscosity directly influences pump operating temperature, electric motor amperage draw, and volumetric air output. Consulting your compressor user manual confirms the precise ISO threshold required to balance mechanical sealing against hydrodynamic drag.
Full Synthetic Versus Conventional Mineral Compressor Oils
Conventional mineral oils derived from refined petroleum base stocks provide dependable, economical protection for light to medium shop duty. Blends such as DEWALT Compressor Oil D55001 and Mag 1 utilize refined petroleum stocks enriched with anti-wear and rust-inhibiting chemistries. These mineral options excel in home workshops and small auto garages where compressors run intermittently for short inflation, nailing, or bolting tasks. However, conventional mineral base stocks undergo accelerated oxidation and thermal thinning when subjected to extended, continuous duty cycles.
Full synthetic compressor lubricants represent a significant upgrade for continuous-duty commercial equipment and high-temperature operating environments. Premium formulations like Ingersoll Rand All Season Select Synthetic Air feature engineered synthetic base stocks designed to withstand extreme thermal conditions without breaking down. Synthetic molecules maintain uniform size and structure, allowing the fluid to resist shear thinning while maintaining higher flash points than standard mineral oils. This elevated thermal resistance prevents oil vaporization, which keeps harmful vapor mists out of downstream air lines and storage tanks.
Service life intervals highlight another practical difference between synthetic and petroleum base stocks. Mineral compressor oils typically require replacement every 250 to 500 operating hours, depending on shop dust levels and ambient temperatures. In contrast, advanced synthetic lubricants like the TRIAX Kompressor full synthetic series are formulated for extended service intervals across thousands of operating hours under controlled conditions. This extended operational life reduces equipment downtime, lowers ongoing maintenance waste, and provides reliable lubrication across multi-shift workshop schedules.
Matching Lubricants to Pump Mechanisms: Reciprocating, Rotary Screw, and Vane
Mechanical pump architecture dictates the exact physical and chemical demands placed upon crankcase fluid. Reciprocating piston pumps rely almost exclusively on splash or basic pressure-fed lubrication to protect connecting rods, wrist pins, and cast-iron cylinder bores. Heavy workshop setups, including stationary belt-drive workshop air compressors, routinely operate with single-stage or two-stage piston designs that require robust ISO 100 non-detergent oils. These reciprocating systems demand fluids with high film strength to withstand the severe reciprocating impact loads delivered by the piston on each compression stroke.
Rotary screw and rotary vane compressors operate under completely different mechanical principles that require specialized circulation oils. In a rotary screw pump, oil is injected directly into the compression chamber between the intermeshing helical rotors to cool the air charge, seal internal clearances, and lubricate the roller bearings. Oils designed for rotary screw systems, such as the multi-viscosity TRIAX Kompressor series, require exceptional thermal stability and rapid air-release properties. Foaming in a rotary screw pump disrupts cooling and leads to high-temperature thermal shutoffs, making specialized non-detergent synthetic fluid mandatory.
Clarifying the distinction between oil-lubricated pumps and oil-free designs prevents catastrophic mistakes during equipment maintenance. Many modern portable pancake and jobsite compressors feature oil-free pump mechanisms that utilize permanently lubricated bearings and Teflon-coated piston sleeves. These oil-free units do not possess a crankcase, dipstick, or oil drain plug, and adding oil to their air intakes or cylinders will permanently ruin the Teflon seals. Always verify whether your compressor pump contains an oil fill port and a sight glass before attempting any lubrication procedure.
Mechanical Symptoms and Operational Risks of Incorrect Lubricant Usage
Introducing the wrong fluid into a compressor crankcase produces distinct operational symptoms that alert attentive operators to developing mechanical damage. One common warning sign is rapid darkening and sludging of the oil, indicating thermal oxidation and carbon suspension. When automotive engine oils are used, the detergents bind to microscopic particles and turn the reservoir black within a few hours of operation. This suspended particulate acts as an abrasive slurry, polishing cylinder bores, widening ring gaps, and eroding bronze wrist pin bushings.
Reed valve failure serves as another classic consequence of improper oil selection. When mineral oils with low flash points or high detergent contents reach hot discharge ports, they vaporize and burn against the reed petals. This process creates hard carbon ridges that prevent the thin steel valves from forming a tight pneumatic seal against the valve seat. As a result, the pump loses volumetric efficiency, recovery times between tank cut-in and cut-out extend significantly, and the cylinder head runs dangerously hot.
Oil foaming within the crankcase introduces severe operational issues downstream in the pneumatic delivery system. Low-quality oils without dedicated anti-foam additives whip into a froth under the rapid action of the connecting rod dippers. This expanded foam reaches the bottom of the cylinder bore, bypasses the piston rings, and enters the compressed air stream in significant quantities. Downstream air tools, spray guns, and plasma cutters quickly become contaminated with atomized oil droplets, destroying paint finishes and clogging pneumatic tool motors.
Crankcase Servicing Protocol: Sight Glasses, Oil Levels, and Safe Drain Practices
Establishing a disciplined fluid inspection routine ensures your compressor pump operates reliably across its mechanical design life. Most modern oil-lubricated pumps feature a clear acrylic sight glass located near the bottom of the crankcase housing. The correct fluid level sits precisely in the center of the sight glass, often marked by a red central dot or between horizontal hash marks. Allowing the fluid level to drop below the bottom of the glass risks starving the dipper, while overfilling creates excessive fluid drag, frothing, and oil blow-by past the rings.
Proper maintenance timing depends heavily on the operating age of the machine and the frequency of shop usage. Brand new compressor pumps require an initial break-in fluid change, typically conducted after the first 20 to 50 hours of run time, to flush away metal seating particles. After this initial break-in period, conventional oils like Milton 1002 or Campbell Hausfeld ST1253 should be replaced every three to six months in active shops. Compressors filled with premium synthetic lubricants can sustain longer intervals, but annual fluid changes remain best practice to eliminate accumulated moisture and particulate contamination.
Safe execution of an oil change requires following standard pneumatic and electrical shop precautions. Always disconnect the compressor from its electrical power supply and discharge all stored tank air pressure completely before beginning maintenance work. Warm the pump slightly by running it for several minutes prior to service, as warm oil drains more thoroughly and carries suspended particles out of the sump. Remove the drain plug, allow the old fluid to empty completely into an approved container, reinstall the plug securely, and refill through the crankcase breather port to the sight glass center.
Practical Guidelines for Selecting Viscosity and Chemical Base
Choosing the ideal lubricant for your specific workshop environment boils down to evaluating ambient temperature, pump design, and workload intensity. For general garage duty with a reciprocating cast iron pump operating between 40°F and 90°F, standard ISO 100 non-detergent mineral oil provides exceptional, cost-effective protection. If you operate your compressor in an unheated workshop during harsh winter months, transitioning to an ISO 46 synthetic ensures dependable cold starts without tripping circuit breakers. Heavy commercial installations running high continuous air demands benefit most from dedicated full synthetic formulations that resist thermal breakdown under continuous duty cycles.
Always inspect the crankcase breather cap during every fluid top-off or oil replacement procedure. The breather vent allows atmospheric air to displace internal volume as pistons oscillate, preventing dangerous pressure buildup inside the crankcase. If dust, sawdust, or dried oil clogs the breather passages, rising internal crankcase pressure will force oil past crankshaft shaft seals and sight glass threads. Keeping this vent clean, monitoring fluid clarity through the sight glass, and strictly avoiding detergent automotive motor oils guarantees reliable pneumatic performance whenever you power on your shop compressor.
Taking a proactive approach to crankcase lubrication prevents costly mechanical breakdowns and preserves the efficiency of your pneumatic equipment. By sticking to non-detergent chemistries, matching ISO viscosity to your shop climate, and maintaining precise oil levels, you ensure your compressor pump operates smoothly for decades. Keep a spare bottle of manufacturer-approved oil on your workshop shelf so routine maintenance never gets delayed. Clean, high-grade oil remains the most cost-effective insurance policy available for any compressed air system.
About the author
Tony Carrick is an experienced product researcher and writer specializing in tools, home improvement, automotive maintenance, and consumer equipment. With extensive experience reviewing tools and tackling hands-on renovation projects, he brings a buyer-focused perspective to compressor performance, usability, and overall value.