
What Is a Rotary Screw Air Compressor: Mechanics, Operation, and Guide for 2026
Learn what is a rotary screw air compressor, how positive displacement rotors work, and which shop setup fits your CFM needs for October 2026.
 By Bob Beacham
Updated October 7, 2026

Industrial workshops running continuous sandblasters, paint spray booths, or CNC machinery frequently overwhelm traditional reciprocating piston compressors. Piston pumps generate intense friction heat, loud mechanical hammering, and rapid line pressure drops when operated past their modest duty cycle limits. Understanding what is a rotary screw air compressor helps fabricators and automotive technicians resolve these air delivery bottlenecks. Unlike reciprocating pumps that pulse air through cylinder strokes, rotary screw systems generate smooth, pulse-free pneumatic volume through interlocking helical rotors designed for non-stop continuous operation.
Modern production facilities demand steady line pressure without the frequent thermal shutdowns associated with consumer-grade equipment. Investing in a commercial rotary screw package provides a 100 percent continuous duty cycle, significantly lower operating noise, and superior electrical efficiency under sustained loads. Equipment from brands such as Compressed Air USA, Triax, LRSD, and HPDAVV highlights how rotary technology handles demanding pneumatic workloads across diverse commercial settings. Evaluating delivered airflow volume, electrical phase requirements, and routine lubrication maintenance ensures your facility selects an air system that performs reliably for decades.
| Award | Product | ACR Score About ACR ScoreThe ACR Score is our own rating from 0 to 10, based on performance, design and build, ease of use, and value. It reflects independent research and is never influenced by manufacturers, retailers, or affiliate commissions. Learn more › | |
|---|---|---|---|
| Best Overall |
XYZIL 54595442 Air Oil Separator Filter
|
8.9/10 | Buy |
| Best Value |
 Compressed Air USA XL 8000-Hour Oil, 1 Gal |
8.9/10 | Buy |
| Best Budget |
 TRIAX Kompressor ISO 46 SAE 20 Full Synthetic Air |
8.8/10 | Buy |
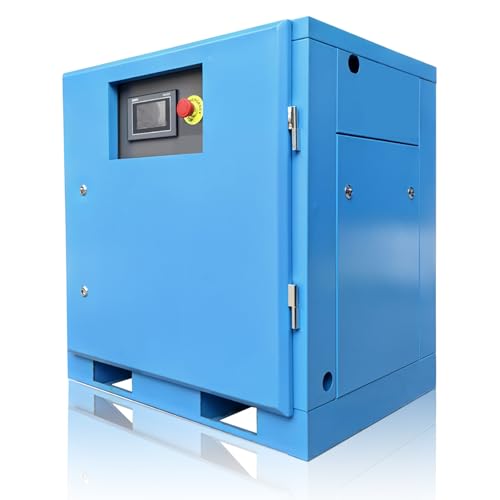 DCYL 10HP 230V Rotary Screw Compressor |
8.6/10 | Buy | |
 TRIAX Kompressor ISO 100 SAE 30 Full Synthetic Air |
8.3/10 | Buy | |
| Best Premium |
 LRSD 10HP 37.5 CFM Rotary Screw Compressor |
8.3/10 | Buy |
 LRSD 7.5HP 80-Gallon Screw Air Compressor |
8.1/10 | Buy | |
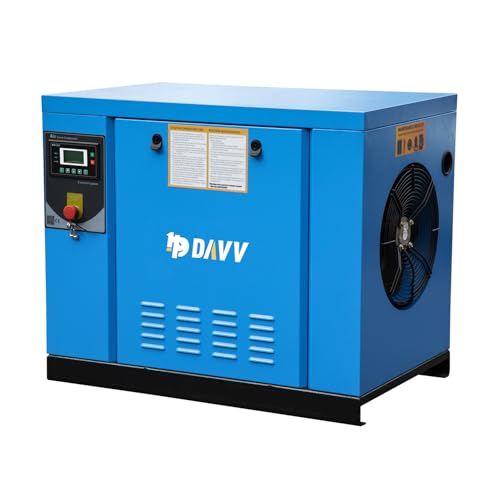 HPDAVV 10HP Rotary Screw Air Compressor |
7.8/10 | Buy |
XYZIL 54595442 Air Oil Separator Filter
This aftermarket air oil separator replaces Ingersoll Rand part numbers 54595442, 39831885, 42545368, and 39831888 on EP-30SE and EP-40SE rotary screw compressors. It provides a direct-fit replacement for shop technicians and facility managers looking to prevent oil carryover during scheduled maintenance.
Pros
- Direct interchange compatibility with multiple Ingersoll Rand cross-reference part numbers
- Cost-effective alternative to purchasing OEM branded replacement elements for routine service
- Maintains oil separation functionality to protect downstream shop air distribution lines
- Built specifically to match EP-30SE and EP-40SE series compressors with J-prefix serial numbers
Cons
- Aftermarket replacement rather than an original manufacturer Ingersoll Rand part
- Strict compatibility limited only to EP-30SE and EP-40SE units with serial numbers starting with J
- Requires physical verification of machine serial plates and cross-reference numbers prior to ordering
Compressed Air USA XL 8000-Hour Oil, 1 Gal
Formulated for rotary screw compressors, this synthetic blend delivers up to 8,000 hours of service life at elevated discharge temperatures. It mixes directly with existing OEM or aftermarket lubricants, eliminating the need for a full system drain before topping off.
Pros
- Long 8,000-hour service life under normal discharge heat
- No drain or flush required for system top-offs
- Broad compatibility with OEM and aftermarket equivalents
- Protects against wear, varnish, and moisture buildup
- Non-toxic and non-hazardous formulation
Cons
- Synthetic blend rather than a pure synthetic base
- Designed specifically for rotary screw air compressors
- One-gallon container may require multiple bottles for large units
TRIAX Kompressor ISO 46 SAE 20 Full Synthetic Air
TRIAX Kompressor ISO 46 SAE 20 is a commercial-grade, full-synthetic non-detergent lubricant engineered for oil-lubricated reciprocating, rotary screw, and vane air compressors. It provides reliable extreme-temperature wear protection and multi-viscosity all-season performance, making it an excellent maintenance choice for auto shops, contractors, and home garage workshops.
Pros
- Full synthetic non-detergent formulation extends pump life across severe operating conditions
- True all-season multi-viscosity rating maintains fluid flow from -49 deg F up to 140 deg F+
- Formulated to lower operating temperatures by up to 30% and eliminate oil vapor odor
- Compatible with a wide array of compressor pumps including reciprocating and rotary screw designs
Cons
- Not formulated for oil-free air compressors, breathing air systems, oxygen setups, or LPG gas pipelines
- Users must verify whether their pump manufacturer specifically calls for ISO 46 (SAE 20) rather than heavier ISO 68 or ISO 100 weights
- Requires careful manual crankcase draining and filling without an included pour spout
DCYL 10HP 230V Rotary Screw Compressor
Built for dedicated workshops needing steady airflow, this single-phase rotary screw unit delivers 39 CFM at up to 120 PSI. Its variable-speed motor automatically adjusts output to air demand, cutting down on power consumption and noise.
Pros
- High 39 CFM airflow on single-phase 230V power
- Variable speed operation conserves energy during low demand
- Pre-commissioned setup simplifies initial installation
- Soft start provides lower noise and smooth operation
Cons
- Cannot convert between single-phase and three-phase power
- Housing color ships randomly unless requested from seller
- Requires dedicated 208-230V high-amperage electrical service
TRIAX Kompressor ISO 100 SAE 30 Full Synthetic Air
TRIAX Kompressor ISO 100 SAE 30 is a commercial-grade, full synthetic non-detergent compressor oil formulated for reciprocating, rotary screw, and vane pumps operating across extreme temperature ranges. It is well-suited for shop owners, auto mechanics, and contractors seeking extended service intervals and cooler operating temperatures for their oil-lubricated compressors.
Pros
- True all-season multi-viscosity performance down to -49°F for dependable cold-weather pump startup
- Non-detergent synthetic blend reduces crankcase sludge, carbon deposits, and thermal breakdown
- Rated for up to 20,000 service hours, drastically extending maintenance intervals compared to mineral oils
- Compatible with a wide spectrum of reciprocating, screw, and vane compressor brands
Cons
- Not compatible with oil-free compressor designs or oxygen and liquid natural gas (LNG) equipment
- One-gallon container size may exceed the simple top-off needs of small single-stage portable units
- Carries a higher initial purchase price than basic mineral-based non-detergent compressor oils
LRSD 10HP 37.5 CFM Rotary Screw Compressor
Delivering 37.5 CFM at 125 PSI, this single-phase unit utilizes a permanent magnet variable speed drive to cut energy consumption during partial loads. Its compact footprint and straightforward maintenance schedule make it a strong continuous-duty air source for space-constrained workshops.
Pros
- Energy-saving permanent magnet variable frequency drive
- High 37.5 CFM output for demanding applications
- Compatible with 230V single-phase electrical connections
- Space-saving footprint suits tight workshop layouts
- Simplified routine maintenance for filters and oil
Cons
- Cannot convert between single-phase and three-phase power
- Substantial 213-pound weight limits machine portability
- Maximum working pressure is capped at 125 PSI
LRSD 7.5HP 80-Gallon Screw Air Compressor
Engineered for demanding fabrication and auto shops, this stationary rotary screw compressor combines an 80-gallon tank, dryer, and filtration system into a single plug-and-play assembly. Its IP55 sealed motor generates 29 CFM of continuous airflow while resisting airborne dust and moisture.
Pros
- All-in-one design combines compressor, tank, and dryer
- Delivers high 29 CFM output for continuous work
- Sealed IP55 motor endures dusty industrial environments
- Service factor of 1.15 tolerates short motor surges
- Large 80-gallon receiver ensures steady air volume
Cons
- Requires three-phase 230V commercial power hookup
- Large stationary footprint requires permanent shop floor space
- Substantial size makes moving difficult after placement
HPDAVV 10HP Rotary Screw Air Compressor
Built for heavy industrial operations, this 10-horsepower rotary screw compressor delivers dependable 125 PSI output with an integrated spin-on separator for reduced downtime. It requires a dedicated 460V three-phase power supply, making it an ideal fit for manufacturing plants, automotive shops, and commercial production facilities.
Pros
- Spin-on separator allows quick and clean maintenance
- Hinged service covers provide instant access to consumables
- Efficient microprocessor controller manages compressor operations
- Steady 33 CFM air output suited for industrial tools
Cons
- Requires high-voltage 460V to 480V three-phase electrical input
- Incompatible with single-phase power converters
The Mechanics, Operation, and Workshop Selection of Rotary Screw Compressors
A rotary screw air compressor is a positive displacement machine that pressurizes atmospheric air using a pair of precision-machined, intermeshing helical screws. Unlike reciprocating piston pumps that compress air in pulsating strokes, the continuous sweep of helical rotors pulls air smoothly into shrinking flute cavities. This positive displacement design delivers a steady, pulse-free stream of pressurized air without severe mechanical vibration or cycle lag. Commercial workshops and industrial production plants rely on this architecture when continuous operation demands dependable pneumatic volume around the clock.
How the Intermeshing Helical Rotor Mechanism Generates Pressurized Air
The core component of every rotary screw compressor is the cast iron air end housing two precision-engineered rotors. The driving male rotor features convex helical lobes that mesh seamlessly into the concave flutes of the driven female rotor. Atmospheric air enters the inlet port at one end of the stator housing, filling the open pockets created between the rotating lobes. As the motor turns the male and female rotors, the rotation moves past the inlet port and traps the air volume within the sealed flute channels.
Continued rotation forces the trapped air pocket along the length of the rotors toward the opposing discharge end. The geometry of the intermeshing flutes progressively reduces the physical volume of the pocket, compressing the air mechanically. Internal pressure rises smoothly until the flute reaches the discharge port, releasing the pressurized air into the delivery system. This continuous rotary sweep prevents the cyclic pressure spikes and mechanical hammer common in piston-driven workshop equipment.
Oil-Flooded Versus Oil-Free Rotary Screw Air Ends
Oil-flooded rotary screw compressors represent the primary choice for automotive collision shops, woodworking facilities, and general industrial manufacturing. Specialized synthetic oil injects directly into the compression chamber while the rotors turn under mechanical load. This synthetic fluid creates an essential sealing film across the microscopic rotor tolerances, preventing air from slipping backward toward the inlet. The circulating fluid also absorbs the intense thermal energy produced during rapid compression and lubricates the heavy-duty roller bearings.
Oil-free rotary screw designs operate without liquid lubricant inside the compression chamber, relying instead on precision external timing gears. These dry air ends utilize specialized polymer or Teflon rotor coatings to prevent metal-to-metal contact during high-speed rotation. Food packaging facilities, medical cleanrooms, and pharmaceutical labs require oil-free air to eliminate any possibility of hydrocarbon vapor contamination. Dry screw compressors generate significantly higher operating temperatures and require frequent maintenance checks compared to rugged oil-flooded models. Most mechanical repair garages and fabrication shops achieve exceptional air purity at lower cost by pairing oil-flooded units with downstream coalescing filters.
The Air-Oil Separation Process and Fluid Circulation
Pressurized air exiting an oil-flooded screw air end leaves as a turbulent mixture of hot compressed gas and atomized lubricant droplets. This mixture discharges into a primary separator reservoir where directional baffles spin the heavy oil droplets out of suspension. Fine microscopic oil mist then travels through a dedicated air-oil separator element, such as an XYZIL spin-on filter element. Coalescing media inside the separator forces minute oil droplets to merge into heavier fluid, which scavenger lines siphon back into the lower sump. This multi-stage separation process ensures downstream workshop air lines remain remarkably free of liquid lubricant carryover.
Scavenged compressor oil passes through a thermostatically controlled bypass valve and an air-cooled radiator core before returning to the rotors. Synthetic lubricants, such as Compressed Air USA XL extended life oil or Triax Kompressor ISO 46 fluids, resist high thermal breakdown and prevent varnish. Non-detergent formulations allow atmospheric moisture to settle at the base of the reservoir rather than emulsifying into the circulating oil stream. Standard automotive motor oils must never enter a screw compressor because detergent additives cause violent foaming and catastrophic separator failure.
Fixed-Speed Compressors Versus Variable Speed Drive Technology
Fixed-speed rotary screw compressors turn their electric drive motors at a steady, unchanging velocity whenever the power switch engages. When shop air demand falls below pump capacity, an inlet throttle closes to switch the unit into an unloaded idling cycle. The motor continues to consume significant electrical power during unloaded idling while producing zero usable compressed air for the facility. Manufacturing plants with constant, unchanging pneumatic consumption, such as automated stamping lines, operate fixed-speed compressors with high efficiency.
Variable speed drive compressors, such as the LRSD and DCYL 10 horsepower inverter-controlled machines, adjust motor speed to match real-time air consumption. An onboard microprocessor monitors system pressure drops and directs the frequency drive to accelerate or slow the permanent magnet motor instantly. Modulating motor speed eliminates wasteful unloaded idling intervals, reducing shop electrical power consumption during low-demand periods. Frequency drive electronics also provide gentle soft-start motor acceleration, protecting workshop electrical panels from massive starting amperage spikes.
Workshop Electrical Infrastructure and Voltage Specifications
Industrial facilities equipped with heavy production machinery typically rely on three-phase electrical power supplies for maximum motor efficiency. Compressors such as the HPDAVV 10 horsepower 35 CFM unit require 460-volt three-phase service to power their high-torque induction motors. Three-phase electricity distributes current evenly across three live conductors, allowing motors to run cooler and draw fewer operating amperes. Commercial facility managers must verify disconnect switches, wire sizing, and transformer ratings before installing large three-phase pneumatic machinery.
Smaller commercial shops, residential pole barns, and independent auto restoration garages often operate on standard single-phase 230-volt electrical panels. Single-phase rotary screw options, including the DCYL 10 horsepower machine, deliver impressive 39 CFM output without requiring three-phase utility connections. Manufacturer documentation explicitly warns against using cheap rotary or static phase converters to convert three-phase screw compressors to single-phase service. Dedicated breakers and heavy-gauge copper wiring prevent destructive voltage drops when high-capacity single-phase motors start under load.
All-In-One Integrated Systems Versus Modular Workshop Plumbing
Compact fabrication spaces often benefit from integrated 4-in-1 packages that house the entire pneumatic system on a single structural base. Units like the LRSD 7.5 horsepower package combine the rotary screw air end, an 80-gallon receiver tank, a refrigerated dryer, and filtration. Pre-plumbed factory packages eliminate the labor of running interconnecting copper piping between separate floor-mounted components. Integrated refrigerated dryers immediately cool the discharged air, condensing out moisture vapor before it can travel downstream into expensive tools. Auto painters, CNC plasma operators, and woodworkers obtain ultra-clean, dry compressed air right from the moment of initial installation.
Modular compressor setups place the standalone screw pump, large vertical storage vessels, and external drying towers in separate workshop locations. A modular layout allows expanding businesses to install auxiliary receiver tanks or upgrade filtration cartridges without replacing the primary air end. However, modular installations require careful planning of shop floor layout, rigid distribution manifolds, and dedicated condensate drain routing. Most small to mid-sized production garages prefer self-contained packages because they conserve floor space and simplify routine visual inspections.
Duty Cycle, Sound Output, and Piston Compressor Comparisons
Reciprocating piston compressors depend on rhythmic piston strokes inside cast iron cylinders, generating extreme friction and thermal stress. Most reciprocating workshop pumps require a 50 to 70 percent duty cycle, forcing operators to allow cooling pauses between run cycles. Rotary screw air ends operate on a continuous 100 percent duty cycle, allowing non-stop air production throughout multi-shift workdays. Constant oil circulation absorbs the thermal load immediately, preventing the valve plate fatigue and piston ring wear typical of overworked piston units.
Noise levels represent another major distinction between reciprocating piston equipment and modern rotary screw installations. Standard open-frame piston pumps frequently produce harsh, pulsating noise levels ranging between 80 and 88 decibels in enclosed garages. Rotary screw compressors feature balanced rotary motion and sound-dampening acoustic enclosures that keep operating sound remarkably smooth and quiet. Reduced sound pressure permits technicians to install the machine directly inside work bays without creating acoustic fatigue or workplace disruption.
Fluid Viscosity, Thermal Stability, and Lubrication Maintenance
Lubrication management dictates the long-term operational lifespan and mechanical reliability of any oil-flooded rotary screw system. Synthetic compressor fluids, such as Triax Kompressor ISO 46 and ISO 100 formulations, maintain stable protective films under extreme operating temperatures. An ISO 46 viscosity grade flows freely during cold morning startups while providing exceptional shear stability when the air end reaches operating temperature. Premium full-synthetic blends resist oxidation, carbon deposition, and varnish buildup across extended service intervals up to 8,000 operating hours. Maintaining proper fluid levels via the external sight glass prevents bearing starvation and ensures consistent heat dissipation through the oil cooler.
Regular fluid sampling and scheduled reservoir maintenance protect internal components from atmospheric moisture contamination. When compressors cycle intermittently in humid environments, water vapor condenses inside the separator vessel during extended cooling cycles. Operators should inspect the bottom tank drain valve prior to morning startups, opening the valve momentarily to release accumulated liquid water. Draining separated condensate before the pump circulates ensures clean oil lubricates the bearings, preventing corrosion and premature mechanical wear.
Filtration Schedules and Air End Wear Prevention
Contaminants entering the compressor intake can rapidly abrade the precision surfaces of spinning helical rotors. Heavy-duty intake air filters trap airborne sanding dust, metal shavings, and shop debris before atmospheric air enters the suction chamber. Restricted air filters reduce volumetric efficiency, causing the motor to pull higher electrical current while delivering diminished output CFM. Technicians should inspect intake elements weekly in dirty shop environments, replacing pleated cartridges according to manufacturer hour intervals.
The spin-on oil filter and air-oil separator element also require timely replacement to maintain system pressure balance. A clogged air-oil separator creates high differential pressure, restricting outgoing airflow and raising internal operating temperatures. Replacing oil filter cartridges during annual maintenance prevents circulating debris from scoring precision rotor faces or damaging roller bearings. Following rigid consumable replacement schedules ensures your rotary screw compressor operates with factory-level efficiency for tens of thousands of hours.
Calculating Pneumatic Demand to Select the Proper System Size
Sizing a rotary screw compressor requires calculating the simultaneous air volume consumption of all active pneumatic tools in your shop. Continuous tools like dual-action sanders, blast cabinets, and paint spray guns demand substantial CFM delivery at steady 90 to 125 PSI ratings. Underestimating air consumption forces a compressor to run below required line pressure, causing air tools to lose power and stall mid-job. Multiplying the total CFM requirements of your primary tools by a 1.25 factor provides an essential buffer for future equipment additions.
Matching calculated air volume with compressor horsepower and storage tank buffer capacity ensures seamless shop productivity. A 7.5 to 10 horsepower rotary screw unit delivering 29 to 39 CFM easily powers multiple high-draw automotive and woodworking tools simultaneously. Pairing the screw compressor with a generous 80-gallon receiver tank dampens line fluctuations and stores reserve volume for sudden surge demands. Choosing the correct configuration protects your pneumatic investments and ensures uninterrupted production across every demanding commercial shift.
Understanding the mechanical operation, fluid circulation, and electrical requirements of rotary screw compressors simplifies your workshop equipment decision. The combination of a 100 percent continuous duty cycle, pulse-free air delivery, and whisper-quiet operation makes rotary screw technology an exceptional upgrade over reciprocating piston pumps. Verifying shop voltage, selecting the right synthetic fluid, and maintaining filtration schedules ensures your system delivers reliable pneumatic power for years to come.
About the author
Bob Beacham is an experienced tools and workshop writer with deep knowledge of power equipment, mechanical systems, and practical DIY applications. His coverage of air compressors, welding equipment, saws, and workshop tools helps translate technical specifications into useful guidance for homeowners and serious DIYers.