
How to Check Cfm on Air Compressor: Practical Guide for 2026
Learn how to check cfm on air compressor with practical tank displacement calculations and timing steps in October 2026 to keep your shop tools powered properly.
 By Bob Beacham
Updated October 8, 2026

Air tools like sanders and paint sprayers demand continuous airflow, but many workshop compressors struggle to keep up when real delivery falls short of manufacturer labels. Motor ratings and marketing claims often promise high volume, yet unloader leaks, clogged intake filters, or pump wear can severely cut actual airflow. Knowing how to check cfm on air compressor setups gives operators a clear picture of true output before an important painting or mechanical project stalls. This simple diagnostic check helps avoid pneumatic tool damage, unexpected pressure drops, and wasted workshop hours.
Measuring airflow relies on straightforward physics rather than expensive testing equipment. By timing how rapidly a tank builds pressure across a known range, any shop owner can calculate realistic delivery at operating pressures like 90 PSI. Comparing these results against continuous tool requirements clarifies whether an existing compressor can handle high-demand tools or if an upgraded delivery system is necessary. Understanding actual delivery also protects equipment from thermal overload caused by continuous motor cycling.
| Award | Product | ACR Score About ACR ScoreThe ACR Score is our own rating from 0 to 10, based on performance, design and build, ease of use, and value. It reflects independent research and is never influenced by manufacturers, retailers, or affiliate commissions. Learn more › | |
|---|---|---|---|
| Best Overall |
Lhfacc 150 PSI In-Cab Air Compressor System
|
9.1/10 | Buy |
| Best Value |
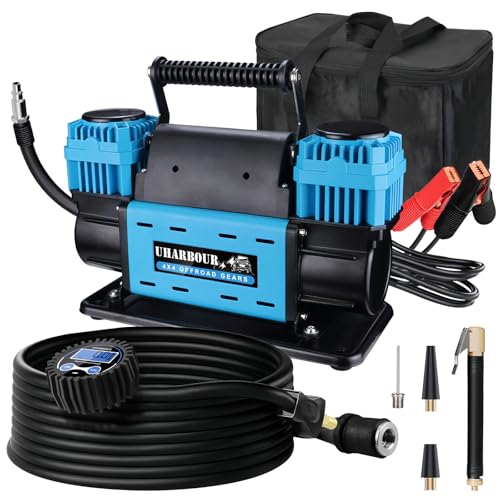 Uharbour 12V 12.35 CFM Air Compressor |
8.6/10 | Buy |
Lhfacc 150 PSI In-Cab Air Compressor System
Designed for trucks and vans, this tankless system allows drivers to monitor and adjust suspension air springs directly from the cab. Its 150 PSI compressor and electric paddle valve setup deliver fast leveling support without taking up excessive chassis space.
Pros
- Compact tankless layout saves valuable vehicle space
- Generates up to 150 PSI for quick leveling
- Real-time digital readout directly inside the cab
- Complete installation kit with relay and air lines
Cons
- Lacks a reserve tank for pre-pressurized air storage
- Requires routing airlines and electrical wiring into the cabin
Uharbour 12V 12.35 CFM Air Compressor
Equipped with dual motors, this heavy-duty compressor delivers a high 12.35 CFM airflow to reinflate off-road tires quickly after trail rides. An integrated digital gauge provides accurate pressure readings, though its 26-pound weight makes transport noticeably hefty.
Pros
- High 12.35 CFM output from dual motors
- Digital gauge provides clear, precise pressure control
- Rugged build designed for harsh trail environments
- Included storage bag keeps gear organized
Cons
- Heavy weight at over 26 pounds to haul
- Bulky dual-motor body requires substantial cargo room
Calculating and Verifying Air Compressor CFM Output
Measuring the true airflow of a workshop compressor provides clarity when operating pneumatic tools. Many operators wonder whether their pump delivers enough volume to sustain heavy grinders or spray guns without stalling mid-stroke. Verifying delivery through tank displacement testing reveals true performance under actual working conditions. This process cuts through exaggerated marketing claims and gives you reliable data for workshop planning.
Understanding CFM, SCFM, and Working Pressure
Cubic feet per minute, commonly abbreviated as CFM, measures the volume of air an air pump delivers at a specific resistance level. Most pneumatic tools specify their volume requirements at 90 PSI or 40 PSI, which represents the dynamic line pressure necessary for internal air motors to spin correctly. Standard cubic feet per minute, or SCFM, adjusts this measurement to standard atmospheric conditions, including sea level pressure and standard room temperature. When a compressor works against rising tank resistance, the volume of free air it moves naturally declines.
A compressor pump might displace a large volume of air at atmospheric pressure, but delivery shrinks as internal tank pressure climbs toward maximum cut-off levels. For example, a standard single-stage pump often delivers more CFM at 40 PSI than it can deliver at 90 PSI. Many manufacturers market displacement CFM, which calculates theoretical cylinder volume multiplied by motor RPM rather than delivered air. Checking delivered CFM reveals what actually enters the receiver tank, ensuring your pneumatic setup operates within realistic working parameters.
Tools and Data Required Before Testing
Testing tank CFM requires only a few basic items already present in most garages or workshops. You need a functioning receiver tank with a known volume listed on the manufacturer data plate, usually measured in US gallons. A reliable stopwatch or digital smartphone timer measures the precise duration of the test run. An accurate tank pressure gauge provides the starting and ending pressure points during the test interval.
Before starting any calculation, inspect the manufacturer data plate attached to the receiver shell. This metal tag specifies the water capacity or nominal gallon capacity of the pressure vessel. If the tank volume is stated only in liters, dividing the liter rating by 3.785 converts the volume to US gallons. Ensuring the tank is completely drained of condensed moisture before testing is also vital, because standing water reduces internal air volume and distorts your calculations.
Step-by-Step Tank Fill Timing Method
The standard procedure for measuring airflow relies on timing how quickly the pump fills the receiver tank between two specific pressure thresholds. Begin by opening the bottom tank drain valve to exhaust all stored compressed air, bringing the tank pressure gauge to zero PSI. Once all air escapes, close the drain valve tightly and inspect all quick-connect fittings to confirm no air leaks exist. Prepare your stopwatch before flipping the power switch to start the motor.
Start the compressor and stopwatch simultaneously, recording the exact seconds required for the tank to reach its automatic cut-off pressure. For an even more accurate assessment of working airflow, record split times between 0 PSI and 90 PSI, or between the cut-in pressure and cut-out pressure. The recovery cycle between cut-in and cut-out represents the realistic operating window where tools run during actual shop work. Note down the exact seconds taken, along with the precise starting and ending gauge pressures.
The Mathematical Formula for Calculating Real CFM
Converting tank fill time into CFM requires a standard pneumatic formula based on ideal gas laws. First, convert the tank capacity from gallons into cubic feet by dividing the total gallons by 7.48, which is the number of gallons in a cubic foot of space. Next, calculate the pressure difference by subtracting the starting gauge pressure from the final gauge pressure. This difference, known as delta PSI, reflects the total pressure accumulated during the timed interval.
Divide that pressure difference by 14.7, which represents standard atmospheric pressure at sea level, to determine the compression ratio across the test. Multiply the tank volume in cubic feet by this compression ratio to find the total cubic feet of free air pumped into the receiver. Finally, divide this free air volume by the fill time in seconds, and multiply the result by 60 to convert seconds into minutes. The resulting figure represents the actual delivered CFM of the air pump during that pressure cycle.
A Practical Calculation Walkthrough
Working through a concrete example clarifies how these mathematical values interact during an actual garage test. Suppose you have a workshop compressor with a 30-gallon storage tank that fills from 0 to 120 PSI in 180 seconds. First, divide 30 gallons by 7.48, which yields an internal tank volume of approximately 4.01 cubic feet. Next, subtract 0 PSI from 120 PSI to find a delta pressure of 120 PSI.
Dividing 120 PSI by 14.7 atmospheric pressure produces a compression factor of roughly 8.16 atmospheres. Multiplying 4.01 cubic feet by 8.16 gives approximately 32.72 cubic feet of atmospheric air compressed into the tank. Now, divide 32.72 cubic feet by the 180 seconds of elapsed fill time to find an output of 0.1817 cubic feet per second. Multiplying 0.1817 by 60 seconds yields a final delivered airflow rate of approximately 10.9 CFM across that full cycle.
If you instead measure only the recovery window from 90 PSI to 120 PSI, the delta pressure is 30 PSI. Dividing 30 by 14.7 yields a compression factor of 2.04 atmospheres, which results in roughly 8.18 cubic feet of free air moved. If this recovery cycle requires 55 seconds, dividing 8.18 by 55 and multiplying by 60 yields approximately 8.92 CFM. This lower output reflects the mechanical reality that pumps move less air as internal tank backpressure increases.
Why Measured CFM Differs from Manufacturer Labels
Workshop owners frequently discover that calculated CFM falls below the numbers advertised on product packaging. Many consumer compressors advertise peak displacement CFM, which represents theoretical pump volume rather than actual delivered air. Friction, heat buildup, and valve clearance spaces prevent any mechanical pump from achieving complete volumetric efficiency. Single-stage pumps especially suffer efficiency losses as compression ratios increase toward maximum shut-off pressures.
Environmental conditions also influence pneumatic test results in measurable ways. High ambient temperatures decrease air density, meaning the pump ingests fewer air molecules per stroke. High shop elevations further reduce atmospheric pressure, requiring more compression strokes to build equivalent gauge pressure. In addition, an intake air filter coated in sawdust or debris restricts incoming airflow, reducing volumetric efficiency before compression even begins.
Evaluating Tankless and Direct-Drive 12V Compressors
Specialized mobile air systems operate without a traditional receiver tank, making standard tank timing formulas inapplicable. For instance, the Lhfacc in Cab On Board Air Compressor System Air is designed specifically for direct suspension support, using paddle valves and a digital gauge to adjust air springs without a storage reservoir. Because these units feed directly into closed pneumatic bladders, measuring output focuses on inflation speed to a specific target pressure rather than calculated tank volume. Understanding how direct-feed systems function prevents misapplying standard tank volume calculations to tankless suspension kits.
Conversely, high-output portable offroad compressors like the Uharbour 12V 12.35 CFM Offroad Air Compressor boast substantial volumetric ratings designed to seat tire beads and inflate large offroad tires rapidly. Direct 12V tire inflators typically state open-flow CFM at zero backpressure alongside reduced delivery at 30 or 40 PSI. To test these units practically, operators often time how quickly the compressor raises a tire of known volume from a trail pressure like 15 PSI to street pressure like 35 PSI. This empirical timing approach provides an accurate assessment of portable tire inflation speed under realistic field conditions.
Matching Measured CFM to Common Pneumatic Tools
Knowing your compressor’s true output prevents frustrating tool stalls and erratic performance during demanding tasks. Intermittent tools such as brad nailers, framing guns, and staple guns consume minimal volume, usually requiring under 1 CFM at 90 PSI. Because fastener tools fire in brief bursts, a modest pump with a small buffer tank easily keeps pace with normal nailing cadences. Even compact jobsite compressors can support multiple trim carpenters when tools fire intermittently.
Continuous pneumatic tools present a completely different challenge for air delivery systems. Dual-action orbital sanders, high-speed die grinders, and HVLP paint spray guns demand continuous volume, often requiring 8 to 15 CFM at 90 PSI. If your timed calculation reveals an actual output of only 5 CFM, running a 10 CFM sander will drain the storage buffer in seconds. Once tank pressure drops below the working threshold, the tool stalls while the pump runs continuously, causing motor overheating and uneven workpiece finishes.
Diagnosing and Correcting Low CFM Output
When tank testing reveals an unexpectedly low CFM figure, systematic troubleshooting helps isolate the cause. Begin by checking for external air leaks around manifold fittings, quick-connect couplers, and the pressure regulator knob using soapy water. A tiny hiss from a loose fitting or cracked whip hose can bleed significant volume during a test cycle. Inspect the tank drain valve at the bottom of the cylinder to verify that it seals completely when closed.
Internal mechanical wear is another common culprit behind reduced airflow rates in older workshop units. Worn reed valves or cracked valve plates allow compressed air to slip backward into the intake stroke, sharply reducing volumetric delivery. In oil-free pumps, the Teflon piston ring and cylinder sleeve gradually wear down over hundreds of run hours, increasing blow-by around the piston seal. Cleaning the intake filter sponge, inspecting unloader valves, and replacing worn valve assemblies often restores lost pumping efficiency.
Operational Safety and System Maintenance
Conducting pneumatic performance checks requires attention to workshop safety rules and system integrity. Never exceed the maximum working pressure stamped on the receiver vessel or bypass factory pressure switch cut-offs to achieve higher numbers. Periodically inspect the ASME safety relief valve ring by pulling it briefly under low pressure to ensure the internal spring moves freely. Inspect electrical connections to confirm the motor draws power from a properly sized circuit, preventing dangerous voltage drops during extended test runs.
Regular maintenance keeps your compressor operating at its peak calculated CFM output season after season. Drain condensation from the receiver tank after every operating session to protect internal steel surfaces from rust and preserve total air storage volume. For oil-lubricated pumps, monitor oil levels in the sight glass and replace fluid with non-detergent compressor oil according to manufacturer guidelines. Clean intake air filters regularly to ensure the pump breathes freely without unnecessary inlet restriction.
Testing the actual airflow of your air compressor removes guesswork from tool selection and equipment upgrades. Whether you manage a stationary workshop tank or portable field gear, knowing your true CFM output ensures smooth tool operation and protects mechanical components from premature failure. Regularly verifying system performance keeps your pneumatic tools running efficiently and helps identify maintenance issues before they cause costly shop downtime.
About the author
Bob Beacham is an experienced tools and workshop writer with deep knowledge of power equipment, mechanical systems, and practical DIY applications. His coverage of air compressors, welding equipment, saws, and workshop tools helps translate technical specifications into useful guidance for homeowners and serious DIYers.