
How to Build a Gas Powered Air Compressor: A Practical Assembly and Sizing Guide for 2026
Learn how to build a gas powered air compressor essentials with our complete assembly and component sizing guide updated for October 2026.
 By Glenda Taylor
Updated October 7, 2026

Remote job sites, agricultural fields, and mobile service trucks frequently require heavy pneumatic power where electrical outlets are completely unavailable. Understanding how to build a gas powered air compressor requires a thorough grasp of how mechanical power transfers from an internal combustion engine to a reciprocating piston pump without relying on electric pressure switch cycling. Operating high-demand tools such as impact wrenches, framing nailers, and spray guns off the grid depends on matching engine output, pump displacement, and storage tank volume. Evaluating your pneumatic delivery needs starts with consulting a reliable air compressor CFM rating guide to ensure your hardware can sustain required flow rates under pressure.
Assembling a custom pneumatic rig gives mechanics and contractors the flexibility to tailor air delivery, whether you need a compact wheelbarrow setup or a high-output truck bed system. Critical components such as continuous-run pilot unloader valves, cast-iron compressor pumps, and engine throttle controls work in harmony to prevent engine stalling and hazardous over-pressurization. A successful build balances safety standards with mechanical efficiency, ensuring that every fitting, pulley, and relief valve meets rigorous jobsite demands.
| Award | Product | ACR Score About ACR ScoreThe ACR Score is our own rating from 0 to 10, based on performance, design and build, ease of use, and value. It reflects independent research and is never influenced by manufacturers, retailers, or affiliate commissions. Learn more › | |
|---|---|---|---|
| Best Overall |
HPDAVV 6.5HP 9-Gallon Gas Air Compressor
|
9.2/10 | Buy |
| Best Value |
 HPDMC 6.5HP Gas 9-Gallon Air Compressor |
9.2/10 | Buy |
| Best Premium |
 XtremepowerUS 13.0HP Horizontal Air Compressor |
9.2/10 | Buy |
| Best Budget |
 Albott 6.5HP 8-Gallon Gas Air Compressor |
9.1/10 | Buy |
 VEVOR 9-Gallon 6.5HP Gas Air Compressor |
8.9/10 | Buy | |
 Klutch 4-Gallon 6.5 HP Pontoon Air Compressor |
8.6/10 | Buy | |
 VEVOR 13.2-Gallon 7HP Gas Air Compressor |
8.6/10 | Buy | |
 Albott 13HP Gas Air Compressor |
8.6/10 | Buy | |
 VEVOR 15HP Gas-Powered Air Compressor |
8.6/10 | Buy | |
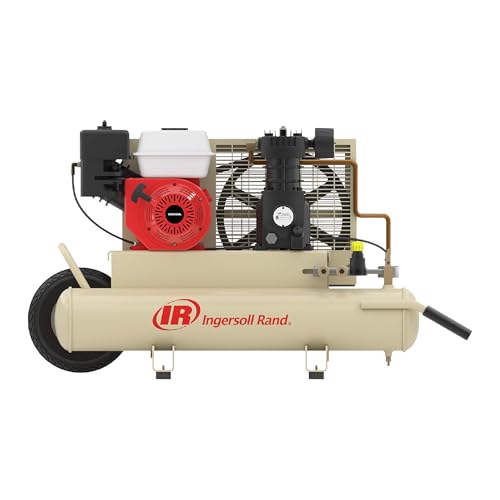 Ingersoll Rand SS3J5.5GH-WB 5.5 HP Compressor |
8.3/10 | Buy |
HPDAVV 6.5HP 9-Gallon Gas Air Compressor
Built for remote job sites and mobile service trucks, this gas-powered unit delivers 12 CFM at up to 125 PSI using a durable cast iron pump. Its wheelbarrow frame and vehicle-mount capability make it a dependable workhorse for field mechanics and heavy air tools where electricity is unavailable.
Pros
- High 12 CFM airflow runs demanding pneumatic equipment
- Cast iron pump head provides long-term mechanical durability
- Wheelbarrow frame simplifies transport across rough job sites
- Truck-mountable base adds versatility for field service
Cons
- Max pressure tops out at 125 PSI
- Gasoline engine requires regular engine maintenance and outdoor venting
- Large footprint takes up substantial bed space in vehicles
HPDMC 6.5HP Gas 9-Gallon Air Compressor
Delivering 12 CFM at up to 125 PSI, this gas-driven compressor offers robust off-grid pneumatic power for remote jobsites and service trucks. Its cast iron pump running at a low 880 RPM ensures steady output and long component life for demanding industrial tools.
Pros
- High 12 CFM output powers demanding air tools
- Low 880 RPM pump speed extends operating life
- Durable cast iron frame and cylinder construction
- Easily mounts to service trucks or utility beds
Cons
- Heavy 199-pound weight makes transport cumbersome
- Gasoline engine requires well-ventilated outdoor operation
- Maximum working pressure capped at 125 PSI
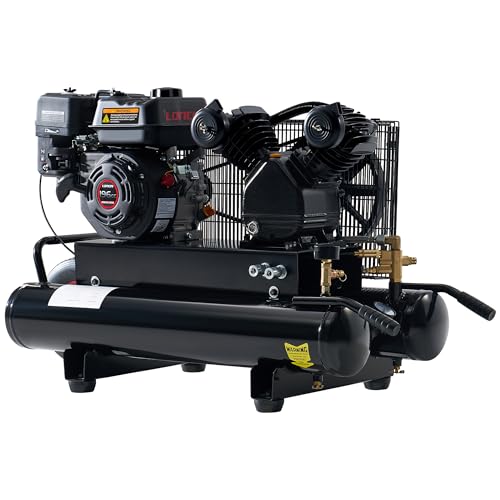
Albott 6.5HP 8-Gallon Gas Air Compressor
Built for off-grid job sites, this gas-powered unit delivers reliable pneumatic power with a 6.5 HP engine and a two-cylinder cast iron pump. Dual air outlets let two operators run tools simultaneously without depending on electrical hookups.
Pros
- Rugged cast iron pump and frame construction
- Dual air outlets support two simultaneous tools
- Gas-powered design eliminates need for electrical outlets
- Automatic safety valve ensures steady pressure management
Cons
- Very heavy at 166 pounds
- Modest 115 PSI maximum working pressure
- Substantial footprint requires ample vehicle cargo space
VEVOR 9-Gallon 6.5HP Gas Air Compressor
Built for remote jobsites without electrical access, this gas-driven unit supplies a dependable 9 CFM output from its 6.5HP engine. Dual outlets let two operators work simultaneously, though managing its 145-pound frame demands notable physical effort.
Pros
- High 9 CFM output drives demanding air tools
- Dual outlets support two operators at once
- Independent gas power works anywhere outdoors
- Fast 105-second tank fill time
Cons
- Heavy weight exceeds 145 pounds
- Maximum pressure capped at 115 PSI
- Produces gas exhaust requiring strict outdoor use
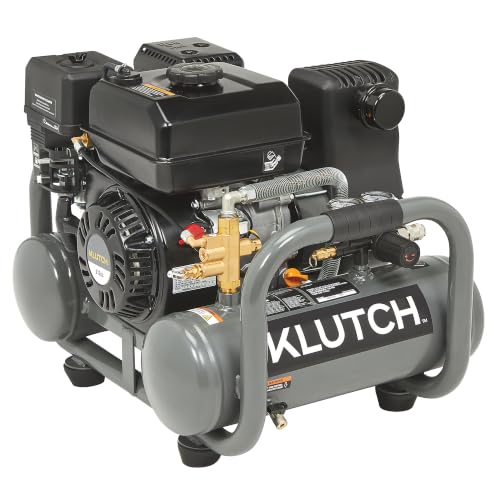
Klutch 4-Gallon 6.5 HP Pontoon Air Compressor
Built for remote jobsites without electrical power, this gas-powered compressor combines a 212cc engine with a 155 max PSI pontoon tank. It provides capable airflow for pneumatic tools, though its 88.2-pound frame requires substantial lifting effort.
Pros
- Runs without electrical outlets via 212cc gas engine
- High 155 max PSI operating pressure
- Provides 5 CFM at 90 PSI for pneumatic tools
- Sturdy 4-gallon pontoon tank structure
Cons
- Heavy 88.2-pound weight reduces portability
- Modest 4-gallon capacity limits continuous air reserves
VEVOR 13.2-Gallon 7HP Gas Air Compressor
Built for job sites lacking electrical hookups, this gas-powered VEVOR unit pairs a 7HP engine with dual outlets to run two pneumatic tools simultaneously. The 9 CFM delivery rate at 115 PSI ensures fast recovery times for outdoor construction and workshop tasks.
Pros
- Dual outlets operate two pneumatic tools at once
- Strong 9 CFM airflow provides rapid air delivery
- Automatic low-oil shutoff prevents pump damage
- Sturdy cast iron cylinders and frame construction
Cons
- Heavy unit weighing over 131 pounds
- Maximum pressure limited to 115 PSI
- Gas-powered design requires regular engine maintenance
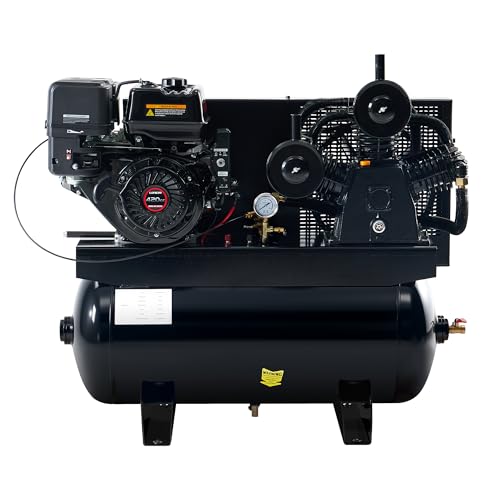
Albott 13HP Gas Air Compressor
The Albott 13HP Gas Air Compressor combines a 30-gallon ASME-certified tank with a 3-cylinder cast iron pump delivering 18 CFM at 90 PSI and up to 180 PSI maximum pressure. It is designed for service truck operators, mobile mechanics, and remote jobsite crews needing high-volume pneumatic airflow without electrical grid access.
Pros
- Delivers a listed 18 CFM at 90 PSI to easily operate high-demand pneumatic tools like heavy impact wrenches and spray guns off the grid
- Rugged 3-cylinder cast iron pump and frame reduce deformation and wear under demanding work conditions
- Substantial 30-gallon ASME-certified horizontal tank provides a reliable air buffer and reduces engine cycle frequency
- Total independence from 120V electrical outlets, eliminating blown household breakers and extension cord voltage drops
Cons
- Substantial dry weight of 344 pounds requires mechanical lifting equipment or permanent truck bed mounting rather than hand carrying
- Internal combustion engine produces exhaust fumes and high sound levels, restricting operation strictly to well-ventilated outdoor areas
- Requires dual routine maintenance schedules for both the gas engine and the oil-lubricated 3-cylinder compressor pump
VEVOR 15HP Gas-Powered Air Compressor
Delivering an impressive 33 CFM at 115 PSI, this 15HP gas-driven VEVOR compressor features a 30-gallon horizontal tank and cast-iron pump for demanding off-grid jobsites. It is an ideal pneumatic solution for framing crews, mobile mechanics, and commercial workshops needing high-volume airflow without electrical hookups.
Pros
- High airflow delivery of 33 CFM at 115 PSI easily runs demanding commercial pneumatic tools.
- Gas-powered 15HP engine operates completely independently without requiring 120V or 240V electrical connections.
- Rugged cast-iron pump cylinders and automatic low-oil shut-off ensure dependable mechanical protection.
- Generous 30-gallon horizontal air reservoir features dual outlets for simultaneous multi-tool operation.
Cons
- Substantial dry weight of 271 pounds requires ramps, a liftgate, or multiple people to transport into a truck bed.
- Maximum operating pressure is capped at 115 PSI, which is lower than multi-stage 150 to 175 PSI systems.
- Gasoline engine requires strictly outdoor, well-ventilated operation along with routine engine oil and fuel maintenance.
Ingersoll Rand SS3J5.5GH-WB 5.5 HP Compressor
Built for rugged jobsites lacking electrical hookups, this wheelbarrow-style compressor pairs a 5.5 HP Honda engine with durable cast-iron construction. It delivers continuous 135 psi operation and supports two pneumatic tools simultaneously.
Pros
- Durable cast iron pump construction
- Reliable 5.5 HP gas-powered Honda engine
- Rated for 100% continuous duty operation
- Dual quick disconnects for multi-tool use
Cons
- Heavy 226-pound weight makes vehicle loading difficult
- Modest 0.825-gallon fuel tank requires frequent refilling
Engineering and Assembling a Gas-Powered Air Compressor System
Fabricating or assembling a gasoline-driven air compressor requires a clear understanding of mechanical power transfer and pneumatic safety. Unlike standard workshop compressors that plug into a wall and cycle on and off using an electric pressure switch, a gas-powered rig operates under continuous engine rotation. Every mechanical junction, from the engine drive shaft to the tank manifold, must withstand substantial vibration and high thermal loads. Getting the configuration right ensures reliable compressed air delivery in remote locations where grid power is absent.
Core Mechanical Principles of Continuous-Run Pneumatic Systems
Electric compressors rely on an electromechanical pressure switch to cut motor power whenever the tank reaches its maximum cut-out pressure. Gasoline engines cannot quickly stop and restart on demand, so a gas-powered system must utilize a continuous-run pilot unloader valve mechanism. When storage tanks reach target pressure, the pilot valve directs air to open the pump intake valves or vent pump discharge air safely into the atmosphere. This mechanical venting eliminates pumping resistance, allowing the engine to idle down without building dangerous internal tank pressure.
Selecting between single-stage and two-stage pump architectures determines the operating pressure ceiling and efficiency of the build. Single-stage pumps compress atmospheric air directly into the storage reservoir in one piston stroke, typically topping out around 115 to 135 PSI. Two-stage pumps compress air in a large low-pressure cylinder, route it through finned intercooler tubing, and compress it further in a smaller high-pressure cylinder up to 175 PSI. Heavy service truck installations and industrial pneumatic machinery usually benefit from two-stage units, while portable framing and wheelbarrow rigs perform reliably with single-stage pumps.
Calculating Engine Horsepower and Matching Compressor Pump Displacement
Pneumatic pumps require substantial rotational torque to compress air against rising tank pressure. As a standard engineering rule of thumb, single-stage cast-iron pumps demand approximately one horsepower of gas engine output for every two to three CFM of delivered airflow. A 6.5 horsepower small engine typically drives a pump producing roughly 9 to 12 CFM at 90 PSI, which is well suited for running multiple framing nailers or impact wrenches. Larger industrial demands, such as commercial sandblasting or high-volume paint sprayers, demand 13 to 15 horsepower engines capable of driving pumps that deliver 18 to 33 CFM.
Mismatched components lead directly to engine stalling, pump overheating, or catastrophic mechanical failure. Coupling an oversized pump to an underpowered engine causes the engine to bog down and stall as tank pressure climbs toward maximum operating limits. Conversely, driving an undersized pump with excessive horsepower risks over-spinning the pump crankshaft beyond its rated speed. Matching the torque curve of a four-stroke OHV engine to the pump displacement ensures consistent air buildup without thermal overload.
Pulley Ratio Calculations and Belt Drive Mechanics
Small commercial gas engines run at a governed operating speed of approximately 3,600 RPM under load. In contrast, heavy-duty cast-iron compressor pumps operate most efficiently between 700 and 1,200 RPM to keep operating temperatures low and prolong valve plate life. Achieving the correct pump speed requires precise pulley sizing based on the ratio between the engine drive pulley and the pump flywheel. The formula divides the engine RPM by the desired pump RPM to establish the exact pitch diameter ratio needed for the drive pulleys.
Proper drive belt tension and pulley alignment prevent belt slippage, excessive bearing side-load, and premature V-belt destruction. For detailed belt replacement practices, reviewing our guide on how to change a compressor belt provides helpful mechanical principles regarding proper pulley alignment and tensioning. Using a heavy cast-iron flywheel with integrated cooling fan blades pulls air directly across the cylinder heads during operation. Steel belt guards must always enclose the entire drive assembly to prevent accidental contact with spinning pulleys and flying jobsite debris.
Pneumatic Pilot Unloader Valves and Throttle Slow-Down Controls
The pilot unloader valve acts as the primary brain of a continuous-run gasoline air compressor system. This brass valve monitors air pressure inside the main storage tank and actuates when the pressure reaches the predetermined cut-out threshold. Upon reaching cut-out pressure, the pilot valve redirects a small stream of pressurized air through a copper or nylon control line to the pump unloader head. This signal holds the intake valves open, allowing the pistons to cycle freely without drawing or compressing additional air.
Simultaneously, the pilot valve routes air to an engine throttle control cylinder, commonly referred to as an engine slow-down control. This pneumatic piston pulls the engine throttle arm back to low idle speed while the compressor pump is unloaded, saving fuel and reducing operational noise. Once air tools consume tank pressure down to the cut-in threshold, the pilot valve exhausts the signal air. The throttle control returns the engine to full governed operating speed, and the pump resumes compressing air into the storage reservoir.
Tank Selection, Structural Mounting, and Vibration Isolation
Selecting a certified pressure vessel is the single most critical structural decision in assembling a safe air compressor. Storage tanks must carry an authentic ASME certification stamp, proving that the vessel has undergone rigorous metallurgical pressure testing. Twin-tank wheelbarrow designs ranging from 4 to 9 gallons offer low centers of gravity and exceptional portability across rough construction jobsites. Stationary service truck builds generally utilize 30-gallon horizontal tanks that provide ample air buffering to reduce frequent throttle cycling during heavy tool usage.
Gas engines produce intense, continuous vibration that can rapidly induce metal fatigue in rigid mounting plates and pneumatic fittings. The engine and pump must be bolted securely to a rigid steel deck equipped with heavy-duty rubber vibration isolation dampeners. Rigid plumbing lines should never connect directly between a vibrating pump head and a rigid tank port without a flexible braided stainless steel discharge hose. Isolating mechanical resonance prevents weld cracking on tank support legs and eliminates loose structural fasteners.
Essential Safety Plumbing: Check Valves and Pressure Relief Hardware
Every custom compressor build requires an in-tank one-way check valve installed directly at the primary tank inlet port. This brass check valve allows compressed air from the pump discharge tube to enter the tank while preventing stored high-pressure air from backflowing into the pump. When the engine idles down and the unloader valve actuates, the check valve holds tank pressure securely inside the reservoir. Without a functional check valve, stored air would instantly escape through the unloader exhaust port.
Safety relief valves represent the final line of defense against catastrophic tank rupture or mechanical over-pressurization. An ASME-coded safety pop-off valve must be threaded directly into an independent tank bung, sized to discharge air faster than the pump can produce it. Never install a shutoff valve between the safety relief valve and the storage tank. Furthermore, a secondary safety valve installed directly on the pump discharge manifold protects cylinder head gaskets in case the main discharge line becomes obstructed.
Pump and Engine Lubrication System Requirements
Gas engines and reciprocating air compressor pumps operate under distinct thermal conditions and demand completely separate lubrication formulas. Small four-stroke gasoline engines require standard detergent motor oils engineered to suspend combustion blow-by and carbon soot. In stark contrast, cast-iron compressor pumps require non-detergent reciprocating compressor lubricants, such as ISO 68 or ISO 100 industrial oil. Standard automotive oil contains detergent additives that will cause severe foaming, carbon buildup on pump reed valves, and premature pump failure.
Maintaining correct fluid levels across both components prevents expensive mechanical breakdowns during long work shifts. If you are unsure which viscosity rating suits your climate, our guide on recommended compressor pump oil clarifies the differences between synthetic and mineral based formulas. Oil sight glasses on the pump crankcase should be checked prior to every engine start to ensure splash lubrication dippers receive adequate oil coverage. Low-oil safety shutdown switches installed on modern engines further protect hardware from seizing during off-camber operation on sloped jobsites.
Initial Break-In Procedure, Calibration, and Verification
Starting a newly assembled gas air compressor under full working pressure can score cylinder walls and ruin fresh piston rings. The initial startup requires a zero-pressure break-in period lasting approximately twenty to thirty minutes with the tank drain petcock fully open. Running the engine at moderate speed allows oil to circulate thoroughly through the pump crankcase, seating the rings and bedding the bearings without compression resistance. After completing the open-air run, close the drain valve and observe the pressure rise steadily across the tank gauge.
Verifying the exact cut-out and cut-in calibration of the pilot unloader valve ensures safe, automatic operation. As tank pressure approaches the rated operating ceiling, typically between 115 and 135 PSI depending on the pump rating, confirm that the pilot valve exhausts air smoothly. The engine should immediately drop to idle speed while the tank pressure stabilizes without leaking. Spraying soapy water around all threaded NPT fittings, compression ferrules, and check valve joints confirms zero air leakage under static storage pressure.
Evaluating Custom Fabrication Against Factory Commercial Assemblies
Building a gas-powered compressor from individual salvage parts offers substantial satisfaction, but sourcing certified individual components presents significant cost and safety challenges. Sourcing a new commercial OHV engine, a cast-iron pump, an ASME certified tank, unloader hardware, pulleys, and guards individually often costs more than purchasing a pre-engineered factory unit. Factory built units from reputable manufacturers arrive with pre-calibrated throttle linkages, certified EPA emissions compliance, and harmonized pulley ratios engineered for maximum pump longevity.
Service contractors and mobile mechanics often find that commercial models provide dependable reliability backed by verified manufacturer specifications. Wheelbarrow compressors equipped with 5.5 to 6.5 horsepower engines deliver turn-key mobility with built-in roll cages, while large 30-gallon horizontal models provide massive volume for heavy industrial equipment. If you choose to assemble your own rig, adhere strictly to certified ASME standards, inspect safety valves regularly, and prioritize proper component balancing for safe, reliable off-grid pneumatic power.
About the author
Glenda Taylor has extensive experience in residential construction, remodeling, home improvement, and tool use. Her practical approach to equipment evaluation focuses on usability, performance, safety, and value—helping DIYers and workshop users make better-informed decisions about compressors and related tools.