
How to Build a Gas Air Compressor: A Practical Guide for 2026
Learn how to build a gas air compressor with the right engine, pump, and pilot valve controls for reliable jobsite power in October 2026.
 By Tom Scalisi
Updated October 8, 2026

Remote jobsites, mobile service trucks, and agricultural fields rarely offer the dedicated 240-volt electrical circuits required to run high-output shop compressors. Relying on long extension cords plugged into standard 15-amp outlets often trips breakers and starves electric motors of necessary voltage, stalling critical framing or repair work. Understanding how to build a gas air compressor gives contractors and mechanics the freedom to generate high-volume airflow anywhere without relying on utility power. Gasoline-driven configurations provide dependable CFM output at 90 PSI to run multiple framing nailers, heavy impact wrenches, or continuous spray equipment simultaneously.
Building or assembling a gas-powered pneumatic setup requires careful component matching rather than simply bolting an engine to an existing pump. Because small gas engines run continuously rather than cycling on and off like electric motors, the system depends on specialized continuous-run pilot unloader valves and engine throttle controls. Selecting a cast-iron reciprocating pump, calculating exact pulley ratios, and securing an ASME-rated receiver tank are critical steps for long-term reliability. By focusing on proven mechanical layouts and essential safety relief systems, you can assemble a rugged, independent pneumatic rig built for demanding field conditions.
| Award | Product | ACR Score About ACR ScoreThe ACR Score is our own rating from 0 to 10, based on performance, design and build, ease of use, and value. It reflects independent research and is never influenced by manufacturers, retailers, or affiliate commissions. Learn more › | |
|---|---|---|---|
| Best Overall |
HPDAVV 6.5HP 9-Gallon Gas Air Compressor
|
9.2/10 | Buy |
| Best Budget |
 Albott 6.5HP 8-Gallon Gas Air Compressor |
9.1/10 | Buy |
| Best Value |
 VEVOR 9-Gallon 6.5HP Gas Air Compressor |
8.9/10 | Buy |
 VEVOR 13.2-Gallon 7HP Gas Air Compressor |
8.6/10 | Buy | |
| Best Premium |
 Albott 13HP Gas Air Compressor |
8.6/10 | Buy |
 Generic 40-Gallon 15HP Gas Air Compressor |
8.0/10 | Buy | |
 EVIL ENERGY 12V 1-Gallon Air Tank and Compressor |
7.8/10 | Buy | |
 Metabo HPT EC2510E 8-Gallon Air Compressor |
7.8/10 | Buy | |
 Metabo HPT EC2610EA 9-Gallon Gas Compressor |
7.8/10 | Buy |
HPDAVV 6.5HP 9-Gallon Gas Air Compressor
Built for remote job sites and mobile service trucks, this gas-powered unit delivers 12 CFM at up to 125 PSI using a durable cast iron pump. Its wheelbarrow frame and vehicle-mount capability make it a dependable workhorse for field mechanics and heavy air tools where electricity is unavailable.
Pros
- High 12 CFM airflow runs demanding pneumatic equipment
- Cast iron pump head provides long-term mechanical durability
- Wheelbarrow frame simplifies transport across rough job sites
- Truck-mountable base adds versatility for field service
Cons
- Max pressure tops out at 125 PSI
- Gasoline engine requires regular engine maintenance and outdoor venting
- Large footprint takes up substantial bed space in vehicles
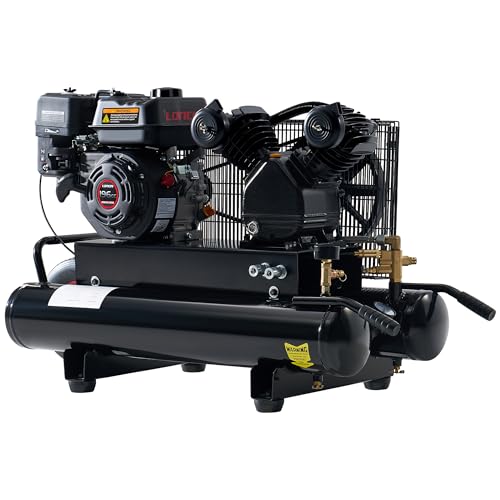
Albott 6.5HP 8-Gallon Gas Air Compressor
Built for off-grid job sites, this gas-powered unit delivers reliable pneumatic power with a 6.5 HP engine and a two-cylinder cast iron pump. Dual air outlets let two operators run tools simultaneously without depending on electrical hookups.
Pros
- Rugged cast iron pump and frame construction
- Dual air outlets support two simultaneous tools
- Gas-powered design eliminates need for electrical outlets
- Automatic safety valve ensures steady pressure management
Cons
- Very heavy at 166 pounds
- Modest 115 PSI maximum working pressure
- Substantial footprint requires ample vehicle cargo space
VEVOR 9-Gallon 6.5HP Gas Air Compressor
Built for remote jobsites without electrical access, this gas-driven unit supplies a dependable 9 CFM output from its 6.5HP engine. Dual outlets let two operators work simultaneously, though managing its 145-pound frame demands notable physical effort.
Pros
- High 9 CFM output drives demanding air tools
- Dual outlets support two operators at once
- Independent gas power works anywhere outdoors
- Fast 105-second tank fill time
Cons
- Heavy weight exceeds 145 pounds
- Maximum pressure capped at 115 PSI
- Produces gas exhaust requiring strict outdoor use
VEVOR 13.2-Gallon 7HP Gas Air Compressor
Built for job sites lacking electrical hookups, this gas-powered VEVOR unit pairs a 7HP engine with dual outlets to run two pneumatic tools simultaneously. The 9 CFM delivery rate at 115 PSI ensures fast recovery times for outdoor construction and workshop tasks.
Pros
- Dual outlets operate two pneumatic tools at once
- Strong 9 CFM airflow provides rapid air delivery
- Automatic low-oil shutoff prevents pump damage
- Sturdy cast iron cylinders and frame construction
Cons
- Heavy unit weighing over 131 pounds
- Maximum pressure limited to 115 PSI
- Gas-powered design requires regular engine maintenance
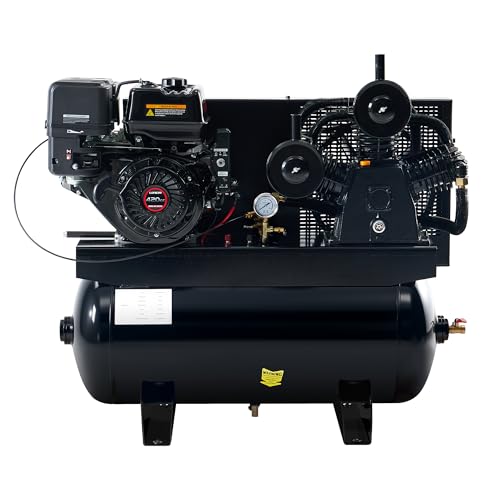
Albott 13HP Gas Air Compressor
The Albott 13HP Gas Air Compressor combines a 30-gallon ASME-certified tank with a 3-cylinder cast iron pump delivering 18 CFM at 90 PSI and up to 180 PSI maximum pressure. It is designed for service truck operators, mobile mechanics, and remote jobsite crews needing high-volume pneumatic airflow without electrical grid access.
Pros
- Delivers a listed 18 CFM at 90 PSI to easily operate high-demand pneumatic tools like heavy impact wrenches and spray guns off the grid
- Rugged 3-cylinder cast iron pump and frame reduce deformation and wear under demanding work conditions
- Substantial 30-gallon ASME-certified horizontal tank provides a reliable air buffer and reduces engine cycle frequency
- Total independence from 120V electrical outlets, eliminating blown household breakers and extension cord voltage drops
Cons
- Substantial dry weight of 344 pounds requires mechanical lifting equipment or permanent truck bed mounting rather than hand carrying
- Internal combustion engine produces exhaust fumes and high sound levels, restricting operation strictly to well-ventilated outdoor areas
- Requires dual routine maintenance schedules for both the gas engine and the oil-lubricated 3-cylinder compressor pump
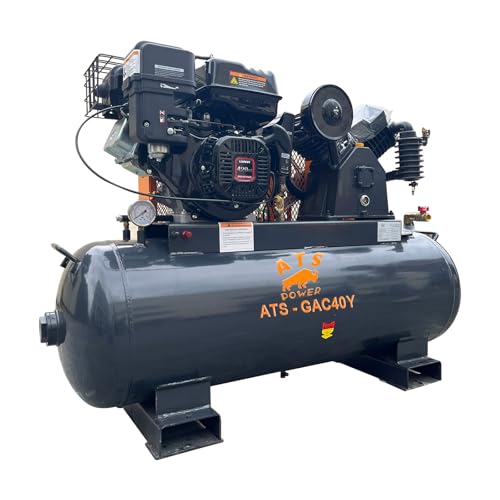
Generic 40-Gallon 15HP Gas Air Compressor
Built for demanding pneumatic tools like sandblasters and impact wrenches, this two-stage compressor pairs a 420cc RATO gas engine with a 40-gallon ASME tank. It delivers 24 CFM at up to 175 psi, providing reliable air delivery for off-grid job sites and busy workshops.
Pros
- High 24 CFM output powers demanding pneumatic tools
- Electric and recoil start provide flexible operation
- Durable ASME-certified steel pressure tank
- Oil-free pump minimizes routine maintenance tasks
- Integrated low-oil shutdown protects the engine
Cons
- Very heavy unit at 360 pounds
- Gas engine requires outdoor or well-ventilated placement
- Large footprint demands significant floor space
EVIL ENERGY 12V 1-Gallon Air Tank and Compressor
This compact 12V onboard air kit pairs a 1-gallon reinforced steel reservoir with an integrated compressor rated up to 150 PSI across five 1/4-inch NPT ports. It is well suited for truck owners, off-road enthusiasts, and DIY builders needing reliable air storage for suspension bags, air horns, and tire topping.
Pros
- Compact 1-gallon footprint fits easily into tight truck beds, trunk compartments, or undercarriage locations
- Five 1/4-inch NPT ports provide exceptional layout flexibility for custom air lines and accessories
- All-in-one kit includes compressor, tank, drain valve, air hose, and mounting brackets
- Solid steel tank construction with anti-corrosion exterior coating designed for mobile environments
Cons
- One-gallon capacity is strictly intended for intermittent air needs, not continuous-demand air tools like sanders or impact wrenches
- Airflow delivery ratings (SCFM) and decibel sound output are not explicitly specified by the manufacturer
- Requires custom 12V automotive wiring, dedicated fuse protection, and careful placement away from extreme road debris
Metabo HPT EC2510E 8-Gallon Air Compressor
Built for job sites without electrical hookups, this Metabo HPT compressor pairs a dependable Honda GX engine with an 8-gallon tank to power demanding framing and roofing nailers. Its cast iron pump and protective control panel suit rugged field use, though its 144-pound heft demands serious effort to haul.
Pros
- Reliable Honda GX gas engine
- Durable cast iron cylinder design
- Protective baseplate shields gauges and plumbing
- Delivers up to 145 PSI pressure
- Pre-installed 3/8-inch locking regulator
Cons
- Very heavy at 144 pounds to transport
- Gas engine requires outdoor ventilation and fuel upkeep
- Standard 1-year warranty is relatively short
Metabo HPT EC2610EA 9-Gallon Gas Compressor
Driven by a Honda GX200 engine, this 9-gallon wheelbarrow compressor supplies 9.5 CFM at 90 PSI to run multiple nailers at once. Its 160-pound frame is built for rugged jobsite mobility, though it demands routine engine and oil maintenance.
Pros
- High 9.5 CFM output supports multi-tool crews
- Reliable Honda GX200 engine for remote jobsites
- Flat-free solid rubber tire handles rough terrain
- Oil-lubricated pump and aftercooler extend service life
Cons
- Heavy 160-pound weight complicates solo truck loading
- Requires ongoing fuel and pump oil maintenance
- Limited to a standard one-year warranty
Engineering and Assembling a Gas-Powered Air Compressor System
Assembling a custom gas-powered pneumatic system gives mechanics, contractors, and fabricators an independent air supply tailored to severe field demands. Standard electric garage compressors cycle on and off using an electric pressure switch, but gasoline-powered units require a continuous-run mechanical architecture. Understanding component sizing, continuous-run pneumatics, and pulley ratios ensures your assembled unit delivers reliable airflow without damaging engine parts or creating safety hazards.
Core Mechanical Principles: Continuous-Run Systems vs. Electric Pressure Switches
Electric air compressors rely on a pressure switch that interrupts line voltage to stop the electric motor once tank pressure peaks. Gasoline engines cannot constantly stop and restart without burning out starter motors or draining starting batteries. Instead, a gas air compressor utilizes a continuous-run pilot unloader valve to manage compression cycles while the engine runs continuously. When tank pressure reaches the designated cut-out threshold, the pilot valve redirects high-pressure air to actuate an engine throttle control and open an unloader mechanism on the pump.
This unloader mechanism vents the compressor pump head so the pistons cycle freely without compressing air against tank resistance. At the same time, a pneumatic throttle control cable, commonly known as a bullwhip, pulls the engine governor arm to reduce engine speed to an idle. As pneumatic tools deplete tank air and system pressure drops to the cut-in threshold, the pilot valve vents its control line. This release allows the engine throttle to snap open, returning the engine to working speed to resume tank recharge.
Sizing Engines, Pumps, and Pulley Ratios for Reliable Air Delivery
Matching gasoline engine horsepower to pump air displacement is the most critical calculation when planning your build. Gasoline engines lack the high starting torque of industrial electric induction motors, requiring a higher horsepower rating to drive equivalent pump displacements. A reliable rule of thumb requires approximately one horsepower of gas engine displacement for every one to one-and-a-half CFM delivered at 90 PSI. For instance, commercial wheelbarrow units pair a 6.5 horsepower engine with a pump delivering 9 to 12 CFM, while large 40-gallon platforms pair a 15 horsepower engine with a two-stage pump to deliver 24 CFM.
Compressor pumps must operate within strict rotational speed limits, typically between 700 and 1,100 RPM for durable cast-iron reciprocating designs. In contrast, small four-stroke gasoline engines operate at governed speeds of approximately 3,000 to 3,600 RPM under load. Direct coupling would destroy pump valves and connecting rods within minutes. You must calculate the drive pulley diameter using the formula where engine pulley diameter equals the pump flywheel diameter multiplied by target pump RPM, divided by engine operating RPM.
Selecting cast-iron cylinder pumps and durable crankcases provides superior heat dissipation during extended field use. Single-stage pumps compress air directly into the receiver tank in a single stroke, generally topping out around 115 to 125 PSI. Two-stage pumps compress air in a primary low-pressure cylinder before pushing it through an intercooler into a high-pressure cylinder, efficiently generating up to 175 PSI. If you plan to power heavy-duty automotive impact wrenches, sandblasting setups, or multiple framing nailers, a two-stage pump ensures lower operating temperatures and higher compressed volume.
Tank Selection and Structural Mounting: Wheelbarrow vs. Skid Configurations
The receiver tank serves as both a mechanical mounting base and a pressure vessel for stored pneumatic energy. Fabricators must choose between mobile wheelbarrow frames and stationary utility skids based on their mobility requirements. Mobile contractor builds favor twin-tank wheelbarrow designs between 8 and 9 gallons, which keep the center of gravity low and incorporate flat-free tires for rough ground. Service truck and utility trailer installations typically employ 30-gallon horizontal ASME-certified tanks or larger 40-gallon platforms that provide substantial air reserves for continuous tool use.
Mounting a vibrating gas engine and a heavy reciprocating pump directly to a pressure vessel requires careful structural consideration. You should never drill, cut, or weld directly onto the pressure-bearing shell of a certified air tank. Doing so ruins the metallurgical temper, creates localized stress points, and risks catastrophic tank rupture under pressure. Instead, mount all mechanical components to the factory-welded deck plate or build a separate subframe that bolts securely to existing saddle mounts.
Installing dense neoprene or rubber vibration isolator bushings between the subframe and the tank deck reduces fatigue fractures in welded joints. High-frequency vibration from a single-cylinder gas engine can quickly loosen mounting bolts and crack rigid copper discharge lines if proper damping is absent. Ensure that grade-5 or grade-8 fasteners with nylon-locking nuts secure the engine and pump baseplates. Checking fastener torque after initial operational hours prevents alignment shifts that lead to thrown belts and damaged shafts.
Essential Pneumatic Plumbing: Pilot Unloaders, Check Valves, and Throttle Controls
The pneumatic control circuit forms the operational heart of any gas-powered compressor system. The primary air line exits the pump discharge port through heavy-duty copper or aluminum tubing equipped with cooling fins to dissipate compression heat. This discharge tube connects directly to an in-tank one-way check valve, which prevents pressurized tank air from backflowing into the pump cylinders when the engine idles. A continuous-run pilot unloader valve installs directly into a top tank port to monitor internal receiver pressure constantly.
When receiver pressure reaches the cut-out limit, the internal pilot valve disc lifts against spring pressure. This routes high-pressure air through a 1/4-inch nylon or copper pilot line to two separate destinations. First, it routes air to an external discharge unloader or pump head unloader pins, venting pump head pressure safely to the atmosphere. Second, it routes air to the engine throttle control cylinder mounted adjacent to the carburetor throttle arm.
The engine throttle control, or pneumatic bullwhip, contains an internal spring-loaded piston connected to a braided steel cable. When pressurized by the pilot valve, the piston extends and pulls the carburetor governor arm toward the idle stop screw, reducing engine speed to approximately 1,800 RPM. When tool use causes receiver pressure to drop to the cut-in threshold, the pilot valve closes and vents the pilot signal line. The spring-loaded bullwhip instantly retracts, allowing the engine governor to bring the engine back up to governed working RPM before the unloader closes.
Step-by-Step Mechanical Assembly and Drivetrain Alignment
Begin physical assembly by placing the air tank on a stable, level workbench and inspecting the mounting deck for flatness. Position the pump flywheel and engine drive shaft so they face the same direction with adequate clearance for pulley installation. Align the pump and engine parallel to each other, using a straightedge across the faces of both pulleys to verify that the belt grooves sit in the exact same plane. Angular or parallel pulley misalignment causes rapid belt wear, generates excessive bearing heat, and robs horsepower from the engine shaft.
Slide the chosen V-belt over the pulleys and adjust the engine position along the slotted deck holes to set tension. Proper belt tension should allow approximately 1/2 inch of deflection when pressed firmly with your thumb midway between pulleys. Tighten the engine mounting bolts in an alternating pattern to maintain alignment, rechecking pulley alignment with your straightedge after final torque is applied. Fit a rigid metal belt guard over the rotating assembly to protect hands, cables, and air lines from moving belts.
Connect the pump discharge port to the tank check valve using rigid copper tubing rated for high-temperature compression service. Include an expansion loop or flexible stainless steel braided discharge hose between the pump and tank to absorb engine vibration without fatiguing the fittings. Thread all pipe fittings using high-temperature anaerobic thread sealant rather than standard plumbing tape, which can shred and clog delicate pilot valve orifices. Hand-tighten all NPT fittings before applying a final turn-and-a-half with a wrench to ensure leak-free high-pressure seals.
Critical Safety Controls: ASME Relief Valves and Thermal Management
Operating a high-pressure mechanical system powered by an internal combustion engine demands redundant safety controls. The most critical component on any air tank is an ASME-certified safety relief valve. This spring-loaded brass valve must be rated for a relief pressure slightly above the cut-out threshold but below the maximum working pressure rating of the tank. If an unloader valve sticks or a pilot line kinks, the ASME valve automatically pops open to dump full pump volume, preventing catastrophic tank failure.
Thermal management is equally vital because air discharge temperatures from a working pump can easily exceed 300 degrees Fahrenheit. Position the compressor pump so the flywheel fan blades direct cooling air across the cylinder fins and aftercooler tubes. Never enclose a gas compressor in an unventilated vehicle compartment or cramped utility shed, as engine exhaust and radiating pump heat degrade lubricant and trigger engine vapor lock. Ensure that fuel lines remain safely routed away from hot cylinder heads and exhaust mufflers.
Incorporating an engine low-oil shutdown sensor protects the engine from destruction during rough jobsite operation. When operating a wheelbarrow compressor on sloped terrain or hauling a skid unit in a moving service truck, oil can slosh away from the splash dipper or pickup tube. Modern commercial engines feature low-oil switches that ground the ignition circuit if the oil level drops below a safe threshold. Always position the air intake filter away from the engine exhaust port to prevent the pump from drawing in carbon monoxide and soot.
Initial Break-In, Pilot Valve Calibration, and System Verification
Before filling the system with fuel, fill both the engine crankcase and the compressor pump with their specified lubricants. Gasoline engines require standard automotive four-stroke engine oil, while reciprocating compressor pumps require non-detergent ISO 68 or ISO 100 compressor oil. Detergent automotive oils should never be used in compressor pumps because detergents hold moisture and particulate in suspension, causing premature bearing wear and carbon build-up on reed valves. Check the pump oil sight glass or dipstick to confirm the level sits dead center before proceeding.
Conduct an initial unpressurized break-in cycle by opening the tank drain valve completely and starting the gasoline engine. Allow the engine to idle and drive the pump with zero tank backpressure for approximately twenty minutes. This zero-load run period allows piston rings to seat properly against the cylinder walls and circulates lubricant across bearings, wrist pins, and splash dippers. Listen for unusual knocking, inspect for oil leaks around gasket surfaces, and confirm that cooling air flows freely across the pump fins.
Close the drain valve and observe system behavior as pressure builds on the tank gauge. Watch the gauge carefully as the needle approaches the designated cut-out pressure, typically 115 to 145 PSI for single-stage setups or 175 PSI for two-stage units. When the cut-out pressure is reached, verify that the pilot valve clicks, the unloader vents head pressure with an audible hiss, and the engine drops smoothly to idle speed. Bleed air from the tank outlet to confirm that when pressure drops to the cut-in mark, the engine throttle snaps open and the pump resumes compressing without hesitation.
Operational Maintenance and Preventing Field Failures
Daily operational care is essential to protect your custom-built gas air compressor from premature internal rust and mechanical wear. As air compresses, ambient moisture condenses rapidly along the cooler inner walls of the steel receiver tank. Installing an accessible quarter-turn brass ball valve at the lowest point of the tank allows operators to purge accumulated water and sludge in seconds. Thumb-operated needle petcocks frequently seize, clog with scale, and discourage daily draining, leading to hidden internal corrosion and weakened tank walls over time.
Regularly inspect and clean the pump air intake filter, especially when operating on dusty construction sites, dirt access roads, or agricultural fields. A clogged intake filter restricts airflow, starves the cylinders, reduces delivered CFM, and pulls oil past the piston rings into the air stream. Check the drive belt tension monthly and inspect the belt surface for glazing, cracking, or edge fraying caused by minor pulley misalignment. Keep the engine spark plug clean and service the engine air filter according to the manufacturer schedule to maintain peak horsepower output.
Monitor pump oil clarity through the sight glass and perform regular oil changes after every 100 to 200 operating hours. Milky oil indicates excessive moisture condensation inside the crankcase, which typically occurs during brief run cycles in humid or cold environments. Operating the compressor long enough to reach full operating temperature evaporates crankcase moisture and keeps the splash lubrication system performing efficiently. Always depressurize the tank completely before servicing any fittings, tightening unloader lines, or checking valve components.
Building a custom gas air compressor delivers ultimate autonomy on remote jobsites where electrical utility power is non-existent. By carefully matching engine horsepower to pump displacement, engineering precise pulley ratios, and installing an uncompromising continuous-run pilot unloader circuit, you create a powerful, dependable workhorse. Prioritizing ASME-certified safety relief valves, robust structural isolation, and diligent daily moisture drainage ensures that your assembled pneumatic system operates safely and powers heavy-duty tools for years to come.
About the author
Tom Scalisi brings more than two decades of experience in construction, building maintenance, contracting, and hands-on tool use. His practical understanding of power tools, automotive work, repairs, and jobsite equipment helps readers evaluate compressors based on real workloads rather than specifications alone.