
How Do Rotary Screw Air Compressors Work: Complete Working Guide for 2026
Learn how do rotary screw air compressors work to provide continuous CFM and quiet industrial air delivery for commercial workshops in October 2026.
 By Tom Scalisi
Updated October 8, 2026

Continuous industrial applications like automotive paint booths, multi-bay impact wrench setups, and production CNC machinery demand high air volume that conventional reciprocating compressors struggle to sustain. Piston units generate severe heat and require regular resting intervals, but commercial operations need a steady stream of pressurized air without pressure drops. Understanding how do rotary screw air compressors work reveals why these machines operate smoothly at a 100% continuous duty cycle. Instead of pistons pumping up and down, these units rely on rotating helical components to compress air steadily and quietly.
Modern rotary screw units deliver reliable CFM output at 90 PSI while keeping operational noise around 65 to 68 decibels. Many commercial shops switch to rotary configurations when upgrading from loud cast-iron pumps because they want steady air pressure, lower energy costs, and minimal vibration. Whether you run an auto repair garage or an automated assembly shop, matching the right drive system and electrical configuration makes a huge difference in performance. This guide breaks down the core internal mechanics, lubrication loops, and control technologies that drive these industrial machines.
| Award | Product | ACR Score About ACR ScoreThe ACR Score is our own rating from 0 to 10, based on performance, design and build, ease of use, and value. It reflects independent research and is never influenced by manufacturers, retailers, or affiliate commissions. Learn more › | |
|---|---|---|---|
| Best Overall |
Compressed Air USA XL 8000-Hour Oil, 1 Gal
|
8.9/10 | Buy |
| Best Budget |
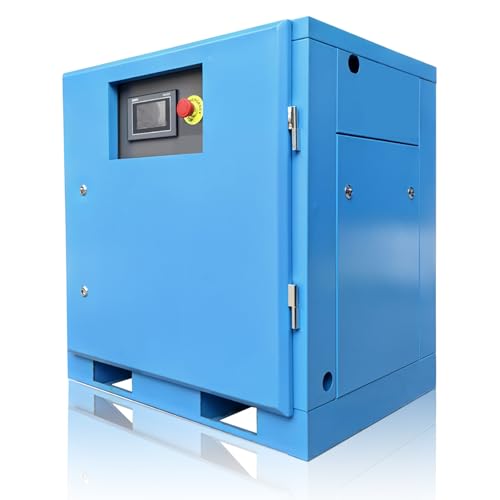 DCYL 10HP 230V Rotary Screw Compressor |
8.6/10 | Buy |
 MechMaxx M10AC230 10HP Rotary Screw Compressor |
8.6/10 | Buy | |
| Best Value |
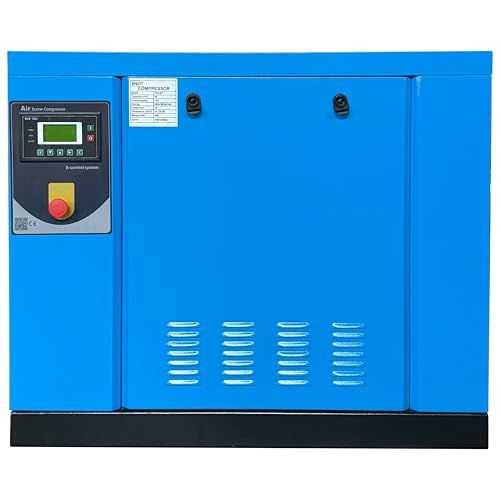 HPDAVV 10HP Rotary Screw Air Compressor |
8.6/10 | Buy |
| Best Premium |
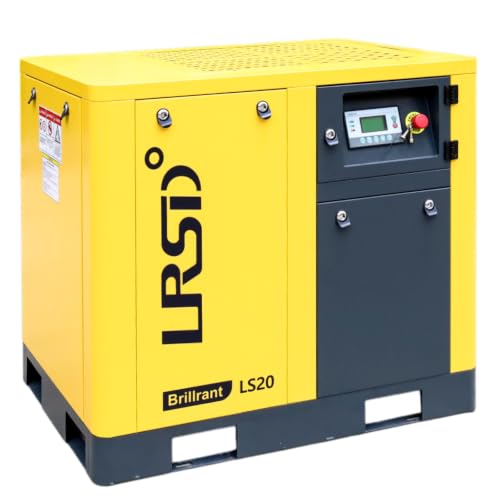 LRSD 20HP Rotary Screw Air Compressor |
8.3/10 | Buy |
 LRSD 7.5HP 80-Gallon Screw Air Compressor |
8.1/10 | Buy | |
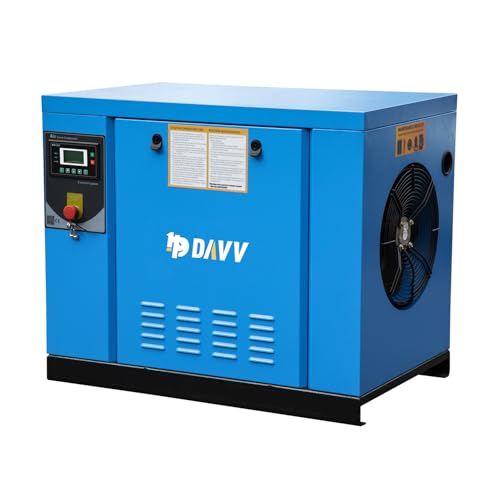 HPDAVV 10HP Rotary Screw Air Compressor |
7.8/10 | Buy | |
 LRSD 10HP Rotary Screw Air Compressor |
7.8/10 | Buy | |
 HPDAVV 10HP VSD Rotary Screw Compressor |
7.8/10 | Buy |
Compressed Air USA XL 8000-Hour Oil, 1 Gal
Formulated for rotary screw compressors, this synthetic blend delivers up to 8,000 hours of service life at elevated discharge temperatures. It mixes directly with existing OEM or aftermarket lubricants, eliminating the need for a full system drain before topping off.
Pros
- Long 8,000-hour service life under normal discharge heat
- No drain or flush required for system top-offs
- Broad compatibility with OEM and aftermarket equivalents
- Protects against wear, varnish, and moisture buildup
- Non-toxic and non-hazardous formulation
Cons
- Synthetic blend rather than a pure synthetic base
- Designed specifically for rotary screw air compressors
- One-gallon container may require multiple bottles for large units
DCYL 10HP 230V Rotary Screw Compressor
Built for dedicated workshops needing steady airflow, this single-phase rotary screw unit delivers 39 CFM at up to 120 PSI. Its variable-speed motor automatically adjusts output to air demand, cutting down on power consumption and noise.
Pros
- High 39 CFM airflow on single-phase 230V power
- Variable speed operation conserves energy during low demand
- Pre-commissioned setup simplifies initial installation
- Soft start provides lower noise and smooth operation
Cons
- Cannot convert between single-phase and three-phase power
- Housing color ships randomly unless requested from seller
- Requires dedicated 208-230V high-amperage electrical service
MechMaxx M10AC230 10HP Rotary Screw Compressor
Designed for continuous industrial demand, this stationary rotary screw compressor delivers 32 CFM at 116 PSI with an automated EPC control system that regulates power according to real-time air consumption. It serves workshops and manufacturing facilities equipped with three-phase power that require clean, high-volume compressed air.
Pros
- High 32 CFM output for continuous industrial use
- Clean air discharge with under 3 ppm oil carryover
- Automatic idle shutdown minimizes operational power waste
- IP54-rated enclosed motor with heavy-duty SKF bearings
- Built-in diagnostic system for rapid fault detection
Cons
- Requires a dedicated 230V three-phase electrical connection
- Maximum operating pressure is capped at 116 PSI
- Stationary footprint requires permanent workshop installation
HPDAVV 10HP Rotary Screw Air Compressor
Built for small to midsize industrial facilities, this rotary screw unit delivers 33 CFM at up to 125 PSI via a continuous-duty three-phase motor. An integrated spin-on separator and air-cooled aftercooler help keep discharge temperatures down while simplifying routine maintenance.
Pros
- High 33 CFM output handles demanding industrial equipment
- Spin-on separator makes routine filter maintenance simple
- Air-cooled aftercooler helps manage operating temperatures
- Internal oil return system reduces air line oil carryover
Cons
- Requires a dedicated three-phase 230V electrical supply
- Cannot run on single-phase power with phase converters
- Heavy 600-pound footprint requires dedicated installation equipment
LRSD 20HP Rotary Screw Air Compressor
Engineered for high-demand workshops, this 20HP rotary screw unit delivers 75 CFM of continuous airflow at up to 145 PSI. An enclosed cabinet suppresses operational noise to roughly 68 dB while preserving valuable floor space.
Pros
- Continuous 75 CFM airflow suited for heavy-duty machinery
- Quiet 68 dB cabinet design minimizes shop noise
- Compact footprint saves industrial floor space
- Adjustable operating pressure between 100 and 145 PSI
Cons
- Requires dedicated 230V three-phase electrical service
- Heavy 595-pound frame requires machinery to position
LRSD 7.5HP 80-Gallon Screw Air Compressor
Engineered for demanding fabrication and auto shops, this stationary rotary screw compressor combines an 80-gallon tank, dryer, and filtration system into a single plug-and-play assembly. Its IP55 sealed motor generates 29 CFM of continuous airflow while resisting airborne dust and moisture.
Pros
- All-in-one design combines compressor, tank, and dryer
- Delivers high 29 CFM output for continuous work
- Sealed IP55 motor endures dusty industrial environments
- Service factor of 1.15 tolerates short motor surges
- Large 80-gallon receiver ensures steady air volume
Cons
- Requires three-phase 230V commercial power hookup
- Large stationary footprint requires permanent shop floor space
- Substantial size makes moving difficult after placement
HPDAVV 10HP Rotary Screw Air Compressor
Built for heavy industrial operations, this 10-horsepower rotary screw compressor delivers dependable 125 PSI output with an integrated spin-on separator for reduced downtime. It requires a dedicated 460V three-phase power supply, making it an ideal fit for manufacturing plants, automotive shops, and commercial production facilities.
Pros
- Spin-on separator allows quick and clean maintenance
- Hinged service covers provide instant access to consumables
- Efficient microprocessor controller manages compressor operations
- Steady 33 CFM air output suited for industrial tools
Cons
- Requires high-voltage 460V to 480V three-phase electrical input
- Incompatible with single-phase power converters
LRSD 10HP Rotary Screw Air Compressor
Built for continuous industrial applications like auto repair and woodworking, this unit delivers high airflow through a direct-drive 10HP motor. It produces exceptionally clean air with minimal oil carry-over, though it strictly demands a dedicated three-phase power supply.
Pros
- High 37 CFM output handles heavy pneumatic equipment
- Direct-drive motor eliminates belt slippage and wear
- Low oil carry-over extends pneumatic tool life
- Engineered for continuous industrial duty cycles
Cons
- Requires 230V 3-phase power with no single-phase conversion
- Heavy 397-pound footprint requires dedicated stationary installation
HPDAVV 10HP VSD Rotary Screw Compressor
Engineered for busy auto body shops and industrial facilities, this all-in-one system combines a 10-horsepower variable speed compressor, storage tank, and refrigerated air dryer into a single base. Its compatibility with both single-phase and three-phase 230V lines delivers continuous 39 CFM output without requiring a three-phase utility connection.
Pros
- Integrated dryer delivers clean, moisture-free compressed air
- Compatible with standard single-phase or three-phase 230V power
- Continuous-duty rating supports non-stop industrial workflows
- Variable speed technology lowers overall operating power draw
Cons
- Substantial 800-pound weight requires heavy machinery for unloading
- Large footprint requires dedicated floor space in the workspace
Inside the Mechanics and Engineering of Rotary Screw Compression
Rotary screw compression relies on positive displacement to generate smooth, continuous pneumatic power without the pulsating cycles of piston pumps. Exploring how do rotary screw air compressors work begins inside the compression chamber, where mechanical precision replaces reciprocating strokes. Understanding these core internal processes helps operators optimize air quality and system efficiency.
The Core Compression Cycle and Helical Rotor Geometry
At the heart of every screw compressor sits an airend containing two precision-machined helical rotors. One rotor features convex lobes designated as the male rotor, while the mating female rotor contains concave flutes. As an electric motor drives these interlocking rotors, ambient air enters through the intake regulator valve into the expanding spaces between the lobes. The turning action sweeps the air along the length of the housing, trapping the air volume within the meshing profiles.
As rotation continues, the physical space between the rotor lobes progressively decreases toward the discharge end. This continuous reduction in volume forces the trapped air into a smaller area, steadily elevating its pressure before it reaches the discharge port. Because this displacement occurs without intake or exhaust valves opening and closing, air flows in a constant, pulsation-free stream. The precision engineering keeps rotor clearances within microns, preventing air leakage back toward the inlet while avoiding direct metal-to-metal contact between the lobes.
The Critical Functions of Injected Compressor Lubricant
Most industrial units use oil-injected screw designs where specialized synthetic fluid plays three vital roles during the compression cycle. First, the lubricant injects directly into the airend to seal the microscopic gaps between the spinning male and female rotors. This dynamic liquid seal prevents compressed air from slipping backward, which keeps volumetric efficiency high. Second, the oil lubricates the heavy-duty roller bearings supporting the rotor shafts under extreme rotational and thrust forces.
Third, the circulating lubricant absorbs the intense thermal energy generated as air compresses. Reciprocating compressors often run scorching discharge temperatures because air heating remains localized in the cylinder heads. In a screw pump, injected oil immediately absorbs this heat, keeping internal discharge temperatures stable around 170 to 200 degrees Fahrenheit. Maintaining this fluid requires high-grade synthetic blends, such as 8000-hour extended life oils, which resist varnish formation, water breakdown, and thermal oxidation under heavy operational stress.
Oil Separation and Scavenging Mechanics
Because oil mixes intimately with atmospheric air inside the airend, the discharged mixture must undergo thorough separation before entering shop air lines. The hot air-and-oil stream discharges directly into an internal separator receiver tank. Centrifugal force and directional baffles cause roughly 90 percent of the heavy liquid oil droplets to drop out of suspension and settle at the tank floor. The remaining aerosol mist moves upward through a dedicated micro-glass coalescing filter element.
Modern spin-on air-oil separators trap tiny oil droplets on their synthetic fibers, allowing them to coalesce into larger drops that pool at the base of the filter. A narrow scavenge line equipped with a sight glass and one-way check valve draws this captured oil back into the low-pressure suction side of the pump. Advanced designs keep oil carry-over at or below 3 parts per million, ensuring that downstream air remains remarkably clean for sensitive applications like auto body paint sprayers and precision pneumatic tools.
Air Regulation: Fixed-Speed Modulation vs. Variable Speed Drive
Controlling output volume determines how efficiently a rotary compressor matches your workshop air demand. Traditional fixed-speed machines run their electric motors at a constant rotational speed, typically around 3600 RPM. When line pressure reaches the upper setpoint, an electronic control system unloads the inlet valve, allowing the motor to idle with minimal air intake. While this load and unload cycling prevents frequent motor restarts, running the machine unloaded still draws substantial electrical power without producing useful compressed air.
Variable Speed Drive systems solve this idle waste by using an internal frequency inverter to adjust motor speed in real time based on actual CFM consumption. If a workshop operates just one orbital sander, the controller slows the motor down to produce only the required air flow. When multiple technicians trigger paint guns or impact wrenches simultaneously, the drive accelerates immediately to deliver peak CFM output. This active modulation eliminates hard electrical inrush surges during starts, maintains rock-solid system pressure within 1 to 2 PSI, and cuts energy waste during fluctuating workloads.
Thermal Control, Aftercoolers, and Moisture Removal
Temperature regulation is essential to prevent internal moisture condensation and extend compressor longevity. A thermostatic mixing valve controls oil flow through an air-cooled radiator core. When the machine starts cold, the valve bypasses the cooler so the oil warms rapidly above the water condensation threshold, preventing moisture from pooling in the lubricant. Once the system reaches normal operating temperature, the valve diverts the oil through the cooler to shed excess heat.
The compressed air stream also passes through an integrated air-cooled aftercooler before discharging into workshop piping. Cooling the discharge air drops its temperature close to ambient levels, which forces suspended water vapor to condense into liquid droplets. An internal moisture separator then expels this condensate through an automatic drain valve. This initial cooling stage protects downstream lines and prepares the air for refrigerated air dryers that lower the pressure dew point further.
All-in-One Integrated Systems vs. Modular Base-Mounted Packages
Commercial buyers often choose between compact all-in-one stations and traditional modular setups. Standalone base-mounted screw compressors supply pressurized air but require external receiver tanks, freestanding dryers, and separate filter banks plumbed together across the shop floor. This approach works well in large facilities with existing air treatment equipment, but it requires significant floor space and extensive copper or aluminum manifold piping.
All-in-one configurations mount the rotary screw pump, an ASME-certified receiver tank, multi-stage coalescing filters, and a refrigerated air dryer on a single unified chassis. Models featuring 80-gallon storage tanks combine clean air production with ample reserve volume in a remarkably small footprint. These pre-commissioned systems simplify installation because shop owners only need to connect one main electrical line and one discharge air header. Having the filtration, moisture separation, and drying equipment factory-matched also ensures balanced airflow without unexpected pressure drops across mismatched components.
Electrical Demands: Single-Phase Convenience vs. Three-Phase Industrial Power
Power supply requirements represent a major factor when installing rotary screw equipment. Most commercial units producing 10 horsepower or more operate on 230-volt or 460-volt three-phase alternating current. Three-phase power delivers smooth rotational torque, superior motor efficiency, and lower running amperage, making it the industrial standard for manufacturing plants and large automotive facilities. However, bringing three-phase utility lines into a standard commercial or residential building often requires expensive utility upgrades.
For smaller independent shops and home restoration garages, manufacturers produce specialized 10-horsepower units designed for 208-230-volt single-phase power. Single-phase screw compressors allow operators to achieve high air delivery, such as 39 CFM at 120 PSI, without utility rewiring. It is critical to recognize that you cannot convert a three-phase compressor to single-phase operation using simple static converters. Buyers must confirm their building panel capacity and select a machine built specifically for their available electrical phase to prevent costly electrical installation failures.
100% Continuous Duty Cycle vs. Reciprocating Piston Limitations
The defining operational advantage of rotary screw technology is its 100% continuous duty rating. Traditional reciprocating piston compressors generate intense frictional heat in their cylinders, requiring a 50% to 70% duty cycle to let the pump cool down between cycles. If a busy automotive body shop runs continuous sanders on a piston pump, the machine can overheat and fail prematurely.
Rotary screw machines operate under steady internal oil cooling, meaning they are designed to run continuously throughout an eight-hour shift without stopping. In fact, screw compressors prefer steady operation because running continuously keeps oil temperatures high enough to boil off atmospheric moisture. Short, infrequent cycles can actually cause condensation to accumulate inside the oil circuit, degrading fluid quality. When your shop workflows require non-stop CFM delivery for plasma cutters, automated assembly lines, or continuous spray finishing, rotary technology provides the stamina reciprocating pumps cannot match.
Essential Preventative Maintenance and Service Intervals
Maintaining a rotary screw compressor requires a structured maintenance routine rather than reactive repairs. Inspecting the oil sight glass before every shift ensures the lubricant reservoir maintains adequate fluid levels. Depending on your working environment and oil formulation, full synthetic compressor fluid typically requires replacement every 4,000 to 8,000 operating hours. Using non-detergent synthetic oils formulated specifically for rotary screws protects internal tolerances and prevents foaming inside the separator tank.
Routine servicing also involves replacing the spin-on air-oil separator and oil filter at regular yearly intervals. The intake air filter element must be inspected weekly in dusty environments like woodworking shops or metal fabrication bays, as restricted intake filters reduce delivered CFM and strain the electric motor. Technicians should also verify automatic drain valve operation and test pressure relief valves to maintain complete workshop safety. Keeping detailed service records and changing consumables on schedule allows modern rotary screw compressors to run reliably for tens of thousands of operating hours.
Understanding the mechanical cycle of twin interlocking screws, dynamic oil cooling, and multi-stage separation clarifies why commercial shops invest in rotary power. When sized properly for your electrical service and paired with appropriate air drying, a rotary screw compressor delivers whisper-quiet, continuous pneumatic output. This continuous reliability keeps high-demand tools running smoothly without unexpected pressure drops.
About the author
Tom Scalisi brings more than two decades of experience in construction, building maintenance, contracting, and hands-on tool use. His practical understanding of power tools, automotive work, repairs, and jobsite equipment helps readers evaluate compressors based on real workloads rather than specifications alone.