
How Air Compressor Works: A Practical Guide for 2026
Explore %how air compressor works% in October 2026. Review air compression mechanics, pressure switches, regulators, and storage tank performance.
 By Glenda Taylor
Updated October 8, 2026

Pneumatic tools derive their driving power from ambient air packed tightly into a rigid steel vessel under mechanical force. When considering %how air compressor works%, the entire mechanism centers on converting electrical or chemical energy into kinetic energy stored as potential air pressure. An electric motor or cordless battery pack spins an internal crankshaft, driving a reciprocating piston that forces atmospheric volume into a sealed chamber. This continuous stroke builds substantial internal kinetic energy, ready to discharge through pneumatic hoses whenever a nailer, spray gun, or impact tool triggers a release.
Operating a pneumatic system requires balancing generated volume, measured as CFM at 90 PSI, against total storage capacity and maximum operational pressure. Modern workshops depend on automated safety assemblies like pressure switches, check valves, and unloader ports to manage continuous cycling without overloading electric motors or rupturing lines. Understanding the interplay between air intake, compression chambers, and downstream regulators ensures that your equipment delivers smooth, reliable output while preventing internal component fatigue.
| Award | Product | ACR Score About ACR ScoreThe ACR Score is our own rating from 0 to 10, based on performance, design and build, ease of use, and value. It reflects independent research and is never influenced by manufacturers, retailers, or affiliate commissions. Learn more › | |
|---|---|---|---|
| Best Overall |
Cordless Air Compressor Compatible with Dewalt 20V
|
9.2/10 | Buy |
| Best Value |
 Metabo HPT 6-Gallon Pancake Air Compressor Review |
8.6/10 | Buy |
| Best Budget |
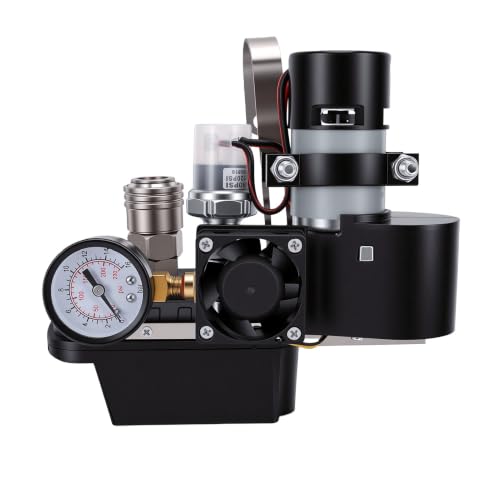 banapoy Portable Cordless Nail Gun Air Compressor |
8.4/10 | Buy |
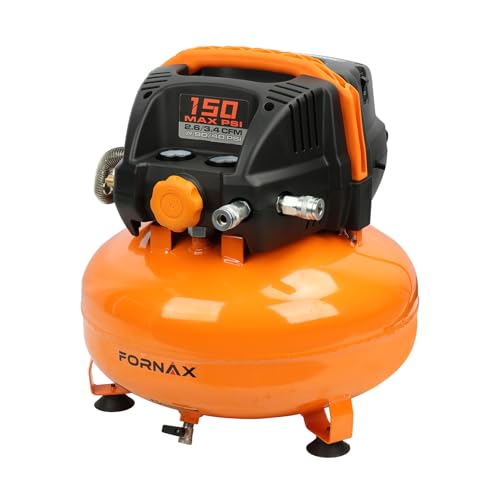 FORNAX 6-Gallon Pancake Air Compressor |
8.4/10 | Buy | |
| Best Premium |
 DEWALT DWFP55130 2.5-Gallon 200 PSI Quiet Trim Air |
8.4/10 | Buy |
 Metabo HPT EC914S 6-Gallon 200 PSI Pancake Air |
8.3/10 | Buy | |
 Cordless Air Compressor for DEWALT 20V MAX Battery |
8.3/10 | Buy | |
 Ultra Quiet Air Compressor, Only 68dB |
7.8/10 | Buy |
Metabo HPT 6-Gallon Pancake Air Compressor Review
The Metabo HPT EC711S is a portable 6-gallon pancake air compressor delivering 2.8 CFM at 90 PSI with a 165 PSI tank ceiling and an operating sound level of 73 dB. With its quick 46-second recovery cycle and dual quick couplers, it is an excellent choice for finish carpenters, punch-list contractors, and DIYers running pneumatic nailers.
Pros
- 73 dB operational sound rating is substantially quieter than standard job-site pancake units
- 165 PSI maximum pressure provides ample air storage with a swift 46-second recovery cycle
- Two 1/4-inch universal quick couplers support multi-tool setups right out of the box
- Sturdy steel roll cage protects gauges and the manifold assembly against knocks and drops
- Oil-free 1.0 HP motor ensures low maintenance and reliable cold-weather motor startup
Cons
- At 38.5 lbs, it is slightly heavier than ultra-compact 1-to-3-gallon trim compressors
- Airflow of 2.8 CFM at 90 PSI is designed for intermittent fastening, not continuous rotary tools or paint sprayers
- Bare-tool configuration means air hoses and pneumatic fastening tools must be purchased separately
FORNAX 6-Gallon Pancake Air Compressor
The FORNAX 6-Gallon Pancake Air Compressor delivers 2.6 CFM at 90 PSI and up to 150 PSI of maximum pressure, featuring dual couplers and a lightweight 28.8-pound portable footprint. It is a practical pneumatic power source for DIY homeowners, finish carpenters, and garage hobbyists driving nailers or managing tire inflation.
Pros
- Dual quick-connect couplers allow two nailers to operate simultaneously without adding an external splitter manifold
- Generous 6-gallon air tank capacity with a 150 PSI maximum pressure ceiling provides a dependable air reserve
- Lightweight 28.8-pound profile simplifies one-handed carrying up stairs and transport into work vans
- Maintenance-free oil-free pump eliminates oil checks, oil changes, and mess around finished work surfaces
Cons
- Operating sound output rated at 95 dBA is loud and makes hearing protection necessary, especially in closed rooms
- Airflow output of 2.6 CFM at 90 PSI cannot support continuous-demand tools like sanders, grinders, or paint sprayers
- Supplied as a bare-tool compressor without an included air hose, tire inflator chuck, or pneumatic nailers
DEWALT DWFP55130 2.5-Gallon 200 PSI Quiet Trim Air
The DEWALT DWFP55130 delivers a capable 3.0 SCFM at 90 PSI with a 200 max PSI 2.5-gallon tank, running at a quiet 71.5 dBA on an efficient 12-amp motor. It is an ideal pneumatic power source for trim carpenters, punch-list contractors, and DIYers working on residential circuits.
Pros
- Delivers 3.0 SCFM at 90 PSI with a high 200 max PSI ceiling for rapid pressure recovery during sequential fastening
- Quiet 71.5 dBA sound output makes indoor trim carpentry and remodeling far less disruptive to homeowners
- Low 12-amp draw reduces breaker trips when running on shared 15-amp household circuits
- Integrated roll cage and console protect critical components while supporting horizontal or vertical operation
- Dual quick couplers allow two trim carpenters to connect and work off a single compressor
Cons
- Bare-tool configuration means you must supply your own air hoses, couplers, and pneumatic nail guns
- At 36 pounds, it is heavier to haul up flights of stairs than ultra-compact 1-gallon finish compressors
- Air output of 3.0 SCFM is built for intermittent finish fastening and will not support continuous tools like rotary sanders or sprayers
Metabo HPT EC914S 6-Gallon 200 PSI Pancake Air
The Metabo HPT EC914S delivers an impressive 200 PSI maximum pressure and 4 CFM at 90 PSI from a 6-gallon tank, giving trim carpenters and remodelers the air volume needed to drive multiple nailers simultaneously. At roughly 41 pounds, it successfully combines high-pressure air storage with practical job-site portability.
Pros
- High 200 PSI tank ceiling stores substantially more usable air than conventional 150 PSI pancake models
- Generous 4 CFM at 90 PSI airflow rating supports multi-tool operation and reduces nailer drive hesitation
- Manageable 41-pound carry weight offers better portability than heavier twin-stack compressor configurations
- Engineered by Metabo HPT to support both lightweight trim nailers and larger framing or roofing guns
Cons
- At 41 pounds, it is noticeably heavier to carry than minimalist 1-to-3 gallon trim-only compressors
- Tank volume and CFM output remain inadequate for continuous high-demand air tools like HVLP sprayers or sanders
- Ships as a bare-tool compressor without included air hoses, pneumatic fittings, or nail guns
The Mechanics Behind Pneumatic Power Generation
Every pneumatic air compressor functions by capturing ambient atmospheric air, reducing its volume mechanically, and holding that pressurized gas inside a heavy-gauge storage tank until needed. Grasping %how air compressor works% requires looking past the outer housing into the synchronized interplay of electric motors, intake valving, check valves, and automated control switches. When this closed pneumatic cycle functions properly, it delivers instantaneous kinetic force capable of cycling framing nailers or powering continuous garage air tools. Without these precisely sequenced components working together, pressurized storage would quickly collapse into thermal overload or catastrophic line leakage.
The Physics of Atmospheric Air Compression
At sea level, normal atmospheric air rests at roughly 14.7 pounds per square inch of absolute ambient pressure. When an air compressor activates, it ingests this atmospheric gas and forces the molecules into a substantially smaller physical space. Boyle’s law describes this physical behavior by establishing that gas pressure increases proportionally as vessel volume decreases under constant temperature. Compressing air molecules together also produces significant friction and thermal energy, creating intense heat within the pump cylinder during every mechanical stroke.
Cooling the compressed air becomes an essential engineering priority because hot air holds moisture and expands beyond its stable volume. As the pump forces pressurized molecules into the storage tank, the air gradually cools, which leads to a slight reduction in localized pressure and causes suspended water vapor to condense. Understanding this fundamental thermodynamic cycle explains why air compressors generate heat during continuous running cycles. It also clarifies why effective heat dissipation fins and cooling fans remain essential components on modern electric pump housings.
The Reciprocating Piston Cycle and Reed Valve Operation
Most portable jobsite units and garage workshop compressors rely on a reciprocating piston assembly driven by an electric motor or brushless drive. As the motor spins the crankshaft, the connecting rod pulls the piston downward inside the cylinder bore during the intake stroke. This downward motion creates an internal partial vacuum above the piston crown, causing the flexible intake reed valve to flex open. Atmospheric air passes through an intake air filter to strip out airborne dust before rushing into the expanding cylinder volume.
Once the piston reaches bottom dead center, the crankshaft pushes it upward into the compression stroke. The sudden increase in internal cylinder pressure immediately forces the intake reed valve shut against its seat, preventing air from escaping back out the intake port. As the rising piston compresses the trapped air toward the top of the cylinder, the localized pressure exceeds the resistance of the exhaust valve spring or flapper. The exhaust valve snaps open, allowing the high-pressure air pulse to rush through the discharge tube directly toward the receiver tank.
The Storage Vessel and One-Way Check Valve Mechanics
Pumping air directly into an open tool line without a receiver tank would produce erratic pressure pulsations with every stroke of the piston. A steel or aluminum storage tank serves as an essential pneumatic buffer, smoothing out these pressure spikes into a steady reservoir of stored potential energy. Tank capacities range widely across the industry, from compact 0.26-gallon portable cylinders to popular 6-gallon pancake designs and large stationary workshop vessels. This stored reserve enables users to operate intermittent pneumatic tools without forcing the electric motor to run constantly.
A critical one-way tank check valve sits at the entrance port where the hot discharge tube enters the storage tank. This brass or bronze fitting contains an internal spring-loaded rubber seal or Teflon disc that allows air to enter during the compression stroke. Once the compressor motor shuts down, the dense air inside the tank pushes firmly against the opposite side of the check valve seal. This mechanical seal blocks stored air from back-feeding into the pump cylinder, preserving full tank pressure and isolating the pump assembly from backpressure.
Pressure Switch Operation: Managing Cut-In and Cut-Out Thresholds
An automated electromechanical pressure switch acts as the command center for the entire air compression cycle. This device monitors internal tank pressure through a sensitive lower diaphragm connected directly to the receiver vessel. As the pump forces air into the tank, the rising internal pressure pushes against an internal diaphragm spring. When the pressure reaches the factory-calibrated maximum setting, known as the cut-out threshold, the internal contact points snap open and instantly cut electrical power to the drive motor.
Cut-out pressure thresholds vary across machine designs, typically reaching between 115 PSI on light utility units and 200 PSI on high-pressure jobsite compressors. As you use air tools, the stored tank pressure steadily drops until it hits the pre-calibrated cut-in threshold. At this lower point, the diaphragm spring overcomes the remaining air pressure, snapping the electrical contacts back together. The motor restarts automatically, running the pump until the tank returns to its upper cut-out limit without requiring any manual switch operation from the user.
Unloader Valve Function and Motor Startup Protection
Electric motors encounter immense resistance if forced to start turning while trapped high-pressure air sits directly atop the piston head. To prevent this mechanical lockup, compressors utilize an unloader valve linked directly to the pressure switch assembly. The exact moment the pressure switch reaches cut-out and shuts off the motor, a mechanical actuator pin depresses the unloader valve stem. This action releases all trapped air trapped inside the cylinder head and discharge tube through a small exhaust vent, producing a brief hiss.
Venting this small volume of residual head pressure leaves atmospheric pressure above the piston during the stationary phase. When the pressure switch later calls for the motor to restart at the cut-in threshold, the piston begins moving against zero head resistance. This brief zero-load window allows the motor to spin up to operating RPM before encountering high compression forces. Without a functioning unloader valve, the motor would experience severe inrush current spikes, frequently tripping standard 15-amp household circuit breakers.
Air Pressure Regulation and Downstream CFM Delivery
Air stored inside a tank at 150 to 200 PSI is generally at too high a pressure for direct tool operation. Most pneumatic nailers, paint sprayers, and impact wrenches require a controlled working pressure between 70 and 110 PSI to prevent internal seal damage. A line pressure regulator installed on the outlet manifold allows operators to dial down tank pressure to the specific requirement of the connected tool. Dual pressure gauges provide visual confirmation, displaying the raw internal tank reserve on one dial and the regulated working line pressure on the other.
While pressure, measured in PSI, determines the force behind a tool stroke, air volume, measured in cubic feet per minute (CFM), dictates sustained runtime. Pneumatic nailers require tiny bursts of CFM, enabling small pancake compressors to keep pace with rapid fastening work. Conversely, continuous-draw tools such as dual-action sanders or HVLP paint sprayers consume high volumes of air constantly. If a tool consumes more CFM at 90 PSI than the pump generates, tank pressure will steadily drop until the tool stalls, regardless of how high the maximum storage PSI is rated.
Oil-Free Dual-Piston Systems Versus Splash-Lubricated Pumps
Piston lubrication represents one of the most significant design differences among modern air compressor pumps. Traditional workshop compressors employ an oil-lubricated cast-iron pump where an oil dipper on the connecting rod splashes lubricant across cylinder walls and bearings. This oil bath provides exceptional heat dissipation and reduces friction, allowing cast-iron pumps to achieve long commercial operating lifespans. However, oil-lubricated compressors require regular fluid level checks, scheduled oil changes, and level operating surfaces to prevent catastrophic pump seizure.
Modern portable compressors and ultra-quiet garage units increasingly utilize oil-free dual-piston pump architectures. Instead of liquid lubricant, these systems feature heat-resistant Teflon-impregnated or composite piston rings that slide smoothly within precision aluminum or steel sleeves. Many quiet units operate twin opposing pistons running at reduced motor speeds, generating steady airflow while holding operational sound levels down near 65 to 68 dB. The absence of lubricating oil prevents downstream line contamination, making oil-free designs highly desirable for indoor trim carpentry, spray finishing, and clean workshop environments.
Thermal Dynamics, Moisture Accumulation, and Tank Drainage
Condensation is an unavoidable byproduct of how an air compressor draws moisture from atmospheric air during normal compression cycles. Ambient air always carries water vapor, and when the pump squeezes that air into a fraction of its original volume, the dew point rises significantly. As the hot compressed air enters the cooler steel storage vessel, water droplets condense rapidly along the inner walls and pool at the bottom. Over time, standing water inside an unmaintained steel vessel creates corrosive rust, weakening structural tank seams and contaminating downstream tools.
Purging this accumulated liquid is an essential maintenance task that every compressor operator must perform regularly. Tanks feature a bottom drain valve, either configured as a threaded needle petcock or an accessible quarter-turn brass ball valve. Opening this valve under partial tank pressure forces stagnant water and sediment out through the discharge port. Proper moisture management keeps internal steel surfaces dry and protects pneumatic nailer o-rings from water damage. It also prevents water droplets from spraying through air lines during delicate spray painting or finish woodworking tasks.
Single-Stage Versus Two-Stage Compression Principles
The vast majority of consumer and portable jobsite compressors utilize single-stage compression mechanisms. In a single-stage pump, each stroke of the piston draws ambient air into the cylinder and compresses it directly to final tank pressure in one motion. Single-stage configurations are compact, cost-effective, and capable of generating pressures ranging from 115 to 200 PSI depending on motor strength and valve geometry. They easily handle light-duty to medium-duty tasks, including finish carpentry, automotive tire maintenance, and occasional pneumatic fastening.
Heavy-duty commercial workshops and industrial facilities often rely on two-stage air compressors to handle continuous pneumatic workloads. In a two-stage pump, a large low-pressure piston first compresses atmospheric air to an intermediate pressure level. That air passes through an exterior finned intercooler tube to shed heat before entering a smaller high-pressure cylinder for secondary compression. Staging the workload across two separate cylinders reduces thermal stress, increases volumetric efficiency, and allows machines to achieve stable operating pressures reaching 175 PSI for demanding industrial tools.
Modern Power Architectures: Cordless Lithium Drive Versus Line Voltage
Traditional electric air compressors require connection to standard 120V household outlets or dedicated 240V circuits to drive induction or universal motors. Universal motors spin at high RPM to deliver fast pump recovery, though they produce elevated decibel levels and draw significant starting amperage. Induction motors run at lower speeds, generating less operating noise and lasting longer in stationary applications, but they carry substantial weight. Managing electrical supply requirements carefully prevents motor stalling and eliminates nuisance breaker tripping when operating heavy tools on jobsite extension cords.
Recent developments in lithium-ion battery technology have introduced cordless air compressor platforms that operate on 20V power tool batteries. These compact machines utilize efficient brushless motors to drive mini oil-free pumps, eliminating extension cords entirely for mobile punch-list work and trim carpentry. While cordless units feature modest tank volumes from 0.26 to 1 gallon, they deliver sufficient pressure to actuate brad nailers and inflate tires on remote sites. Choosing between cordless mobility and corded line-voltage continuous runtime depends largely on the airflow requirements of your chosen pneumatic applications.
Operational Verification and Diagnostic System Health
Verifying proper compressor operation involves observing cycle timing and listening for subtle mechanical cues during pressurized operation. A healthy air compressor should build pressure smoothly from zero to cut-out without motor hesitation or erratic RPM fluctuations. When the motor shuts off, the unloader valve should emit a crisp, brief air blast, followed by absolute silence from the pump head. Any continuous hissing from the unloader port after shutdown indicates a leaking tank check valve that requires cleaning or replacement.
Routine safety checks should also include manually testing the ASME-certified safety relief valve ring to ensure the internal spring moves freely. Inspecting intake air filters for dirt accumulation prevents pump restriction, ensuring the compression chamber receives full atmospheric volume on every downward stroke. Verifying that the pressure regulator turns smoothly and holds steady working line pressure protects connected tools from pressure surges. By understanding each step in the mechanical chain, operators can easily diagnose minor leaks, optimize performance, and keep their pneumatic systems operating safely for years to come.
About the author
Glenda Taylor has extensive experience in residential construction, remodeling, home improvement, and tool use. Her practical approach to equipment evaluation focuses on usability, performance, safety, and value—helping DIYers and workshop users make better-informed decisions about compressors and related tools.