
Can I Put a Bigger Motor on My Air Compressor? Practical Guide for 2026
Wondering can i put a bigger motor on my air compressor? Learn mechanical limits, pulley ratios, electrical draw, and safety factors for October 2026.
 By Tony Carrick
Updated October 7, 2026

Air tool starvation frequently leaves workshop mechanics and woodworkers waiting for undersized storage tanks to recover pressure. When a continuous sander or paint gun drains line pressure below ninety PSI, many users wonder: can i put a bigger motor on my air compressor to boost performance? Swapping in a higher-horsepower electric motor sounds like an easy weekend upgrade, but pneumatic systems depend on a balanced relationship between motor torque, pump displacement, and tank safety ratings. Understanding how these mechanical components interact prevents expensive motor burnout, tripped breakers, and hazardous pressure spikes.
Direct-drive compressors integrate the pump and motor on a single shaft, making isolated motor swaps impractical without replacing the entire powerhead. Belt-driven models offer more mechanical flexibility, but simply increasing motor horsepower without adjusting pulley ratios will not produce extra airflow. Before investing in a larger motor or modifying your electrical supply, reviewing wiring electrical circuits for compressors helps determine whether your shop wiring can handle the increased amperage draw.
| Award | Product | ACR Score About ACR ScoreThe ACR Score is our own rating from 0 to 10, based on performance, design and build, ease of use, and value. It reflects independent research and is never influenced by manufacturers, retailers, or affiliate commissions. Learn more › | |
|---|---|---|---|
| Best Overall |
Baococo 4-Gallon 0.5 HP Air Compressor
|
9.2/10 | Buy |
| Best Value |
 Albott 10-Gallon 1.8 HP Air Compressor |
9.2/10 | Buy |
| Best Premium |
 Makita MAC2400 2.5 HP Air Compressor |
9.2/10 | Buy |
 HPDAVV 6.5HP 9-Gallon Gas Air Compressor |
9.2/10 | Buy | |
 MZB MZB-1100H-50 13.2-Gallon Air Compressor |
8.8/10 | Buy | |
| Best Budget |
 MZB MZB-900H-24 6.4-Gallon Air Compressor |
8.6/10 | Buy |
 Baococo 8 Gallon Portable Air Compressor |
8.6/10 | Buy | |
 MZB MZB-850H-9 2.4-Gallon Air Compressor |
8.1/10 | Buy | |
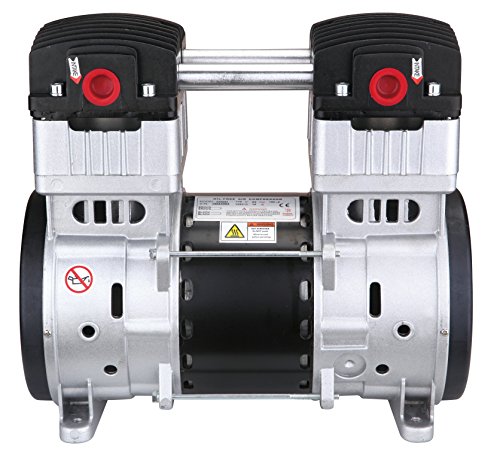 California Air Tools SP-9421 2.0 HP Motor |
8.1/10 | Buy | |
 BUNKER INDUST 12V Twin Motor Air Compressor |
8.0/10 | Buy |
Baococo 4-Gallon 0.5 HP Air Compressor
Built for light household maintenance and quick inflation tasks, this compact 4-gallon unit pairs a quiet 0.5 HP motor with an automatic overpressure safety shut-off. Its modest air delivery handles small nailers and tire filling without creating excessive workshop noise.
Pros
- Quiet operation suitable for residential spaces
- Automatic overpressure shut-off enhances operational safety
- Compact footprint stores easily in tight spaces
- Stable base minimizes movement during use
Cons
- Low airflow output limits heavy pneumatic tool use
- Maximum pressure capped at 110 PSI
- Modest 0.5 HP motor lacks heavy-duty capability
Albott 10-Gallon 1.8 HP Air Compressor
Built with an upright 10-gallon tank and a 1.8 HP motor, this Albott compressor delivers up to 115 PSI while saving workshop floor space. Its oil-free dual-piston pump and built-in wheels make it a low-maintenance option for garage projects and basic air tools.
Pros
- Compact vertical tank saves floor space
- Oil-free design requires minimal routine maintenance
- Equipped with wheels and handle for easier transport
- Dual fans provide active motor cooling
Cons
- Heavy at 80.5 pounds to lift manually
- Maximum pressure output capped at 115 PSI
Makita MAC2400 2.5 HP Air Compressor
Built for demanding jobsite tasks, this heavy-duty compressor pairs a rugged roll-cage frame with a low-RPM cast iron pump delivering 4.2 CFM at 90 PSI. Its low amp draw and cooler, oil-lubricated operation make it a dependable workhorse for contractors running pneumatic tools.
Pros
- Strong 4.2 CFM output at 90 PSI
- Protective roll-cage construction for jobsite durability
- Low 1,730 RPM pump runs quieter at 79 dB
- Low amp draw prevents tripped breakers at startup
Cons
- Oil-lubricated design requires routine oil level maintenance
- Substantial 20-inch footprint requires dedicated storage space
HPDAVV 6.5HP 9-Gallon Gas Air Compressor
Built for remote job sites and mobile service trucks, this gas-powered unit delivers 12 CFM at up to 125 PSI using a durable cast iron pump. Its wheelbarrow frame and vehicle-mount capability make it a dependable workhorse for field mechanics and heavy air tools where electricity is unavailable.
Pros
- High 12 CFM airflow runs demanding pneumatic equipment
- Cast iron pump head provides long-term mechanical durability
- Wheelbarrow frame simplifies transport across rough job sites
- Truck-mountable base adds versatility for field service
Cons
- Max pressure tops out at 125 PSI
- Gasoline engine requires regular engine maintenance and outdoor venting
- Large footprint takes up substantial bed space in vehicles
MZB MZB-1100H-50 13.2-Gallon Air Compressor
Designed for indoor workshops and residential garages, this compressor keeps operating noise down to a manageable 70 decibels. Its 13.2-gallon steel tank and wheeled frame suit DIY woodworkers, painters, and mechanics needing reliable airflow without regular pump maintenance.
Pros
- Quiet 70dB sound level ideal for indoor spaces
- Maintenance-free oil-free pump design
- Large 13.2-gallon durable steel tank
- Wheels and handle make transport manageable
Cons
- Hefty 72-pound weight makes vehicle loading difficult
- 115 PSI maximum pressure is modest for heavy-duty pneumatic tools
MZB MZB-900H-24 6.4-Gallon Air Compressor
Delivering 5.65 CFM at 115 psi, this 1.2 HP oil-free unit rapidly pressurizes its 6.4-gallon tank in about one minute while maintaining a low 70-decibel noise output. It serves well for home garages and workshops handling nail guns, air tools, and light painting.
Pros
- Quiet 70 dB operating volume
- Fast tank recovery under 65 seconds
- Generous 5.65 CFM output at 115 psi
- Low-maintenance oil-free motor design
- Integrated wheels assist mobility
Cons
- Steel construction adds significant carrying weight
- Tank capacity limits continuous heavy spraying sessions
- Corded operation requires standard electrical outlet
Baococo 8 Gallon Portable Air Compressor
The Baococo 8-gallon portable air compressor pairs a 2HP electric motor with a 150 PSI receiver tank, delivering 2.8 SCFM at 90 PSI. It provides a solid, accessible air source for garage DIYers tackling tire inflation, car detailing, and pneumatic finish nailing.
Pros
- Useful 8-gallon tank capacity cushions air demand better than smaller pancake style compressors
- 150 PSI peak tank pressure accommodates common automotive tire inflators and pneumatic nailers
- Standard 120V 60Hz power compatibility allows easy plug-and-play use in residential garages
- Sufficient airflow rating of 2.8 SCFM at 90 PSI for light woodworking, trim carpentry, and cleaning tasks
Cons
- Continuous high-CFM pneumatic tools like rotary sanders and heavy-duty 1/2-inch impact wrenches will quickly deplete tank reserves
- Contradictory product listing notes an oil-free tank in the title while mentioning regular oil checks in the description, requiring users to inspect pump details before first start
- Does not include an air hose, quick-connect fittings, or downstream regulator accessories in the box
MZB MZB-850H-9 2.4-Gallon Air Compressor
Built for carpentry, auto repair, and painting tasks, this compact compressor pairs a 1.2 HP oil-free motor with rapid 30-second tank recovery. Its steel frame and dual silencers balance durability with manageable 70 dB operation for portable workshop use.
Pros
- Fast 28 to 32 second tank fill time
- Maintenance-free oil-free motor design
- Solid 5.65 CFM output for its footprint
- Durable three-layer rust-resistant steel construction
Cons
- Maximum pressure is limited to 115 PSI
- Modest 2.4-gallon tank limits continuous heavy airflow
California Air Tools SP-9421 2.0 HP Motor
Designed for noise-sensitive workspaces, this 2.0 HP replacement motor operates at an ultra-quiet 70 decibels while delivering 5.3 CFM at 90 PSI. Its oil-free design makes it an ideal drop-in upgrade for users seeking dependable airflow without frequent pump maintenance.
Pros
- Low noise output rated at 70 decibels
- Oil-free design requires minimal ongoing maintenance
- Strong air delivery of 5.30 CFM at 90 PSI
- Includes intake air filter and operating capacitor
Cons
- Relatively heavy at 40 pounds
- Maximum pressure capped at 125 PSI
- Standalone motor unit requires existing tank and fittings
BUNKER INDUST 12V Twin Motor Air Compressor
Built for off-road rigs and overlanding vehicles, this twin-motor compressor airs up a 33-inch tire in under 2.5 minutes with its 100 percent duty cycle. The included 25-foot hose and ARB-friendly mounting make it a capable on-board or portable air source.
Pros
- Rapid inflation powered by dual cylinders and twin motors
- Continuous operation supported by 100 percent duty cycle
- Generous 25-foot hose easily reaches all four wheels
- Built-in bleeder valve allows precise tire pressure adjustments
Cons
- Heavier 29-pound build limits effortless handheld portability
- Requires substantial space for under-seat or engine-bay mounting
Mechanical Realities and Safety Limits of Compressor Motor Upgrades
Pneumatic tools demand steady airflow, but upgrading an existing compressor is rarely as straightforward as bolting on extra horsepower. The short answer to whether you can put a larger motor on your air compressor is technically yes on belt-driven platforms, but it will not increase your delivered airflow unless other mechanical components change. Direct-drive compressors also make an isolated motor swap virtually impossible because the pump crankshaft and motor rotor share a single housing. Before attempting any modification, you must understand how displacement physics, thermal thresholds, and electrical limits dictate compressor performance.
Direct-Drive Versus Belt-Drive Architecture
Direct-drive air compressors connect the electric motor armature directly to the pump crankshaft inside a compact, unified chassis. Portable units like the Makita MAC2400 or compact oil-free models from Baococo and Albott utilize this space-saving design to minimize weight and eliminate belt maintenance. Because the motor bearings and pump eccentric journals are machined into one shared housing, you cannot remove the motor while leaving the pump intact. Swapping a motor on a direct-drive unit requires replacing the complete motor and pump powerhead as a single pre-assembled unit.
Belt-driven compressors separate the electric motor from the pump head, mounting both components to a heavy steel baseplate welded across the tank top. A drive pulley on the motor shaft transfers rotational power through a V-belt to the larger flywheel pulley on the cast-iron pump. This physical separation makes it mechanically possible to unbolt the factory motor and install a different unit with a higher horsepower rating. However, the new motor must share compatible NEMA frame dimensions, shaft diameters, baseplate bolt patterns, and rotational direction to align properly with the existing pump flywheel.
Misaligned pulleys or incorrect belt tension can introduce severe side-loading forces that destroy motor bearings and pump shaft seals within hours. Even if the new motor physically fits the compressor saddle, you must verify that the motor shaft height and center distance allow proper belt tensioning. Many aftermarket motors feature different face mounts or shaft keyway dimensions that require custom mounting plates or replacement pulleys. Physical fit is only the first obstacle, as the mechanical relationship between motor speed and pump displacement governs actual air delivery.
Why a Bigger Motor Alone Does Not Increase CFM Output
Air delivery volume, measured in cubic feet per minute, is determined entirely by pump cylinder displacement and pump rotational speed. The pump cylinder bore diameter, stroke length, and number of compression stages establish how much atmospheric air the pistons draw in per revolution. Motor horsepower represents the mechanical torque available to turn that pump against rising tank pressure without stalling or overheating. Installing a motor with double the horsepower rating simply provides surplus torque, while the pump continues to rotate at the exact same speed dictated by the motor pulley.
Because standard induction motors run at fixed speeds, usually around 1,750 or 3,450 revolutions per minute, keeping the original pulleys produces the exact same pump RPM. With identical RPM and unchanged cylinder volume, your compressor will produce identical CFM output at forty and ninety PSI. The larger motor will not compress air any faster, nor will it shorten tank recovery times during heavy pneumatic tool operation. An oversized motor running a pump designed for lower power operates underloaded, drawing unnecessary electrical current without providing any operational advantage.
Some operators mistakenly assume that extra motor power forces more air molecules into the tank on each piston stroke. In reality, the intake reed valves only admit ambient air until the cylinder reaches atmospheric pressure during the downward piston stroke. Extra motor torque cannot alter atmospheric density or force additional air through the intake ports. Unless the pump rotates faster or features larger cylinder bores, air volume generation remains completely static regardless of motor size.
The Serious Risks of Over-Spinning a Compressor Pump
When mechanics realize a larger motor alone does not increase airflow, the next instinct is to install a larger motor pulley to spin the pump faster. While increasing pump RPM does displace more air per minute, compressor pumps are carefully engineered for specific maximum operating speeds. Forcing a cast-iron or aluminum pump beyond its rated RPM dramatically accelerates mechanical wear, friction, and heat generation. Most consumer and workshop pump heads are balanced for rotational speeds between 700 and 1,200 RPM, and exceeding those thresholds invites catastrophic failure.
Extreme thermal expansion represents the primary danger of over-spinning a reciprocating compressor pump head. Compression creates massive heat, and spinning the pistons faster reduces cooling intervals between cycles while overwhelming the pump cooling fins. Excessive heat causes lubricating oil to break down and oxidize rapidly, leading to piston scoring, cylinder galling, and wrist pin seizure. Maintaining proper compressor pump lubrication helps protect standard equipment, but no oil can withstand the extreme friction generated by an over-spun pump assembly.
Valve flutter and mechanical fatigue also increase exponentially when pump rotational speeds exceed factory design specifications. The thin spring-steel reed valves or disc valves inside the cylinder head must seat and seal hundreds of times per minute. Operating beyond rated RPM causes reed valves to flutter rather than seal cleanly, resulting in blow-by, severe CFM loss, and eventual metal breakage. If a shattered valve fragment falls into the cylinder, it will strike the piston crown and destroy the entire cylinder assembly instantly.
Electrical Circuit Demands and Breaker Compatibility
Electric motors require substantial electrical power, and stepping up in motor horsepower dramatically increases running and starting current. A standard 1.5 to 2.0 horsepower motor draws between twelve and fifteen running amps on a standard 120-volt household circuit. Upgrading to a genuine 3.0 or 5.0 horsepower motor pushes running amperage well beyond what a standard fifteen-amp or twenty-amp residential breaker can supply. Attempting to run a larger motor on inadequate electrical wiring will trip branch breakers immediately upon startup.
Electric compressor motors also draw massive inrush current during the first few cycles as the motor overcomes head pressure and accelerates. Inrush current can reach three to five times the motor running amperage rating, placing severe stress on branch circuit wiring. Undersized branch wiring causes voltage drop, which deprives the motor of starting torque and leads to stalled rotors and burned start windings. If you install a larger motor, you must ensure your electrical panel features adequate wire gauge and dedicated circuit breaker capacity to handle peak startup demand.
Switching to a larger motor often necessitates upgrading from a 120-volt single-phase supply to a dedicated 240-volt circuit. Larger motors also require upgraded magnetic starters and heavy-duty pressure switches capable of handling higher electrical arcs across contact points. Standard pressure switches designed for compact garage compressors will weld their contacts shut when switching high-horsepower inductive loads. Replacing electrical panels, running conduit, and installing magnetic contactors quickly inflates the financial cost of what seemed like a minor motor upgrade.
Air Tank Safety Limits and ASME Pressure Ratings
Some compressor owners pursue motor upgrades under the mistaken belief that more horsepower will increase the maximum tank pressure. In a properly functioning pneumatic system, maximum tank pressure is governed strictly by the factory pressure switch calibration and ASME safety relief valve. Every steel air tank features a certified maximum allowable working pressure stamped into its metal data plate. A bigger motor will not and should not push tank storage pressure beyond the manufacturer certified limit, because doing so creates catastrophic explosion risks.
The ASME safety relief valve installed on the tank manifold protects operators by popping open if pressure exceeds safe thresholds. Tampering with the pressure switch cut-out setting or installing an oversized relief valve to exploit extra motor power violates basic workshop safety standards. Air tanks experience metal fatigue from continuous pressurization and moisture-induced internal corrosion over years of service. Forcing an aging tank to hold higher pressures than its engineered rating risks sudden structural rupture and severe physical injury.
Motor horsepower also impacts compressor duty cycle, which is the ratio of operating time to resting time required to dissipate heat. While a larger motor may operate with a cooler motor casing, the air tank and pump still require adequate resting intervals. Small four-gallon to ten-gallon air tanks offer minimal buffer capacity, causing the pump to cycle frequently under continuous tool use. If your storage capacity is too small for your work, a bigger motor will not resolve pressure fluctuation or prevent hot air delivery down your pneumatic lines.
Sizing Pneumatic Tool Air Consumption Accurately
Before considering any compressor modification, evaluating the actual airflow demands of your pneumatic tools provides essential perspective. Different pneumatic tools consume air in fundamentally different ways based on whether they operate intermittently or continuously. Fastener tools like brad nailers, finish nailers, and framing nailers consume discrete bursts of air, requiring relatively low continuous CFM output. Reviewing matching compressor output to pneumatic tools illustrates how small tanks and modest motors easily support intermittent fastening tasks without pressure starvation.
Continuous pneumatic tools like dual-action rotary sanders, die grinders, cut-off wheels, and HVLP paint sprayers demand immense sustained airflow. A typical orbital sander consumes eight to twelve CFM at ninety PSI, which far exceeds the production capability of compact garage compressors. When a tool consumes air faster than the pump can compress it, line pressure collapses regardless of motor horsepower. Trying to solve continuous tool starvation by swapping motors on a light-duty compressor is mechanically futile because the underlying pump head displacement remains inadequate.
Matching your workshop workload to delivered CFM ratings ensures consistent tool torque and superior finishing results. If your tools require ten CFM at ninety PSI, your compressor pump must physically displace enough air to replenish that consumption in real time. Upgrading a motor on a small two-CFM pump will never bridge that performance deficit, no matter how much horsepower you add. Understanding your pneumatic consumption profile helps redirect your investment toward practical equipment solutions that actually deliver required airflow.
Unified Replacement Motor and Pump Assemblies
For direct-drive and oil-free air compressors, replacing the unified motor and pump assembly represents the only practical upgrade path. Manufacturers like California Air Tools engineer integrated powerheads, such as the SP-9421 2.0HP ultra-quiet oil-free motor pump unit, which combines twin cylinders and motor coils in one balanced package. These replacement assemblies produce verified airflow ratings, such as 5.3 CFM at ninety PSI, while maintaining low operating noise around seventy decibels. Installing a complete factory-engineered assembly eliminates the mechanical mismatch risks associated with custom motor retrofits.
When replacing a complete powerhead assembly, you must verify mounting foot spacing, capacitor wiring connections, and plumbing discharge line compatibility. The aluminum or copper unloader tube and tank check valve must align properly with the new cylinder head discharge port to prevent air leaks. High-efficiency dual-piston oil-free assemblies feature dual intake air filters and specialized Teflon piston rings that require clean, dry operating environments. While complete assemblies offer clean air delivery and zero oil maintenance, they still require dedicated electrical circuits to prevent voltage sag.
Evaluating the total expenditure of a replacement powerhead against the cost of a complete brand-new compressor is essential before purchasing parts. A complete motor-pump assembly requires transferring your existing tank, pressure switch, safety valve, drain cock, and regulator manifold. If your air tank exhibits internal rust or the factory pressure switch is worn, rebuilding the system around an old tank offers poor long-term value. In many workshop scenarios, purchasing a factory-balanced new compressor provides fresh warranty coverage and updated safety components for comparable total investment.
Practical Workshop Alternatives to Motor Swapping
Instead of attempting risky and expensive motor modifications, several proven workshop alternatives can dramatically improve your pneumatic performance. Adding an auxiliary air storage tank plumbed in parallel with your primary compressor increases usable reserve volume significantly. A secondary tank acts as an air capacitor, storing compressed air during idle periods so you can operate high-demand tools for longer bursts without immediate pressure drop. While an auxiliary tank does not increase pump CFM output, it extends working duration before pressure drops below operational thresholds.
Running two smaller air compressors simultaneously using a manifold tee fitting and dual check valves provides another reliable way to double delivered CFM. By combining the output of two separate 120-volt compressors plugged into different electrical circuits, you achieve high airflow without overloading household wiring. This dual-compressor configuration offers tremendous flexibility, allowing you to run one unit for light nailing and fire up both units for spray painting or grinding. Each compressor operates within its factory-engineered limits, preserving component longevity and maintaining full manufacturer safety standards.
Upgrading to a dedicated, purpose-built stationary workshop compressor remains the ultimate long-term solution for demanding pneumatic applications. Heavy-duty two-stage cast-iron compressors engineered with continuous-duty electric motors deliver the sustained high CFM and pressure stability that modified consumer units cannot match. These commercial systems feature balanced flywheels, large oil reservoirs, magnetic starters, and ASME-certified pressure vessels designed specifically for high duty cycles. Investing in engineered air delivery equipment protects your workshop safety, eliminates electrical headaches, and guarantees consistent tool performance across every project.
About the author
Tony Carrick is an experienced product researcher and writer specializing in tools, home improvement, automotive maintenance, and consumer equipment. With extensive experience reviewing tools and tackling hands-on renovation projects, he brings a buyer-focused perspective to compressor performance, usability, and overall value.