
How Reciprocating Air Compressor Works: Practical Guide for 2026
Learn how reciprocating air compressor works and how cylinder strokes, pressure valves, and pump stages generate reliable pneumatic power in October 2026.
 By Tom Scalisi
Updated October 8, 2026

Pneumatic power systems rely on reliable mechanical pressure generation to drive everything from framing nailers to continuous automotive tools. Understanding how reciprocating air compressor works provides valuable clarity when sizing equipment for a workshop, diagnosing line pressure loss, or selecting the proper pump configuration for demanding pneumatic air tools. The reciprocating mechanism serves as the backbone of modern positive-displacement compression, converting rotary mechanical force from an electric motor or gas engine into stored pneumatic energy. By examining the physical movement of the internal piston assembly, workshop owners and tradespeople can better assess air delivery volume, heat dissipation, and overall system longevity.
Every compression cycle involves precise timing between cylinder intake suction, piston stroke displacement, and automatic valve movement. Learning how reciprocating air compressor works allows operators to match tool consumption rates against delivered CFM at 90 PSI without stalling pneumatic equipment mid-cut or burning out electric motors. Whether inspecting a compact oil-free jobsite pancake pump or an industrial two-stage cast-iron workshop installation, the underlying principles of air displacement dictate usable tool pressure and daily reliability. Taking the time to understand these mechanical dynamics ensures that your pneumatic system operates efficiently while avoiding common pitfalls like thermal overload or internal tank rust.
| Award | Product | ACR Score About ACR ScoreThe ACR Score is our own rating from 0 to 10, based on performance, design and build, ease of use, and value. It reflects independent research and is never influenced by manufacturers, retailers, or affiliate commissions. Learn more › | |
|---|---|---|---|
| Best Overall |
Ingersoll Rand 429 3/8" Reciprocating Air Saw
|
9.2/10 | Buy |
| Best Budget |
 Ingersoll Rand 47853635004-R Startup Kit with All |
8.9/10 | Buy |
| Best Premium |
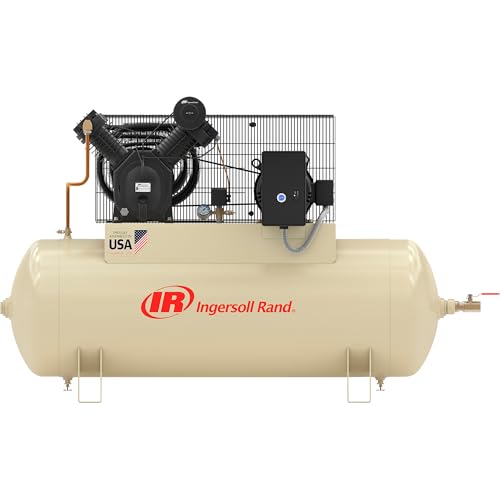 Ingersoll Rand Type-30 Reciprocating Air |
8.8/10 | Buy |
 Metabo HPT 6-Gallon Pancake Air Compressor Review |
8.6/10 | Buy | |
| Best Value |
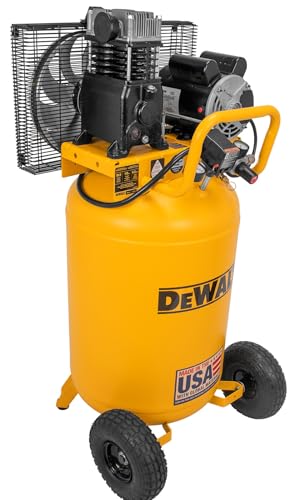 DEWALT 30-Gallon Vertical Portable Electric Air |
8.3/10 | Buy |
 Air Lift 25980EZ WirelessONE Air Compressor |
8.1/10 | Buy | |
 Ingersoll Rand Type-30 Reciprocating Air |
8.0/10 | Buy |
Ingersoll Rand 47853635004-R Startup Kit with All
This genuine Ingersoll Rand startup kit provides 2 years of All Season Select synthetic lubricant and replacement air filter elements to prevent carbon buildup and wear on compatible reciprocating compressors. It is an essential investment for shop owners and mechanics running Ingersoll Rand 2200, 2340, 2475, or TS4 models who want extended factory warranty protection.
Pros
- Activates extended 2-year bumper-to-bumper and 5-year tank warranty coverage on eligible Ingersoll Rand units
- Includes two full years of factory-matched synthetic oil and intake air filters
- All Season Select synthetic blend minimizes carbon deposits under heavy duty cycles
- OEM fitment ensures hassle-free filter replacement without pump modifications
Cons
- Compatible only with specific Ingersoll Rand models (2200, 2340, 2475, TS4) and cannot be used with other compressor brands
- Covers only routine fluid and air intake maintenance, excluding mechanical parts like drive belts, gaskets, or drain valves
Metabo HPT 6-Gallon Pancake Air Compressor Review
The Metabo HPT EC711S is a portable 6-gallon pancake air compressor delivering 2.8 CFM at 90 PSI with a 165 PSI tank ceiling and an operating sound level of 73 dB. With its quick 46-second recovery cycle and dual quick couplers, it is an excellent choice for finish carpenters, punch-list contractors, and DIYers running pneumatic nailers.
Pros
- 73 dB operational sound rating is substantially quieter than standard job-site pancake units
- 165 PSI maximum pressure provides ample air storage with a swift 46-second recovery cycle
- Two 1/4-inch universal quick couplers support multi-tool setups right out of the box
- Sturdy steel roll cage protects gauges and the manifold assembly against knocks and drops
- Oil-free 1.0 HP motor ensures low maintenance and reliable cold-weather motor startup
Cons
- At 38.5 lbs, it is slightly heavier than ultra-compact 1-to-3-gallon trim compressors
- Airflow of 2.8 CFM at 90 PSI is designed for intermittent fastening, not continuous rotary tools or paint sprayers
- Bare-tool configuration means air hoses and pneumatic fastening tools must be purchased separately
Air Lift 25980EZ WirelessONE Air Compressor
Designed for effortless vehicle leveling, the Air Lift 25980EZ combines a pre-assembled 12V compressor with wireless app and remote control. It is an ideal on-board inflation solution for drivers regularly towing or hauling heavy payloads.
Pros
- Pre-assembled bracket noticeably cuts down installation time
- Dual control options via wireless remote or mobile app
- Capable 120 PSI output handles demanding towing needs
- Three custom presets enable quick pressure adjustments
- Backed by a two-year manufacturer warranty
Cons
- Single-path system cannot level side-to-side loads independently
- Maximum pressure output capped at 120 PSI
- Requires adequate vehicle underbody mounting clearance
Operating Principles and Mechanics of Reciprocating Air Compressors
A reciprocating air compressor operates on the fundamental principle of positive displacement, using a mechanical piston to physically reduce the volume of trapped air inside a sealed cylinder. As the air volume decreases, the internal pressure increases proportionally until the compressed air overcomes downstream resistance and discharges into an air storage tank. This mechanical approach remains one of the most widely utilized compression methods across home workshops, automotive service bays, and industrial facilities. Understanding this mechanical sequence reveals why pump design, cylinder staging, and valve efficiency directly determine the sustained pneumatic performance available at your air hose connection.
The Cylinder Stroke Cycle: Intake and Compression Stages
The reciprocating cycle begins when an external power source, such as an electric motor, turns the pump crankshaft inside the crankcase. As the crankshaft rotates, it drives the connecting rod, which pulls the piston downward from top dead center to bottom dead center inside the precision-machined cylinder. This downward motion dramatically increases the volume inside the cylinder bore, creating an immediate atmospheric pressure drop or partial vacuum above the piston crown. Because the cylinder pressure is now lower than surrounding ambient atmospheric pressure, incoming air forces the intake reed or flapper valve open to flood the cylinder chamber.
Once the piston reaches the absolute bottom of its travel, the crankshaft continues its rotation and reverses the piston direction upward. As the piston begins ascending toward top dead center, the internal volume immediately contracts, causing cylinder pressure to rise above atmospheric levels. This sudden pressure equalization immediately forces the flexible intake reed valve closed against its valve seat, sealing the air charge inside the cylinder. With nowhere to escape, the trapped air molecules are compressed closer together, causing both the air pressure and internal temperature to rise rapidly during the compression stroke.
Near the peak of the upward stroke, the rising air pressure inside the cylinder exceeds the static pressure maintained in the discharge line and air receiver tank. This pressure differential forces the spring-loaded discharge valve open, allowing the highly pressurized air to evacuate the cylinder bore and enter the discharge tube. When the piston reaches top dead center, the discharge valve snaps shut, preventing any compressed air from returning backward into the chamber. The crankshaft then pulls the piston downward once again, repeating this rapid cyclical process hundreds or thousands of times every minute.
Valve Operation: Reed, Flapper, and Disc Valve Dynamics
Unlike automotive combustion engines that rely on mechanical camshafts and timing belts to actuate valves, reciprocating air compressor pumps utilize automatic pressure-actuated valves. These components typically take the form of thin, highly flexible spring-steel reed valves, flapper strips, or spring-loaded concentric disc valves situated between the cylinder head and valve plate. These valves function strictly as passive one-way check mechanisms, opening and closing in direct response to pressure differentials created across the valve port faces. The absence of mechanical timing gears reduces pump complexity while ensuring lightning-fast valve responses during high-speed motor rotation.
During the intake stroke, ambient air enters through the intake air filter element, which traps airborne dust and abrasive debris before it can score the cylinder walls. The slight vacuum generated by the descending piston pulls the intake reed downward away from its flat ground seat, clearing a path for fresh air. Once compression commences, the upward force of the compressed air firmly presses the intake reed flat against its cast seat, forming a leak-free mechanical seal. If dirt accumulates or carbon builds up on this sealing face, intake air can leak backward, drastically reducing delivered CFM output and extending tank fill times.
The discharge valve operates under identical pressure principles but faces considerably higher thermal and pneumatic stresses. As compressed air reaches target discharge pressure, it overcomes the stiffness of the discharge reed or retainer spring, escaping into the manifold line. When the piston reverses direction at top dead center, the higher pressure in the discharge tube instantly slams the discharge valve closed. Any physical wear, heat warpage, or metal fatigue on the discharge valve plate allows pressurized air to bleed back into the cylinder during intake strokes, causing chronic pump overheating and severe loss of volumetric efficiency.
Single-Stage Versus Two-Stage Compression Mechanics
Reciprocating air compressors are broadly divided into single-stage and two-stage architectures based on how many compression steps the air undergoes before reaching storage. In a single-stage compressor pump, ambient air enters the cylinder and is compressed directly to final storage tank pressure in one complete upward stroke. Most portable consumer units, such as the Metabo HPT pancake air compressor, utilize a single-stage design to achieve maximum working pressures around 165 PSI with high mechanical simplicity. Single-stage configurations excel in intermittent trade work, light nailing, and general workshop tire inflation where continuous high-volume air demands remain modest.
Two-stage reciprocating compressors divide the total compression workload across two distinct cylinders of differing sizes. Ambient air first enters a large, low-pressure cylinder where it undergoes initial compression to an intermediate pressure, typically between 40 and 60 PSI. Instead of routing directly into the air tank, this pre-compressed air discharges through an external finned intercooler tube directly into a smaller high-pressure cylinder. The smaller cylinder then completes the second compression phase, driving the air up to industrial working pressures of 175 PSI or higher.
The physical inclusion of an intercooler between stages represents a critical engineering advantage in heavy-duty reciprocating systems. Compressing air generates substantial thermal energy, and cooling the intermediate air between stages reduces air volume and lowers operating temperatures before secondary compression. Premium industrial units, such as the Ingersoll Rand Type-30 reciprocating air compressors with 100% cast iron construction, incorporate finned copper intercoolers between cylinders to dissipate excessive heat effectively. This staged cooling reduces thermal stress on internal valves, increases overall volumetric compression efficiency, and prevents synthetic lubricant breakdown during sustained operation.
Lubrication Architectures: Oil-Free Versus Cast-Iron Splash Lubrication
The method used to lubricate moving parts inside the pump crankcase fundamentally impacts maintenance requirements, noise generation, and operational lifespan. Modern lightweight portable compressors frequently employ oil-free pump mechanisms featuring Teflon or PTFE-coated piston rings and permanently sealed roller bearings. These oil-free systems eliminate the need for regular crankcase oil checks, allow the compressor to operate reliably on uneven slopes, and guarantee oil-free discharge air. However, because they lack liquid cooling and lubrication, oil-free pumps typically generate higher operational noise levels and have lower continuous duty cycle ratings.
Commercial workshops and industrial facilities generally prefer oil-lubricated reciprocating pumps built with heavy-duty cast-iron cylinders and aluminum or cast crankcases. In these systems, an oil dipper attached to the bottom of the one-piece connecting rod splashes oil throughout the crankcase with every crankshaft rotation. This continuous oil mist coats cylinder walls, wrist pins, and main bearings, reducing frictional heat and creating a hydraulic seal across the piston compression rings. Units utilizing solid cast-iron cylinders offer superior thermal mass, effectively absorbing and radiating away intense compression heat during extended operation.
Maintaining proper oil quality is crucial for protecting the internal reciprocating components against premature friction and carbonization. Synthetic all-temperature lubricants, such as Ingersoll Rand All Season Select synthetic oil, are specifically engineered to resist thermal degradation and prevent carbon buildup on sensitive valve assemblies. Using a proper startup kit with matched synthetic lubricants and replacement air filter elements ensures optimal cylinder protection across thousands of operating hours. Failure to monitor the oil sight glass or operating with degraded lubricant can quickly lead to wrist-pin galling, piston ring seizure, and catastrophic connecting rod failure.
Pneumatic Regulation and Safety Controls: Pressure Switches, Check Valves, and Unloaders
A reciprocating compressor pump does not operate in isolation; it functions as part of an integrated pneumatic control circuit designed to automate pressure delivery safely. The central control component is the electromechanical pressure switch, which monitors the static air pressure inside the storage reservoir tank. When tank pressure falls below a factory-calibrated cut-in threshold, internal contacts snap shut to energize the electric motor and initiate compression. Once the pump raises tank pressure to the preset cut-off limit, the switch contacts open, immediately cutting power to the motor.
Directly connected to the pressure switch is a small unloader valve, which serves a vital mechanical role during motor shutdown cycles. When the pressure switch trips off at maximum tank PSI, the unloader valve immediately opens, releasing any trapped high-pressure air resting between the pump cylinder heads and the tank. This audible brief hiss depressurizes the pump discharge line, ensuring the piston does not face trapped head pressure when the motor restarts. Without a functioning unloader valve, the electric motor must overcome immense head resistance during startup, frequently tripping 15-amp branch circuit breakers or stalling out completely.
Between the pump discharge line and the air receiver tank sits a heavy-duty one-way brass check valve. This valve permits pressurized air to flow into the receiver tank during the compression stroke but mechanically blocks stored air from escaping back toward the pump. If this check valve becomes contaminated with carbon or debris, tank pressure leaks continuously backward through the unloader valve whenever the compressor is shut off. Operators should also regularly inspect the spring-loaded ASME safety relief valve mounted on the tank, which automatically pops open to vent excess pressure if the primary pressure switch fails to cut off the motor.
Storage Buffers, Recovery Cycles, and Air Tool Consumption
The receiver tank on a reciprocating air compressor acts as an energy storage capacitor, smoothing out the pulsating air discharges produced by the cycling piston. Compressed air enters the tank in rapid, discrete pulses, and the reservoir volume absorbs these pressure surges to supply a smooth, continuous air stream to downstream pneumatic tools. Tank size also determines how long an operator can run pneumatic equipment before the internal pressure drops to the cut-in threshold, triggering pump restart. Vertical tanks, such as the DEWALT 30-gallon vertical portable electric air compressor, provide a substantial storage buffer while maintaining a compact workshop floor footprint.
Matching the compressor pump delivery rate to the air consumption of specific pneumatic tools is essential for maintaining productivity. Air delivery is measured in cubic feet per minute at specified pressures, primarily CFM at 90 PSI or CFM at 40 PSI. Intermittent tools like finish nailers and tire inflators consume minimal overall air volume, allowing compact 6-gallon pancake compressors to cycle comfortably between shots. In contrast, continuous air tools require substantial air volume; for example, an Ingersoll Rand 429 reciprocating air saw requires at least 8 CFM at 90 PSI to maintain full cutting performance.
When a pneumatic tool consumes more CFM than the reciprocating pump can generate, the air tank buffer quickly drains and working pressure drops below tool operating requirements. In such scenarios, the pump runs continuously without cycling off, leading to rapid heat accumulation and possible thermal overload shutdown. Understanding your tool air consumption profile allows you to select an appropriate pump displacement and tank capacity, preventing unwanted work interruptions. Utilizing a high-flow pressure regulator further optimizes performance by providing consistent, usable line pressure directly to the tool without creating unnecessary internal restrictions.
Condensation Dynamics and Routine Preventative Maintenance
A natural physical consequence of the reciprocating air compression process is the generation and accumulation of moisture inside the receiver tank. Atmospheric ambient air always contains a degree of water vapor, and compressing this air into a fraction of its original volume supersaturates the air charge. As the hot compressed air enters the cooler steel receiver tank, the water vapor quickly condenses into liquid water that pools along the tank floor. If left unmanaged, this acidic moisture promotes internal rust, compromises tank wall structural integrity, and travels down air lines to contaminate pneumatic tools and paint finishes.
To protect against internal corrosion, operators must purge accumulated moisture through the tank bottom drain valve after every work session. Traditional threaded needle petcocks can be stiff and prone to seizing, whereas quarter-turn brass ball valves provide quick, effortless draining that encourages daily maintenance routines. Depressurizing the tank completely and leaving the drain valve slightly cracked during off-duty storage prevents moisture stagnation and helps dry out internal tank surfaces. Clean, moisture-free storage preserves the receiver tank for years of safe operation while ensuring downstream tools receive dry, reliable pneumatic power.
Beyond daily moisture purges, maintaining clean intake air filters represents the most effective way to prevent premature piston and ring wear. Restricted intake filters choke airflow into the cylinder, forcing the reciprocating pump to work harder, run hotter, and deliver reduced CFM output. Periodic inspection of pump belt tension on belt-driven models, coupled with visual checks of oil level and clarity on lubricated units, ensures reliable mechanical operation. Adhering to these fundamental maintenance routines keeps the reciprocating assembly operating smoothly, delivering consistent pressure and volume for all your workshop and jobsite projects.
Understanding the mechanical principles behind reciprocating compression transforms how you operate, maintain, and select workshop air power systems. From the downward intake stroke of the piston to the automated cycling of the pressure switch and unloader valve, every component plays a specific role in delivering stored pneumatic force. Proper valve care, moisture draining, and realistic CFM matching ensure your compressor runs reliably without unexpected downtime or pressure drops. By matching your tool air consumption demands to a properly configured pump and tank setup, you can ensure dependable performance across any residential, automotive, or jobsite application.
About the author
Tom Scalisi brings more than two decades of experience in construction, building maintenance, contracting, and hands-on tool use. His practical understanding of power tools, automotive work, repairs, and jobsite equipment helps readers evaluate compressors based on real workloads rather than specifications alone.