
How Does a Screw Type Air Compressor Work: Mechanics and Operation Guide for 2026
Learn how does a screw type air compressor work to deliver continuous pneumatic flow. Practical operation guide for October 2026.
 By Tony Carrick
Updated October 8, 2026

Air-hungry industrial machinery and continuous manufacturing tools often overwhelm standard reciprocating compressors, leading to thermal shutdowns and fluctuating line pressure. Understanding how does a screw type air compressor work reveals why heavy production facilities rely on rotary screw technology for steady pneumatic output. Unlike piston pumps that push air in rapid pulses, screw compressors compress air continuously through smooth mechanical rotation. This continuous operation enables a complete one hundred percent duty cycle without the thermal strain typical of conventional garage pumps.
Piston units handle intermittent tasks like framing nailers with ease, but rotary screw units solve the problem of uninterrupted air volume. Industrial setups running CNC machines, automated assembly lines, or continuous spray systems require massive cubic feet per minute ratings that only twin-screw mechanisms can reliably generate. By exploring the internal mechanics of interlocking helical rotors, equipment operators can properly evaluate air demands, operational noise limits, and system efficiency. Modern rotary technology ensures predictable pressure delivery while lowering maintenance frequency across rigorous workshop environments.
| Award | Product | ACR Score About ACR ScoreThe ACR Score is our own rating from 0 to 10, based on performance, design and build, ease of use, and value. It reflects independent research and is never influenced by manufacturers, retailers, or affiliate commissions. Learn more › | |
|---|---|---|---|
| Best Overall |
ALL-TOP Dual Cylinder 12V Air Compressor
|
9.2/10 | Buy |
| Best Premium |
 Bilowk 15HP Variable Speed Screw Compressor |
8.9/10 | Buy |
| Best Budget |
 QWORK Air Compressor Pressure Switch Manifold |
8.6/10 | Buy |
 ECOMAX Wall Mount 0.5-Gal Air Compressor |
8.6/10 | Buy | |
| Best Value |
 Metabo HPT 6-Gallon Pancake Air Compressor Review |
8.6/10 | Buy |
 DEWALT DWFP55130 2.5-Gallon 200 PSI Quiet Trim Air |
8.4/10 | Buy | |
 Harrier Hardware 11-Piece Air Compressor Starter |
8.3/10 | Buy |
ALL-TOP Dual Cylinder 12V Air Compressor
Built for rapid tire inflation on large trucks and off-road rigs, this dual-cylinder pump pushes an impressive 12.35 CFM flow rate up to 150 PSI. The rugged metal frame, integrated thermal safeguards, and extended 26-foot hose provide reliable utility for heavy-duty vehicle recovery.
Pros
- High 12.35 CFM output swiftly inflates large tires
- Dual aluminum cylinder construction helps dissipate heat
- Generous 26-foot hose reaches all corners of large vehicles
- Equipped with automatic thermal and over-current safety switches
Cons
- Heftier 24-pound build demands extra carrying effort
- Third-party gauges require built-in over-pressure protection
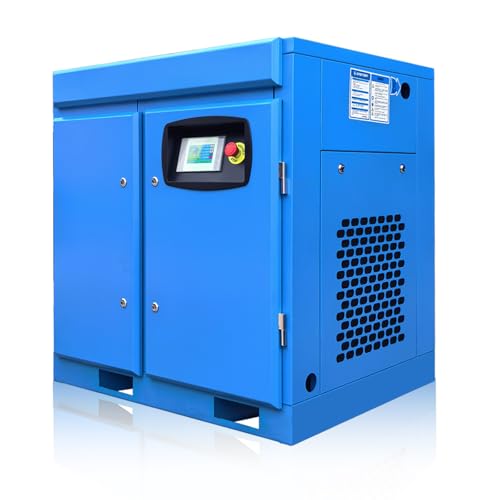
Bilowk 15HP Variable Speed Screw Compressor
Designed for high-demand industrial facilities, this Bilowk rotary screw compressor delivers 61 CFM while dynamically adjusting motor output to conserve energy. Its variable-frequency soft start minimizes electrical surges, making it a dependable choice for continuous shop operation.
Pros
- High 61 CFM airflow supports demanding industrial machinery
- Variable speed operation optimizes energy consumption
- Soft-start motor produces lower noise and stable pressure
- Low maintenance requirements with periodic filter changes
Cons
- Strictly requires 3-phase power and incompatible with phase converters
- Heavy 507-pound footprint makes repositioning difficult
- Must be sheltered indoors away from humidity and dust
QWORK Air Compressor Pressure Switch Manifold
The QWORK Air Compressor Pressure Switch Manifold provides an integrated pressure switch, regulator, and dual gauges with a factory 90 to 120 PSI cycling range. It suits DIYers and shop owners looking to rebuild a compressor manifold, though American users must note its G1/4 BSP thread sizing requires adapters for standard NPT equipment.
Pros
- Factory-set 90 to 120 PSI cut-in and cut-out cycling provides stable air supply regulation
- Convenient pre-assembled manifold block integrates dual monitoring gauges and a pressure regulator
- Solid pressure tolerance capable of handling equipment setups up to 175 PSI maximum
- Reinforced ABS cover protects electrical switch contacts from shop dust and debris
Cons
- Features G1/4 BSP threaded ports, meaning standard 1/4-inch NPT American fittings will not thread directly without adapters
- Fittings are constructed from iron rather than solid brass, requiring careful sealing against moisture corrosion
- Adjustment instructions are minimal, requiring users to carefully verify cut-in and cut-out settings before operation
ECOMAX Wall Mount 0.5-Gal Air Compressor
Built for garage workshops, this space-saving wall-mounted unit integrates a 30-foot retractable hose reel and a low-maintenance oil-free motor. The 0.5-gallon tank and 125 PSI output make it ideal for tire inflation and light pneumatic fastening without cluttering floor space.
Pros
- Convenient built-in retractable 30-foot hose reel
- Low-maintenance oil-free motor design
- Wall-mount form factor frees up workshop floor space
- Solid 125 PSI maximum working pressure
Cons
- Small 0.5-gallon tank limits continuous high-demand airflow
- Does not include starter air tool accessories
- Relatively heavy at nearly 21 pounds to mount
Metabo HPT 6-Gallon Pancake Air Compressor Review
The Metabo HPT EC711S is a portable 6-gallon pancake air compressor delivering 2.8 CFM at 90 PSI with a 165 PSI tank ceiling and an operating sound level of 73 dB. With its quick 46-second recovery cycle and dual quick couplers, it is an excellent choice for finish carpenters, punch-list contractors, and DIYers running pneumatic nailers.
Pros
- 73 dB operational sound rating is substantially quieter than standard job-site pancake units
- 165 PSI maximum pressure provides ample air storage with a swift 46-second recovery cycle
- Two 1/4-inch universal quick couplers support multi-tool setups right out of the box
- Sturdy steel roll cage protects gauges and the manifold assembly against knocks and drops
- Oil-free 1.0 HP motor ensures low maintenance and reliable cold-weather motor startup
Cons
- At 38.5 lbs, it is slightly heavier than ultra-compact 1-to-3-gallon trim compressors
- Airflow of 2.8 CFM at 90 PSI is designed for intermittent fastening, not continuous rotary tools or paint sprayers
- Bare-tool configuration means air hoses and pneumatic fastening tools must be purchased separately
DEWALT DWFP55130 2.5-Gallon 200 PSI Quiet Trim Air
The DEWALT DWFP55130 delivers a capable 3.0 SCFM at 90 PSI with a 200 max PSI 2.5-gallon tank, running at a quiet 71.5 dBA on an efficient 12-amp motor. It is an ideal pneumatic power source for trim carpenters, punch-list contractors, and DIYers working on residential circuits.
Pros
- Delivers 3.0 SCFM at 90 PSI with a high 200 max PSI ceiling for rapid pressure recovery during sequential fastening
- Quiet 71.5 dBA sound output makes indoor trim carpentry and remodeling far less disruptive to homeowners
- Low 12-amp draw reduces breaker trips when running on shared 15-amp household circuits
- Integrated roll cage and console protect critical components while supporting horizontal or vertical operation
- Dual quick couplers allow two trim carpenters to connect and work off a single compressor
Cons
- Bare-tool configuration means you must supply your own air hoses, couplers, and pneumatic nail guns
- At 36 pounds, it is heavier to haul up flights of stairs than ultra-compact 1-gallon finish compressors
- Air output of 3.0 SCFM is built for intermittent finish fastening and will not support continuous tools like rotary sanders or sprayers
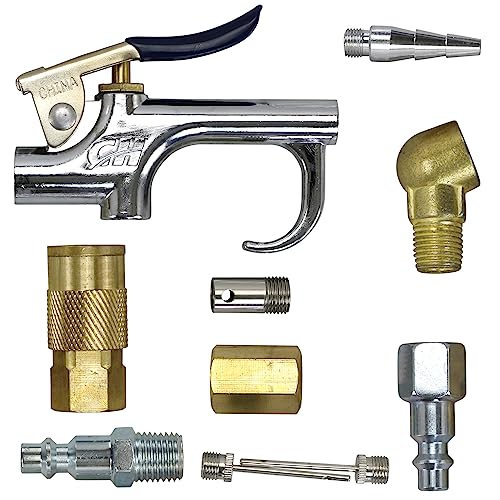
Harrier Hardware 11-Piece Air Compressor Starter
The Harrier Hardware 11-piece air compressor accessory kit provides essential pneumatic connections including a blow gun, tire chuck, and standard 1/4-inch NPT fittings. It is a practical starter set for garage DIYers and homeowners looking to handle basic inflation and shop cleanup tasks.
Pros
- Comprehensive 11-piece starter bundle covers basic inflation and workbench cleanup needs.
- Standard 1/4-inch NPT fitting compatibility connects easily with common workshop air hoses.
- Dedicated plastic storage container prevents losing small needles, inflator tips, and fittings.
- Cost-effective entry option for homeowners setting up a newly purchased air compressor.
Cons
- Supplies only one coupler and plug set, requiring extra fittings for multi-tool setups.
- Thread sealant or PTFE tape is not pre-applied and must be added to ensure leak-free connections.
- Designed for light DIY and garage duties rather than high-demand industrial production.
The Mechanics and Operation of Rotary Screw Air Compressors
Rotary screw air compressors generate pressurized air through positive displacement by trapping atmospheric air between two interlocking helical rotors. As an electric motor drives these synchronized screws, the pocket of trapped air travels along the length of the housing while its physical volume steadily decreases. This smooth, continuous movement delivers a steady stream of compressed air without the rhythmic pressure pulsations characteristic of reciprocating piston pumps. The entire mechanism is engineered to operate under continuous industrial workloads without requiring rest cycles to dissipate excess heat.
The Core Compression Principle: Intermeshing Helical Rotors
At the heart of every rotary screw pump lies an air end housing containing two precision-machined helical rotors known as the male and female rotors. The male rotor typically features convex lobes that mesh smoothly into the concave flutes of the female rotor. As these screws rotate in opposite directions within a close-tolerance casing, ambient air enters through the intake port and fills the expanding cavities between the lobes. As rotation continues, the inlet port is sealed off by the rotor lobes, trapping a fixed volume of air inside the flute chambers.
The helical profile forces the trapped air to travel axially along the length of the rotors toward the discharge end. Because the intermeshing geometry causes the space between the lobes and housing wall to diminish progressively, the air is mechanically compressed as it moves forward. By the time the air reaches the discharge port at the opposite end of the chamber, its volume has been substantially reduced, creating elevated working pressure. The continuous rotation ensures that as one pocket finishes discharge, another is already undergoing compression, providing an uninterrupted flow of pneumatic energy.
The Step-by-Step Rotary Screw Air Flow Cycle
The air compression process moves through four distinct physical phases, beginning with the initial intake cycle. During the intake phase, the compressor inlet valve opens, allowing ambient air to pass through a high-efficiency air intake filter to remove airborne dust and debris. The clean air fills the open flutes at the suction end of the rotating screws until the rotor teeth rotate past the housing edge. Once the lobes seal the intake cavity, the air is locked within the compression chamber for the next stage of movement.
During the compression phase, the trapped volume is pushed toward the discharge side, continuously shrinking in volume against the tightly machined housing walls. Friction and rapid molecular compaction generate significant thermal energy, which is managed depending on whether the system is oil-injected or oil-free. Once the compression reaches the predetermined internal pressure ratio, the discharge port is uncovered by the rotating rotor profile. The pressurized air discharges smoothly into downstream piping or an internal separator vessel, maintaining a stable flow rate without significant pressure drop.
The Vital Role of Compressor Oil in Lubricated Screw Systems
In oil-injected rotary screw compressors, specialized synthetic lubricant plays several essential roles inside the compression chamber. The fluid is injected directly into the air end while the rotors are spinning, forming a thin dynamic barrier between the male and female lobes. This liquid barrier seals the microscopic clearance gaps between the rotors and the housing, preventing compressed air from leaking back to the suction side. Without this hydraulic seal, internal air slippage would severely degrade the volumetric efficiency of the air end.
In addition to sealing, the circulating oil absorbs the immense heat created during the compression cycle. Air temperature would otherwise spike to dangerous levels, potentially distorting metal rotors or causing mechanical seizure. The lubricant also cushions the rotor bearings and gears, drastically minimizing friction and mechanical wear over thousands of operational hours. After leaving the discharge port, the mixture of compressed air and oil enters an air-oil separator tank, where centrifugal force and coalescing filters remove the lubricant so clean, pressurized air can travel downstream.
Oil-Injected Versus Oil-Free Rotary Screw Designs
Choosing between oil-injected and oil-free rotary screw mechanisms depends largely on the purity requirements of the pneumatic application. Oil-injected models represent the workhorse of industrial manufacturing, automotive repair shops, and heavy engineering facilities where standard air filtration suffices. These systems benefit from the cooling and sealing properties of synthetic oil, which allows for simpler single-stage rotor profiles operating at moderate internal temperatures. The presence of lubricant extends the operational lifespan of internal components, provided scheduled fluid and filter maintenance intervals are respected.
Oil-free rotary screw compressors are engineered for specialized sectors such as pharmaceutical manufacturing, food processing, and electronics assembly where even microscopic traces of oil vapor cannot be tolerated. Because no liquid sealant exists inside the air end, oil-free rotors must be manufactured with extreme precision and coated with specialized materials like Teflon or molybdenum. These units typically utilize two compression stages with intermediate air intercoolers to manage the intense thermal load without fluid cooling. While oil-free machines provide pristine air quality, they generally carry higher initial manufacturing costs and require precise operational oversight.
Rotary Screw Versus Reciprocating Piston Compressors
The operational differences between rotary screw and reciprocating piston compressors center around duty cycle capability and mechanical design. Conventional piston compressors, ranging from compact jobsite pancake units to two-stage shop pumps, utilize connecting rods and pistons moving up and down within cylinders. These reciprocating assemblies generate severe friction and heat, requiring a fifty to seventy percent duty cycle so the pump can cool down between run cycles. If a piston pump is forced to run continuously, the cylinder heads overheat, leading to accelerated valve fatigue and premature ring failure.
In contrast, rotary screw compressors are designed from the ground up for a one hundred percent continuous duty cycle. Because the rotating screws do not generate reciprocating inertia or stop-and-start friction, the air end runs smoothly without the intense heat buildup seen in piston heads. Furthermore, screw compressors operate at noticeably lower sound levels, often producing a steady hum rather than the concussive clatter of piston strikes. While compact portable piston compressors excel for intermittent punch-list work and trim nailing, stationary screw systems dominate continuous production facilities where air flow cannot pause.
Variable Speed Drive and Energy Efficiency in Modern Systems
Traditional fixed-speed screw compressors run their electric motors at a constant rotational speed, utilizing an inlet modulation valve or load-unload cycle to manage pressure. When compressed air demand drops, a fixed-speed unit unloads by closing its intake valve while the motor continues to spin at full RPM, wasting electrical power. Modern variable speed drive technology, often powered by advanced inverter systems, solves this efficiency bottleneck by altering motor RPM in real time. The compressor electronic controller monitors line pressure and adjusts motor output to match dynamic workshop consumption exactly.
Variable speed operation provides substantial electrical benefits, including low inrush current during startup through soft-start programming. High-horsepower three-phase motors can draw massive electrical surges on initial spin-up, potentially stressing shop electrical distribution systems. Inverter-driven screw compressors ramp up rotational speed gradually, eliminating sharp amperage spikes and protecting internal drive components. By eliminating unloaded idling and stabilizing working line pressure within a narrow margin, variable frequency technology drastically lowers overall energy consumption across variable-demand manufacturing shifts.
Essential Ancillary Systems: Pressure Controls, Separators, and Filtration
A rotary screw compressor relies on an integrated network of auxiliary components to deliver clean, dry, and regulated pneumatic energy. The air-oil separation vessel serves as the primary separation stage, using mechanical baffling and centrifugal action to drop bulk lubricant out of the air stream. The air then passes through a fine coalescing separator filter element that captures remaining microscopic oil droplets and returns them to the lubrication circuit via a scavenge line. A minimum pressure valve maintains adequate internal pressure inside the separator vessel to ensure oil circulation even when downstream piping is depressurized.
Downstream line regulation and pressure monitoring are equally critical to maintain system balance across the shop floor. Adjustable pressure controllers, switches, and electronic sensor displays monitor system pressure and dictate operational state transitions. Heavy-duty pipe manifolds, such as standard three-quarter-inch NPT outlets, allow massive volumes of compressed air to flow into storage receivers and downstream distribution piping without restrictive bottlenecks. Quality pressure switch assemblies and electronic monitoring modules ensure that the machine operates within safe working parameters, preventing over-pressurization while maintaining consistent system equilibrium.
Air Delivery and Pneumatic Tool Demand Matching
Understanding how screw compressors generate volume helps workshop operators match their machinery to demanding pneumatic tools. Air delivery volume, measured in cubic feet per minute at operating pressures like ninety to one hundred twenty PSI, determines how many tools can run concurrently. Intermittent pneumatic fasteners, such as finish nailers and staplers, consume small volumes of air and operate comfortably on portable small-tank units. However, continuous tools such as dual-action sanders, blast cabinets, and industrial CNC routers demand continuous high CFM flow that quickly empties small receiver tanks.
When air consumption exceeds compressor pump output, line pressure drops rapidly, causing production tools to stall or lose power mid-cycle. Rotary screw compressors provide the volumetric capacity needed to keep continuous industrial tools operating without pressure fluctuations. Because screw units produce high volume continuously, facilities can maintain smaller buffer tanks relative to their total CFM output compared to reciprocating setups. Matching your total shop air consumption to the sustained delivery curve of a rotary screw pump eliminates tool starvation and maximizes shop productivity.
Installation Prerequisites, Ventilation, and Electrical Setup
Proper facility preparation is necessary before commissioning any industrial rotary screw air compressor. Because these heavy-duty machines generate substantial thermal heat during continuous operation, the compressor room must offer generous clearance and active ventilation. Installing the unit in an unventilated closet or confined alcove will cause ambient temperatures to spike, triggering thermal overload safety shutoffs. Keeping the air compressor indoors away from severe moisture and dust accumulation protects sensitive electronic inverters and ensures uninterrupted airflow through cooling heat exchangers.
Electrical service planning is equally critical when installing high-output rotary screw equipment. Commercial units often demand three-phase electrical connections, such as two hundred eight to two hundred thirty-volt power, to supply continuous torque without drawing excessive amperage. Operators must verify that supply lines match manufacturer electrical phase specifications, as three-phase industrial motors cannot be operated on single-phase circuits via standard converters without severe power loss or equipment damage. Dedicated circuit breakers, proper wire gauges, and robust grounding safeguard internal motor windings against voltage dips during peak factory operation.
Routine Preventative Maintenance and Operational Verification
Maintaining a rotary screw compressor involves consistent inspection routines rather than frequent component overhauls. Operators should check the oil level sight glass before each operational shift and monitor air-oil separator pressure differentials to detect early filter restriction. Routine service intervals typically require changing the air intake filter, oil filter, and separator cartridge at designated running-hour milestones. Keeping the external radiator fins clean of dust and debris allows the cooling fan to dissipate oil heat efficiently, preserving lubricant viscosity and preventing premature fluid thermal breakdown.
Regular moisture management downstream from the compressor air end prevents corrosion across pneumatic distribution lines. While the screw mechanism discharges air smoothly, hot compressed air inevitably condenses moisture as it cools in receiver tanks and air piping. Daily purging through manual or automatic tank drain valves removes accumulated water before it can enter sensitive pneumatic tools, spray guns, or manufacturing machinery. Following manufacturer maintenance schedules and depressurizing line pressure fully before servicing fittings ensures safe, reliable pneumatic power for years of heavy-duty operation.
About the author
Tony Carrick is an experienced product researcher and writer specializing in tools, home improvement, automotive maintenance, and consumer equipment. With extensive experience reviewing tools and tackling hands-on renovation projects, he brings a buyer-focused perspective to compressor performance, usability, and overall value.