
Can I Put a Smaller Motor on My Air Compressor: Practical Guide for 2026
Learn if can i put a smaller motor on my air compressor is practical, how pulley ratios balance pump torque, and essential electrical rules in this October 2026 guide.
 By Tom Scalisi
Updated October 7, 2026

Tripping a 15-amp household circuit breaker during compressor startup remains one of the most frustrating experiences in a home garage. When an electric motor draws excessive inrush current or strains against high tank pressure, many workshop owners naturally wonder: can i put a smaller motor on my air compressor? Downsizing a motor seems like an intuitive way to reduce electrical demand and keep equipment running on standard household circuits without expensive panel upgrades. However, replacing an electric motor on a pneumatic system involves balancing mechanical torque, pump displacement, and operational resistance.
Before swapping hardware, it is critical to evaluate how motor horsepower directly influences pump speed, operating pressure, and delivered airflow. A smaller motor can struggle to overcome the mechanical resistance of a pressurized cylinder, risking thermal overload and sudden motor stall. Consulting an air tool tank sizing guide helps determine whether your tools can even function with the lower airflow that results from a smaller powerplant. Understanding the relationship between motor wattage, pump displacement, and storage volume is essential before loosening a single mounting bolt.
| Award | Product | ACR Score About ACR ScoreThe ACR Score is our own rating from 0 to 10, based on performance, design and build, ease of use, and value. It reflects independent research and is never influenced by manufacturers, retailers, or affiliate commissions. Learn more › | |
|---|---|---|---|
| Best Overall |
Baococo 4-Gallon 0.5 HP Air Compressor
|
9.2/10 | Buy |
| Best Budget |
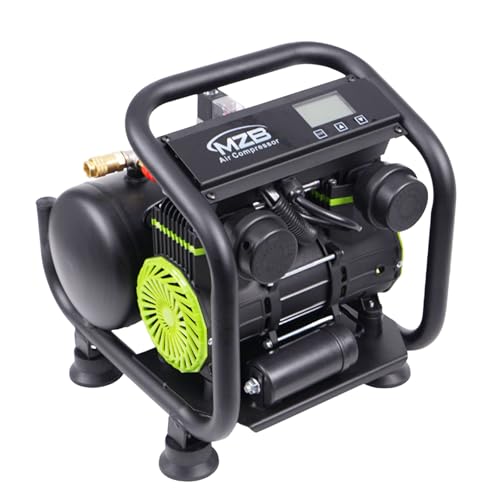 MZB MZB-900H-6 1.6-Gallon Air Compressor |
9.2/10 | Buy |
| Best Premium |
 HPDAVV 6.5HP 9-Gallon Gas Air Compressor |
9.2/10 | Buy |
 ZHSYMX 120 PSI 12V Air Compressor |
8.8/10 | Buy | |
 MZB MZB-1100H-50 13.2-Gallon Air Compressor |
8.8/10 | Buy | |
 GELUOXI 12V Twin On-Board Air Compressor |
8.8/10 | Buy | |
 MZB MZB-900H-24 6.4-Gallon Air Compressor |
8.6/10 | Buy | |
| Best Value |
 Baococo 8 Gallon Portable Air Compressor |
8.6/10 | Buy |
 VEVOR 2HP Oil-Free Air Compressor Motor |
8.4/10 | Buy | |
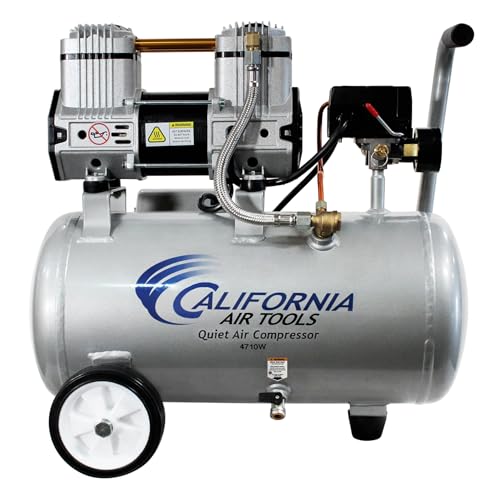 California Air Tools CAT-4710W 4.7-Gal Compressor |
8.3/10 | Buy |
Baococo 4-Gallon 0.5 HP Air Compressor
Built for light household maintenance and quick inflation tasks, this compact 4-gallon unit pairs a quiet 0.5 HP motor with an automatic overpressure safety shut-off. Its modest air delivery handles small nailers and tire filling without creating excessive workshop noise.
Pros
- Quiet operation suitable for residential spaces
- Automatic overpressure shut-off enhances operational safety
- Compact footprint stores easily in tight spaces
- Stable base minimizes movement during use
Cons
- Low airflow output limits heavy pneumatic tool use
- Maximum pressure capped at 110 PSI
- Modest 0.5 HP motor lacks heavy-duty capability
MZB MZB-900H-6 1.6-Gallon Air Compressor
Built for trim carpentry and light pneumatic tasks, this compact MZB unit pairs a 1.6-gallon steel tank with an oil-free pump. It produces up to 115 PSI while keeping operating sound around 70 decibels.
Pros
- Low-maintenance oil-free pump design
- Moderate 70 dB operating sound level
- Compact footprint is convenient to transport
- Sturdy steel air tank construction
Cons
- Small 1.6-gallon capacity limits continuous air tool runtimes
- Modest maximum output pressure of 115 PSI
HPDAVV 6.5HP 9-Gallon Gas Air Compressor
Built for remote job sites and mobile service trucks, this gas-powered unit delivers 12 CFM at up to 125 PSI using a durable cast iron pump. Its wheelbarrow frame and vehicle-mount capability make it a dependable workhorse for field mechanics and heavy air tools where electricity is unavailable.
Pros
- High 12 CFM airflow runs demanding pneumatic equipment
- Cast iron pump head provides long-term mechanical durability
- Wheelbarrow frame simplifies transport across rough job sites
- Truck-mountable base adds versatility for field service
Cons
- Max pressure tops out at 125 PSI
- Gasoline engine requires regular engine maintenance and outdoor venting
- Large footprint takes up substantial bed space in vehicles
ZHSYMX 120 PSI 12V Air Compressor
Built for onboard vehicle setups, this 12-volt compressor delivers up to 120 PSI with a 1.27 CFM flow rate for air horns, helper springs, and tire top-offs. Its sealed, permanently lubricated stainless steel cylinder ensures maintenance-free operation under harsh outdoor conditions.
Pros
- Permanently lubricated design requires zero ongoing maintenance
- Built-in thermal overload protection safeguards the 12V motor
- Durable, weather-sealed stainless steel cylinder construction
- Compact footprint fits tight vehicle underbody spaces
Cons
- Modest 1.27 CFM flow rate slows high-volume filling
- 120 PSI maximum pressure limits heavy-duty commercial applications
MZB MZB-1100H-50 13.2-Gallon Air Compressor
Designed for indoor workshops and residential garages, this compressor keeps operating noise down to a manageable 70 decibels. Its 13.2-gallon steel tank and wheeled frame suit DIY woodworkers, painters, and mechanics needing reliable airflow without regular pump maintenance.
Pros
- Quiet 70dB sound level ideal for indoor spaces
- Maintenance-free oil-free pump design
- Large 13.2-gallon durable steel tank
- Wheels and handle make transport manageable
Cons
- Hefty 72-pound weight makes vehicle loading difficult
- 115 PSI maximum pressure is modest for heavy-duty pneumatic tools
GELUOXI 12V Twin On-Board Air Compressor
Engineered as a 12-volt dual-motor on-board air system, this twin-cylinder compressor delivers up to 100 PSI for rapid vehicle tire inflation and pneumatic accessories. It is an ideal direct-replacement choice for overland enthusiasts, mobile repair techs, and truck owners seeking compact vehicle-mounted air power.
Pros
- Twin-cylinder dual 12V motor layout delivers high air volume relative to its compact size
- Water-sealed motor housings and internal thermal protection guard against dust, splashes, and heat on the trail
- High-grade internal rotating assembly utilizes ball bearings and European cylindrical roller bearings rather than basic bushings
- Manageable 20-pound weight and modular mounting profile fit easily into custom vehicle or overland setups
Cons
- Maximum cutoff pressure is rated at 100 PSI, which is below standard 150-PSI workshop systems and high-pressure commercial tires
- Requires a dedicated high-amperage 12V DC automotive wiring circuit rather than standard 120V household wall outlets
- Operates as a tankless compressor out of the box, requiring an auxiliary air tank if continuous-draw air tools are needed
MZB MZB-900H-24 6.4-Gallon Air Compressor
Delivering 5.65 CFM at 115 psi, this 1.2 HP oil-free unit rapidly pressurizes its 6.4-gallon tank in about one minute while maintaining a low 70-decibel noise output. It serves well for home garages and workshops handling nail guns, air tools, and light painting.
Pros
- Quiet 70 dB operating volume
- Fast tank recovery under 65 seconds
- Generous 5.65 CFM output at 115 psi
- Low-maintenance oil-free motor design
- Integrated wheels assist mobility
Cons
- Steel construction adds significant carrying weight
- Tank capacity limits continuous heavy spraying sessions
- Corded operation requires standard electrical outlet
Baococo 8 Gallon Portable Air Compressor
The Baococo 8-gallon portable air compressor pairs a 2HP electric motor with a 150 PSI receiver tank, delivering 2.8 SCFM at 90 PSI. It provides a solid, accessible air source for garage DIYers tackling tire inflation, car detailing, and pneumatic finish nailing.
Pros
- Useful 8-gallon tank capacity cushions air demand better than smaller pancake style compressors
- 150 PSI peak tank pressure accommodates common automotive tire inflators and pneumatic nailers
- Standard 120V 60Hz power compatibility allows easy plug-and-play use in residential garages
- Sufficient airflow rating of 2.8 SCFM at 90 PSI for light woodworking, trim carpentry, and cleaning tasks
Cons
- Continuous high-CFM pneumatic tools like rotary sanders and heavy-duty 1/2-inch impact wrenches will quickly deplete tank reserves
- Contradictory product listing notes an oil-free tank in the title while mentioning regular oil checks in the description, requiring users to inspect pump details before first start
- Does not include an air hose, quick-connect fittings, or downstream regulator accessories in the box
VEVOR 2HP Oil-Free Air Compressor Motor
Delivering 5.2 CFM at 90 PSI with a 1680 RPM motor, this oil-free VEVOR pump head provides clean, low-maintenance air output for garage shops and pneumatic tools. Its cold-rolled steel build and dedicated cooling fans make it a dependable drop-in motor for woodworking, spray painting, and automotive repairs.
Pros
- Low-maintenance oil-free operation
- Generates 5.2 CFM at 90 PSI
- Sturdy steel and aluminum construction
- Effective cooling via built-in fans and heat sinks
Cons
- Heavier unit at over 36 pounds to install
- Single-stage design limits peak pressure to 145 PSI
- At 78 dB, operating volume is still noticeable indoors
California Air Tools CAT-4710W 4.7-Gal Compressor
Built for garage workshops and DIY tasks, this mobile unit features an oil-free dual-piston pump that fills its 4.7-gallon steel tank in 78 seconds. Its low 7.5-amp motor draw ensures smooth startups on standard household circuits without tripping breakers.
Pros
- Fast 78-second tank fill time from empty
- Low 7.5-amp draw prevents tripped breakers
- Low-maintenance oil-free pump operation
- Wheels and pull handle ease transport at 35 pounds
Cons
- Delivers only 2.2 CFM at 90 PSI for demanding tools
- Steel tank construction is heavier than aluminum alternatives
Engineering Realities of Changing Air Compressor Motor Sizes
The short technical answer is yes, you can technically put a smaller motor on an air compressor, but only under specific mechanical conditions. Doing so successfully requires recalculating pulley ratios, reducing pump rotational speed, or lowering maximum cut-out pressure to match the reduced motor torque. Simply bolting a lower-horsepower motor to an existing pump with identical pulleys will lead to motor stalling, tripped thermal overload protectors, and potential winding damage. To understand why, you must examine how pneumatic pumps generate resistance against electric motors.
The Mechanical Physics: Torque Demand and Operating Pressure
Air compressor pumps do not present a constant load to their drive motors throughout the compression cycle. When an empty storage tank begins to fill from zero pressure, the electric motor experiences minimal resistance because atmospheric air easily passes through intake reed valves. As storage tank pressure climbs toward cut-out thresholds of 125 PSI or 150 PSI, the piston faces escalating counter-pressure on every compression stroke. This climbing pressure demands peak mechanical torque from the motor right before the pressure switch disengages.
A motor rated at lower running horsepower produces proportionally less starting and running torque. If a heavy cast-iron pump requires three horsepower of continuous mechanical force to push air into a 150 PSI tank, a two-horsepower motor simply will not have the rotational torque to complete the cycle. The motor will slow down, draw excessive amperage from the electrical supply, generate severe internal heat, and trip its internal thermal reset. Understanding the difference between misleading peak horsepower marketing claims and true continuous running horsepower is the first step in diagnosing feasibility.
Direct-Drive Versus Belt-Drive Pump Architectures
The physical layout of your air compressor determines whether downsizing a motor is even physically possible. Direct-drive air compressors, such as compact oil-free units or low-noise consumer models, integrate the motor shaft directly into the pump eccentric journal. On these machines, including typical portable models from brands like Baococo or California Air Tools, the motor and pump share an integrated housing. You cannot replace the motor independently because there is no separate drive shaft, belt, or modular mounting plate.
In contrast, stationary workshop compressors and industrial portable units utilize belt-drive architectures where a standalone electric motor connects to a cast-iron pump via V-belts and pulleys. These modular systems permit motor replacements because the motor is an independent component bolted to a universal baseplate. On belt-driven setups, you have the flexibility to alter drive pulley diameters and adjust center-to-center distances. If your compressor is a direct-drive design, replacing the powerplant requires replacing the entire pump and motor assembly together.
Compensating With Pulley Ratios and Pump Speed Reduction
To safely operate a smaller motor on a belt-drive pump, you must reduce the mechanical load placed on the motor shaft. The standard engineering solution is installing a smaller drive pulley on the motor shaft to lower the pump rotational speed. Electric motor speed remains fixed by electrical line frequency, typically operating at 1,725 RPM or 3,450 RPM on standard 60 Hz alternating current. By changing the ratio between the motor drive pulley and the pump flywheel pulley, you trade pump rotational speed for mechanical advantage.
When you slow down the pump, the motor gains the torque leverage needed to push pistons against full tank pressure without stalling. However, this mechanical advantage comes with a direct performance penalty in delivered air volume. Piston displacement per minute drops in direct proportion to pump rotational speed, reducing delivered cubic feet per minute (CFM) at both 40 PSI and 90 PSI. If you downsize a motor by one-third, your compressor will deliver approximately one-third less airflow, dramatically increasing recovery time between cycles.
Electrical Constraints: Breaker Tripping and Inrush Current
The primary reason workshop owners seek smaller motors is avoiding electrical circuit overloads on standard 15-amp or 20-amp residential circuits. Large stationary compressors often require dedicated 240V circuits pulling significant running amperage and substantial startup inrush current. An induction motor under heavy startup load can draw up to five to seven times its continuous rated current during the initial fraction of a second when rotor inertia is overcome. If a garage circuit supplies lighting and other tools simultaneously, the compressor immediately trips the breaker.
Swapping to a motor with lower continuous amperage draw can solve breaker tripping issues during startup, provided the pump is properly re-geared. A smaller capacitor-start motor drawing 12 amps to 14 amps runs reliably on a standard 120V 20-amp branch circuit where a larger motor would fail. However, if the smaller motor is overloaded due to incorrect pulley sizing, it will run continuously above its rated full-load amperage. In that scenario, the smaller motor will trip circuit breakers just as frequently as the larger unit while running the risk of permanent insulation failure.
Pressure Switch Calibration and Maximum PSI Adjustments
Another method to accommodate a smaller motor is reducing the maximum operating pressure of the storage tank. Torque demand on an air compressor pump peaks at maximum cut-out pressure, meaning the final 20 PSI of compression requires the most power. If a pump was engineered to fill a reservoir to 150 PSI, adjusting the pressure switch to cut out at 115 PSI substantially lowers peak torque requirements. This pressure drop allows a smaller motor to complete the cycle without stalling near the end of the stroke.
While lowering cut-out pressure makes motor downsizing easier, it reduces the usable volume of stored compressed air. When comparing single-stage and two-stage pump systems, multi-stage units depend on high pressure to store energy efficiently in compact reservoirs. A lower cut-out threshold means your air tools will consume the stored buffer much faster, forcing the compressor to start cycling sooner. If your pneumatic tools require continuous 90 PSI line pressure, dropping maximum tank pressure leaves very little margin for regulator stability.
Cooling Efficiency and Duty Cycle Vulnerabilities
Electric motors and compressor pumps rely on forced-air cooling to dissipate the immense heat generated during gas compression. On belt-driven systems, the pump flywheel features integrated fan blades designed to blow ambient air across cooling fins at a specific design RPM. When you install a smaller motor and reduce pump speed through pulley modifications, airflow across the cylinder heads drops significantly. This reduction in cooling efficiency occurs precisely when the compressor must run longer cycles to deliver the same volume of air.
Extended runtimes combined with reduced cooling airflow can quickly push equipment past its rated duty cycle limits. Most consumer and workshop air compressors feature intermittent duty cycles, typically around 50% to 70%, requiring rest intervals between pumping cycles. If a downsized motor forces a pump to run for twenty consecutive minutes to fill an empty tank, cylinder temperatures escalate rapidly. Excessive heat breaks down lubricating oil, accelerates carbon buildup on valve plates, and risks thermal breakdown inside motor windings.
Modular Replacement Assemblies as Practical Alternatives
Rather than attempting complex pulley and bracket modifications on an existing pump, replacing the entire motor and pump head assembly often proves more practical. Manufacturers like VEVOR produce matched, oil-free replacement assemblies rated for specific horsepower and CFM levels that bolt directly onto existing air tanks. These integrated pump-motor combinations eliminate pulley calculations and guarantee proper alignment between mechanical displacement and electrical power. Matching a factory-engineered assembly ensures optimal valve sizing and built-in thermal protection.
For users seeking low-noise performance or specific portability benefits, standalone compressors from brands such as MZB or California Air Tools offer complete solutions designed around quiet dual-piston technology. These units operate on modest electrical current while maintaining quiet noise levels around 70 to 75 decibels. If you frequently handle vehicle tires, train horns, or air suspension setups, specialized compact 12V onboard units from brands like GELUOXI or ZHSYMX provide dedicated performance without modifying stationary shop equipment. When heavy pneumatic airflow is needed in remote locations without electrical access, gas-powered wheelbarrow compressors from brands like HPDAVV bypass electrical limitations entirely.
Mechanical Installation Checks: Shafts, Brackets, and Rotation
If you proceed with installing a smaller motor on a belt-drive system, mechanical fitment requires rigorous verification. Electric motors feature standardized NEMA frame sizes that dictate foot mounting hole spacing, shaft centerline height, and shaft diameter. A smaller motor often features a smaller frame size, meaning its mounting bolt pattern will not align with existing baseplate slots without an adapter plate. Furthermore, a smaller shaft diameter requires purchasing a new motor pulley with matching bore and keyway dimensions.
Rotational direction is another critical factor that can destroy equipment if overlooked during wiring. Compressor flywheels are designed to spin in one specific direction to direct cooling air across the pump cylinders and intercoolers. Many industrial electric motors can rotate either clockwise or counter-clockwise depending on how internal capacitor leads are connected. Reversing motor rotation starves cylinder heads of airflow and can cause splash-lubricated pumps to suffer oil starvation, leading to premature mechanical failure.
Valve Operation and Storage Safety Considerations
Any alteration to motor size or pump operation requires careful inspection of the pneumatic safety components. The unloader valve must function flawlessly to vent residual head pressure when the motor stops, allowing a lower-torque motor to start without counter-pressure. If the unloader valve or tank check valve fails, trapped air against the piston crown will prevent a smaller motor from rotating, instantly popping breakers. Depressurizing the tank completely and checking safety relief valve rings are mandatory procedures before energizing any modified drive system.
Proper maintenance habits remain essential regardless of motor size, especially regarding moisture management inside the pressure vessel. Condensation naturally collects at the bottom of the tank during every compression cycle, making regular purging through drain valves vital to prevent rust. Understanding the implications of storing compressed air in the tank ensures long-term tank integrity and reliable regulator operation. Always verify that pressure switches, relief valves, and belt guards remain securely installed before returning modified equipment to daily workshop service.
Downsizing an air compressor motor is an engineering compromise that trades air delivery volume for lower electrical demand. While mechanically feasible on belt-driven compressors through calculated pulley adjustments and reduced cut-out pressure, it reduces delivered CFM and lengthens recovery cycles. Direct-drive compressors cannot accommodate smaller motors due to integrated shafts, making full assembly replacement the only sensible path. By carefully evaluating torque requirements, thermal duty cycles, and pneumatic safety components, you can make an informed choice that keeps your workshop running safely and efficiently.
About the author
Tom Scalisi brings more than two decades of experience in construction, building maintenance, contracting, and hands-on tool use. His practical understanding of power tools, automotive work, repairs, and jobsite equipment helps readers evaluate compressors based on real workloads rather than specifications alone.