
How to Figure Cfm of Air Compressor: Practical Guide for 2026
Learn how to figure cfm of air compressor tanks and pumps accurately to match pneumatic tools and prevent pressure drops in October 2026.
 By Glenda Taylor
Updated October 8, 2026

Running air-demanding pneumatic tools without stalling or suffering sudden line pressure drops depends entirely on your pump delivering adequate airflow under load. Many DIYers and workshop mechanics struggle when rotary sanders, paint sprayers, or impact wrenches bog down because they do not know how to figure cfm of air compressor equipment before starting a demanding job. Cubic feet per minute represents the actual volume of air your pump delivers to an air line at a specific operating pressure, making it the most critical metric for tool performance.
Determining accurate air delivery requires looking past misleading marketing figures like peak surge horsepower and focusing on delivered CFM @ 90 PSI. Whether you need to calculate output through a manual tank pump-up test or estimate pump capacity from verified motor specifications, understanding these calculations ensures your workshop operates efficiently. This guide explains the exact formulas, mechanical considerations, and tool-matching rules required to evaluate compressed air delivery with confidence.
| Award | Product | ACR Score About ACR ScoreThe ACR Score is our own rating from 0 to 10, based on performance, design and build, ease of use, and value. It reflects independent research and is never influenced by manufacturers, retailers, or affiliate commissions. Learn more › | |
|---|---|---|---|
| Best Overall |
Eastwood Elite QST 30/60 Scroll Air Compressor
|
8.9/10 | Buy |
| Best Budget |
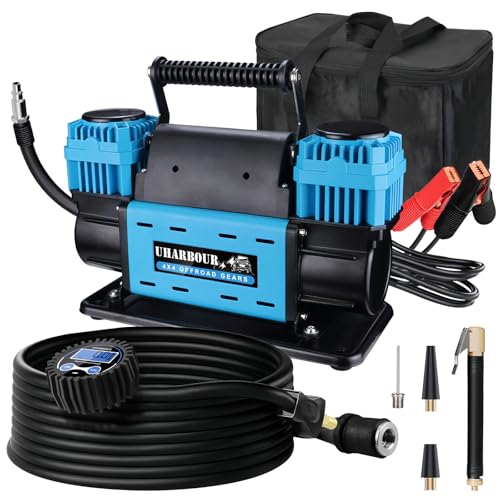 Uharbour 12V 12.35 CFM Offroad Air Compressor |
8.6/10 | Buy |
| Best Value |
 MZB 13.2 Gallon Ultra Quiet Air Compressor |
8.6/10 | Buy |
 Stealth 12 Gallon Ultra Quiet Air Compressor |
8.4/10 | Buy | |
 OwnMy 2 Set Air Compressor Silencer with 6 Air |
8.3/10 | Buy | |
 PointZero 1/5 HP Airbrush Compressor with Air |
8.3/10 | Buy | |
 FORNAX 8 Gallon Air Compressor, 1HP 2.2 CFM |
8.0/10 | Buy | |
 BUNKER INDUST 12V Air Compressor |
8.0/10 | Buy | |
| Best Premium |
 CSI Accessories AIR8260 Portable Twin Air |
8.0/10 | Buy |
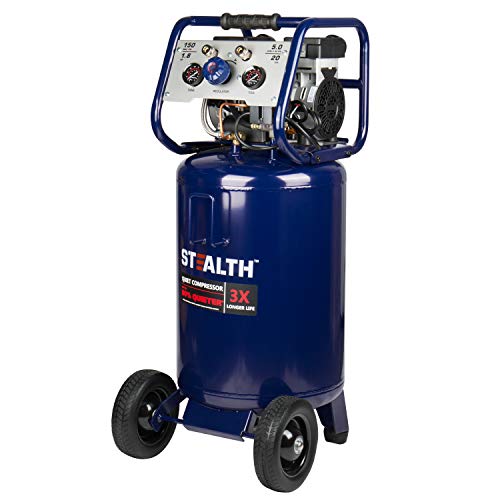 Stealth 20 Gallon Ultra Quiet Air Compressor,1.8 |
7.8/10 | Buy |
How to Calculate, Measure, and Verify Air Compressor CFM Output
Figuring the true air output of a pneumatic system requires looking beyond general pump labels and calculating actual air volume delivered under working pressure. Many compressor owners discover that factory specifications reflect ideal conditions or unpressurized free air displacement rather than sustained volume at working tool pressures. By using straightforward timing formulas, evaluating motor power, and accounting for pneumatic friction, you can determine exactly what your compressor delivers and whether it can handle your pneumatic tools.
Understanding Air Delivery Metrics: CFM, SCFM, and Pressure Thresholds
Pneumatic air volume is commonly expressed in cubic feet per minute, but this single number can represent very different operating conditions. Standard cubic feet per minute, or SCFM, measures air delivery corrected to standardized atmospheric conditions of 14.7 pounds per square inch absolute, 68 degrees Fahrenheit, and 36 percent relative humidity. Because air contracts under pressure and expands with ambient heat, unpressurized free air displacement will always show a higher numeric value than pressurized delivered air.
Evaluating usable air flow requires checking the delivery volume at specific operating pressures, most notably at 90 PSI and 40 PSI. Most heavy pneumatic shop tools such as impact wrenches, framing nailers, and die grinders require roughly 90 PSI to function at full rated power. Delicate equipment like touch-up paint guns and airbrushes operate closer to 40 PSI, where air pumps naturally move more volume because the pistons encounter less counter-pressure inside the storage vessel.
Looking at manufacturer ratings demonstrates how pressure alters delivery rates. A typical shop unit like the Stealth 12 Gallon Ultra Quiet Air Compressor delivers 5 CFM @ 40 PSI, but its output drops to 4 CFM @ 90 PSI as cylinder back-pressure rises. If a compressor specification only states a single CFM number without specifying the corresponding PSI, that rating often reflects unpressurized displacement rather than working air delivery.
The Tank Fill-Up Formula: Calculating Real-World Pump Output
Measuring the actual air output of your compressor at home or in your workshop requires a simple stopwatch and basic arithmetic using your tank storage capacity. This physical timing method bypasses marketing claims and reveals the exact performance of your pump assembly. Before starting the test, ensure that all line drain valves, air chucks, and regulator petcocks are completely shut to eliminate hidden pneumatic leaks.
To begin the measurement process, drain the storage tank until your line pressure gauge reads zero PSI, then close the drain valve securely. Start your compressor while simultaneously starting your stopwatch, timing how many seconds the pump takes to fill the tank to its automatic cut-out shutoff pressure. Record the tank volume in gallons, the final cut-out pressure in PSI, and the total elapsed time in seconds.
The mathematical calculation converts the tank volume into cubic feet and determines how many atmospheric volumes the pump displaced over time. First, divide your tank capacity in gallons by 7.48 to convert liquid gallons into cubic feet of volume. Next, divide the change in gauge pressure by 14.7, which represents one standard atmosphere of pressure at sea level. Finally, multiply the tank volume in cubic feet by the atmospheric pressure ratio, multiply that result by 60, and divide by the total fill time in seconds.
Applying this formula to an actual workshop example clarifies the mathematics. Suppose you test an 8-gallon unit such as the FORNAX 8 Gallon Air Compressor, which charges from zero to a maximum cut-out pressure of 125 PSI in roughly 90 seconds. Converting 8 gallons yields roughly 1.07 cubic feet, while dividing 125 PSI by 14.7 equals approximately 8.5 atmospheres. Multiplying 1.07 by 8.5 produces 9.1 cubic feet of compressed air, and multiplying by 60 before dividing by 90 seconds reveals an average delivery rate of approximately 6.07 CFM across that full zero-to-cut-off cycle.
Measuring Output Between Cut-In and Cut-Out Pressure Cycles
While a full fill from zero PSI provides a general snapshot of pump health, measuring between cut-in and cut-out pressures yields a far more practical figure for tool operation. Compressors rarely pump from an empty tank during everyday shop tasks because the automatic pressure switch cycles the motor on when tank pressure drops to its cut-in threshold. Pumping against high existing tank pressure requires more mechanical effort and reduces the volumetric efficiency of the pump cylinders.
To run a cut-in to cut-out test, allow the compressor to charge fully until the motor shuts off, then slowly bleed air using a blow gun until the pressure switch triggers motor restart. Start your stopwatch the exact moment the motor restarts at cut-in pressure, then stop timing when the motor reaches full cut-out pressure and shuts off. Note both the cut-in pressure and cut-out pressure along with the elapsed time in seconds.
Calculating output across this working band uses the exact same physical formula, but you substitute the difference between cut-out and cut-in pressure into the equation. For example, if a pressure switch restarts the motor at 90 PSI and shuts off at 120 PSI, your pressure delta is 30 PSI rather than the full tank rating. Dividing 30 PSI by 14.7 yields roughly 2.04 atmospheres, which reflects the true mechanical delivery under heavy continuous tool load.
Estimating Air Delivery from True Motor Horsepower
When physical tank testing is impractical before buying a compressor, motor horsepower provides a dependable guideline for estimating delivered airflow. In standard single-stage electric air compressors running on 120-volt circuits, an efficient pump produces approximately 3 to 4 CFM @ 90 PSI for every true continuous running horsepower. This ratio is governed by basic electrical and mechanical power limits, meaning single-phase household power cannot produce unlimited air output.
Evaluating specifications from verified units demonstrates this mechanical relationship. The Stealth 20 Gallon Ultra Quiet Air Compressor features a 1.8 HP motor and delivers 5 CFM @ 90 PSI, which aligns closely with the expected 3.5 CFM per horsepower baseline. In contrast, heavy shop equipment like the Eastwood Elite QST 30/60 Scroll Air Compressor utilizes a 4 HP motor to produce 12.7 CFM @ 90 PSI, maintaining that exact same engineering proportion while delivering industrial air volume.
Consumers must remain cautious regarding exaggerated peak surge horsepower ratings frequently printed on retail product boxes. Peak horsepower refers only to the brief electrical surge drawn as the motor starts turning against inertia, not continuous working power. If a compact portable compressor claims 5 peak horsepower while plugging into a standard 15-amp household outlet, its true running horsepower is usually closer to 1.5 HP, which cannot deliver more than 4 to 5 CFM @ 90 PSI without violating physical electrical limits.
Sizing Compressor Output Against Pneumatic Tool Demand
Figuring your compressor CFM output is only half of the equation; you must also evaluate the air volume consumed by your specific pneumatic tools. Air tools divide into two distinct operational categories: intermittent-draw tools and continuous-draw tools. Intermittent tools such as brad nailers, finish nailers, and framing staplers consume a brief burst of air per fastener, typically requiring less than 1 to 2 CFM to operate reliably.
Continuous-draw equipment such as dual-action rotary sanders, die grinders, needle scalers, and HVLP paint spray guns draw massive volumes of pressurized air uninterruptedly. A standard HVLP spray gun or rotary sander frequently demands between 8 and 14 CFM @ 90 PSI during steady operation. If your air compressor pump only delivers 4 CFM @ 90 PSI, the tool will rapidly exhaust the tank reserve, forcing the pressure to plummet and causing the tool to stall mid-job.
When matching tool consumption to compressor delivery, practical workshop practice recommends applying a 1.25 to 1.5 safety multiplier to the tool demand rating. If your highest-demand tool lists an average air requirement of 6 CFM, you should target a compressor capable of supplying at least 7.5 to 9 CFM @ 90 PSI. This buffer accommodates normal duty cycle rests, prevents continuous motor overheating, and accounts for slight pressure drop across air lines and quick-connect fittings.
The Role of Storage Tank Capacity Versus Pump Delivery
A widespread misconception among workshop owners is that purchasing a larger air tank will solve inadequate pump CFM delivery. A large storage tank acts solely as an air accumulator or pneumatic buffer, storing pressurized air for temporary spikes in tool demand. While a 20-gallon or 30-gallon tank allows you to operate a high-draw tool for a short burst, it cannot sustain continuous operation if the pump output does not match tool consumption.
Small reserve vessels such as the 1-gallon tank on the CSI Accessories AIR8260 Portable Twin Air Compressor or the 0.8-gallon tank on the PointZero 1/5 HP Airbrush Compressor work exceptionally well for low-demand, highly portable tasks. These compact tanks stabilize air pressure pulses and allow sensitive tools like airbrushes or tire inflators to operate smoothly. However, once the initial tank reserve is depleted, the tool is entirely dependent on the continuous displacement of the pump assembly.
When running high-volume tools on undersized pumps, a large tank merely delays the inevitable pressure drop while significantly extending recovery time. A pump producing only 3 CFM will take several minutes to recharge a 20-gallon tank back to cut-out pressure once emptied. For continuous sanding, cutting, or media blasting, true pump CFM delivery at 90 PSI matters far more than overall tank gallon capacity.
Mechanical Factors Causing CFM Drops and Flow Restrictions
If your pump-up test indicates that your compressor is delivering significantly less CFM than its original manufacturer rating, several mechanical issues may be restricting output. Air intake restrictions represent one of the most common yet overlooked causes of reduced volumetric efficiency. Clean intake filters and quality silencers, such as those found in the OwnMy 2 Set Air Compressor Silencer with 6 Air Compressor Intake Filters kit, allow unrestricted atmospheric air into the compression chamber while filtering harmful shop dust.
Worn internal components in the pump head also degrade output pressure over time. In oil-free compressor designs, Teflon piston rings and cylinder sleeves gradually wear down, allowing pressurized air to slip past the piston during the compression stroke. Similarly, in cast-iron or scroll compressors, carbonized reed valves or failing disc check valves prevent complete sealing, forcing the pump to recompress the same air repeatedly and drastically extending fill times.
Downstream restrictions can also create the illusion of inadequate pump CFM even when the pump is operating at peak mechanical efficiency. Undersized air hoses with a 1/4-inch internal diameter choke high-flow tools over long distances, causing severe dynamic pressure drops. Upgrading to a 3/8-inch internal diameter hose, cleaning inline regulator diaphragms, and inspecting quick-connect couplers ensures that the full CFM delivered by the compressor actually reaches your pneumatic tools.
Duty Cycles and Thermal Management During High Air Demand
Compressor output figures must always be interpreted alongside the manufacturer rated duty cycle of the machine. The duty cycle represents the percentage of time a compressor pump can safely run within a standard ten-minute operating window without overheating or suffering accelerated component wear. Many consumer-grade oil-free compressors feature a 50 percent duty cycle rating, meaning the pump should only run for five minutes out of every ten minutes under load.
Operating a low-CFM compressor continuously on heavy air tools quickly exceeds rated duty cycle thresholds, generating extreme cylinder heat. Excessive operating temperatures break down lubrication on oil-lubricated pumps and degrade sealing rings on oil-free units, ultimately triggering internal thermal overload switches. Industrial designs like the Eastwood Elite QST 30/60 Scroll Air Compressor feature a 100 percent continuous duty cycle, allowing non-stop operation for demanding automotive restoration and production environments.
To preserve pump longevity and maintain consistent CFM delivery, you should never select a compressor that must operate at 100 percent of its capacity to meet minimum tool needs. Allowing the pump to cycle naturally between cut-in and cut-out thresholds dissipates heat, reduces internal moisture condensation, and extends the operational lifespan of motor windings and valve plates.
Essential Maintenance to Preserve True CFM Delivery
Maintaining consistent air volume delivery over years of workshop use requires regular preventative maintenance routines. Daily moisture drainage represents the most critical task for preserving effective storage capacity and preventing internal vessel rust. Atmospheric air naturally contains humidity that condenses into liquid water under compression, accumulating at the bottom of the tank and robbing valuable air storage space if left unpurged.
Periodically inspecting intake silencer elements and replacing clogged paper filter media ensures that your compressor draws maximum air volume without creating vacuum resistance. Furthermore, checking the safety relief valve and testing the unloader valve after motor shutdown prevents trapped head pressure, which strains electric motors during startup and causes unnecessary circuit breaker tripping.
Calculating and verifying your compressor CFM empowers you to make informed decisions about your workshop equipment and pneumatic workflow. By measuring tank pump-up cycles, respecting continuous horsepower limits, and maintaining clean intake filtration, you can ensure your pneumatic tools always receive the clean, pressurized air volume required to get the job done right.
About the author
Glenda Taylor has extensive experience in residential construction, remodeling, home improvement, and tool use. Her practical approach to equipment evaluation focuses on usability, performance, safety, and value—helping DIYers and workshop users make better-informed decisions about compressors and related tools.