
Can You Use Compressor Oil in Air Tools: A Practical Guide for 2026
Wondering can you use compressor oil in air tools? Learn how viscosity affects pneumatic performance and proper tool care for October 2026.
 By Glenda Taylor
Updated October 8, 2026
Pneumatic motors rely on clean airflow and low-viscosity lubrication to spin high-speed rotors and cycle reciprocating strike mechanisms without hesitation. When operators find an empty bottle on the workbench, the immediate question is whether can you use compressor oil in air tools without causing internal component damage. While both liquids serve compressed air machinery, air compressor pump oil is formulated specifically for high-temperature crankcases rather than the sensitive internal vanes of pneumatic equipment. Exploring suitable air compressor oil alternatives helps clarify how fluid properties differ between pump sumps and air motors.
Pouring heavy pump lubricant directly into a pneumatic intake often leads to sluggish motor cycling, sticky trigger valves, and gummed exhaust ports. True pneumatic oils feature lightweight viscosities alongside specialized emulsifiers that trap moisture and protect rubber O-rings during rapid decompression. Understanding the distinct mechanical demands of each fluid ensures your tools maintain peak torque while preventing costly shop downtime. Proper fluid selection keeps internal motor vanes spinning freely and protects vital internal seals across demanding daily shop tasks.
| Award | Product | ACR Score About ACR ScoreThe ACR Score is our own rating from 0 to 10, based on performance, design and build, ease of use, and value. It reflects independent research and is never influenced by manufacturers, retailers, or affiliate commissions. Learn more › | |
|---|---|---|---|
| Best Overall |
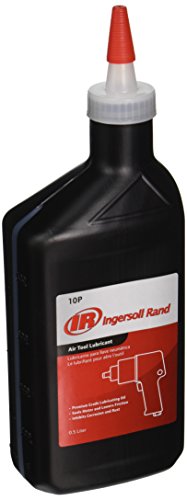
Ingersoll Rand 10P Edge Series Premium Air Tool
|
9.2/10 | Buy |
| Best Premium |
 TRIAX Kompressor ISO 46 SAE 20, Full Synthetic |
9.1/10 | Buy |
| Best Value |
 Marvel Air Tool Oil 4 oz Bottles |
8.9/10 | Buy |
 1/4" Mini LUBRICATOR air in line OILER compressed |
8.9/10 | Buy | |
 Lucas Oil 10216 Air Tool Lubricant & Tool Box |
8.8/10 | Buy | |
| Best Budget |
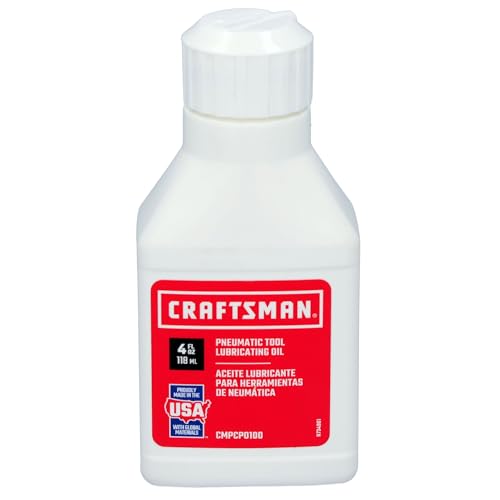 CRAFTSMAN Air Tool Oil, Pneumatic Tool Oil |
8.6/10 | Buy |
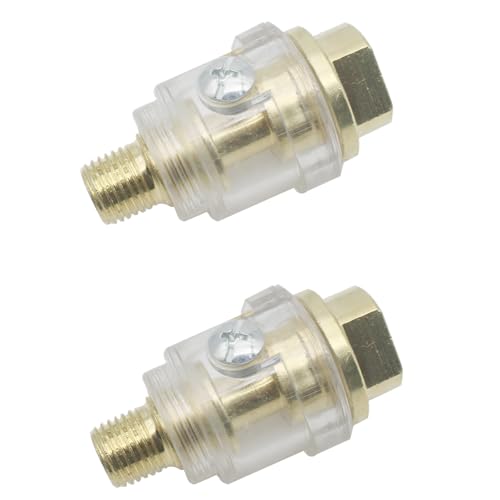 OZXNO 2 Pcs Automatic Mini |
8.6/10 | Buy | |
 Milton Industries High Performance Air Tool Oil |
8.4/10 | Buy | |
 Freeman PTTO Air Tool Oil, 8 oz. |
8.3/10 | Buy | |
 NEIKO 30252A Water and Oil Separator for Air Line |
8.3/10 | Buy |
The Mechanical Reality of Using Compressor Oil in Pneumatic Air Tools
Compressor crankcase oil and dedicated pneumatic air tool oil serve two entirely different mechanical purposes in a workshop. While a pump oil protects heavy crankshafts and pistons operating under high thermal friction, air tools require an ultra-light oil that mists easily at room temperature. Using compressor oil inside pneumatic tools is strongly discouraged because the heavier fluid creates severe mechanical drag and attracts airborne debris. The direct result of using thick pump fluid is sluggish tool startup, reduced output power, and eventual valve gumming.
Direct Comparison: Pump Lubrication Versus Air Motor Requirements
Air compressor pumps generate significant heat as atmospheric air compresses into high-pressure storage tanks. The crankcase oil inside reciprocating pumps, such as industrial ISO 46 or ISO 68 formulations, relies on thermal stability to prevent fluid thinning and vapor burnoff at elevated temperatures. A heavy fluid film creates a cushion between cast-iron cylinders, wrist pins, and bearings rotating under sustained mechanical load. These formulations remain inside a sealed crankcase where external moisture exposure is minimal and temperatures routinely exceed normal ambient room levels.
Pneumatic tools experience the inverse thermodynamic environment during daily operation. Compressed air cools dramatically as it expands through motor vanes, cylinder chambers, and exhaust ports. A fluid inside a pneumatic impact wrench or die grinder must flow instantly in cool conditions without requiring a warm-up cycle. Dedicated pneumatic lubricants maintain fluid mobility at ambient and refrigerated temperatures, ensuring immediate response the moment an operator depresses the trigger valve.
The mechanical velocity of pneumatic tools also dictates lubrication requirements. A standard air grinder or rotary sander can spin at speeds exceeding twenty thousand revolutions per minute. Thick compressor oil creates intense fluid friction against rapid vane movement, effectively acting like a hydraulic brake inside the motor chamber. Lightweight pneumatic oils provide boundary lubrication across delicate cylinder walls without robbing the motor of air-driven rotational velocity.
Viscosity Ratings and Kinematic Resistance
Kinematic viscosity represents the primary technical difference between pump oil and pneumatic lubricant. Air tool oils typically register at ISO 22 or ISO 32, which roughly corresponds to an ultra-light SAE 5W or SAE 10W rating. In contrast, standard reciprocating compressor oils feature ISO 68 or ISO 100 viscosities, comparable to non-detergent SAE 30 motor oil. Some synthetic multi-viscosity compressor fluids reach ISO 46, but even these remain significantly heavier than standard air tool oils like Milton Industries High Performance Air Tool Oil.
Higher viscosity oils resist the atomization process required to coat interior pneumatic surfaces evenly. Dedicated air tool lubricants are designed to break into a fine mist when compressed air rushes through the tool inlet bushing. This atomization ensures that microscopic oil droplets reach rear rotor bearings, front cylinder plates, and sliding composite motor vanes simultaneously. A thick compressor fluid drops straight to the bottom of the air chamber instead of atomizing, leaving upper contact surfaces completely unprotected.
The added drag from heavy oil directly impairs high-torque tools during challenging fastening jobs. When matching pneumatic equipment for automotive service, our guide on air compressor sizing for impact wrenches explains how volume delivery directly influences torque performance. Introducing viscous pump oil into an impact gun mechanism creates internal resistance that robs air volume before kinetic energy reaches the anvil. Maintaining proper fluid viscosity ensures your compressor output translates into clean mechanical force at the drive socket.
Additive Packages, Emulsifiers, and Seal Degradation
The chemical additives blended into pneumatic oils address unique contamination risks that compressor pump oils never encounter. Air tool oils incorporate specialized detergent additives and anti-gumming agents that break down varnish and dissolve sludgy deposits. Products like Marvel Air Tool Oil specifically focus on dissolving old gummy buildup to restore free vane travel inside pneumatic motors. Crankcase pump oils lack these aggressive solvent properties because crankcases operate in closed environments designed to avoid deposit agitation.
Moisture control represents another crucial chemical distinction between these specialized fluids. Compressing ambient air forces water vapor out of suspension, delivering microscopic water droplets directly through delivery hoses to the tool inlet. Dedicated pneumatic lubricants contain emulsifiers that bind with incoming moisture, neutralizing its corrosive potential before venting it harmlessly out the exhaust muffler. Compressor pump oils use demulsifiers that intentionally separate water from oil, causing free liquid water to pool directly against polished steel pneumatic vanes.
Seal compatibility also depends heavily on specific chemical formulations. Pneumatic tools rely on soft nitrile, polyurethane, and fluorocarbon O-rings to seal reversing valves, trigger stems, and air regulator dials. Certain compressor oils contain anti-wear compounds or synthetic esters that can cause soft pneumatic rubber to swell, soften, or harden prematurely. Once an internal O-ring loses elasticity or expands beyond its groove, tools suffer from internal blow-by leaks and erratic throttle modulation.
Mechanical Consequences of Using Compressor Oil in Air Tools
Introducing thick pump oil into pneumatic equipment triggers several immediate mechanical symptoms that degrade shop productivity. Operators usually notice a distinct drop in tool speed and a noticeable hesitation when pulling the trigger. The tool motor may feel sluggish, requiring manual spinning of the spindle or drive socket before the vanes catch compressed air. This sluggishness occurs because heavy oil clings to rotor slots, preventing spring-loaded or centrifugal vanes from extending fully against the cylinder wall.
Exhaust clogging quickly follows the introduction of improper fluids into pneumatic equipment. As thick oil mixes with ambient dust, metal shavings, and line moisture, it forms a sticky paste inside the sintered bronze or mesh exhaust silencer. This restriction creates high backpressure inside the tool body, choking air exhaust and drastically reducing available running power. Operators often mistake this backpressure choke for an air compressor pressure switch malfunction or undersized air line diameter.
Extended operation with incorrect fluids can cause permanent mechanical damage to rotating assemblies. When heavy oil fails to mist properly, friction heats the sliding edges of composite fiber or phenolic motor vanes. Overheated vanes warp, chip, or score the polished inner walls of the tool cylinder sleeve. Replacing a scored pneumatic motor cylinder often costs more than purchasing a brand-new replacement tool, making fluid mistakes surprisingly expensive over time.
The Role of In-Line Lubricators and Moisture Separation
Automating oil delivery through continuous pneumatic systems requires careful equipment selection and proper fluid viscosity. Compact devices like the THB mini lubricator or OZXNO automatic mini in-line oiler use venturi pressure drops to siphon lubricant into the active airstream. These precision metering orifices are calibrated strictly for light ISO 22 to ISO 32 fluids that flow freely through tiny adjustment needles. Pouring heavy compressor oil into an in-line oiler reservoir clogs the internal metering siphon and completely starves downstream equipment of lubrication.
Moisture filtration hardware plays an equally critical role in protecting pneumatic tools from compressor fluid contamination. Crankcase pumps naturally carry small amounts of aerosolized pump oil into the air tank and discharge piping. Installing a dedicated moisture and oil separator, such as the NEIKO water and oil separator, removes residual pump oil mist and condensed moisture before air enters flexible supply hoses. This separation guarantees that downstream tools receive only clean, dry air alongside their intended pneumatic lubricant.
Draining compressor tanks regularly works hand-in-hand with inline filtration to maintain dry line conditions. As outlined in our detailed process on removing condensation from your air compressor, daily tank draining prevents corrosive water from overwhelming in-line filters. Keeping water out of the air supply prevents emulsifying additives in your air tool oil from depleting prematurely. Clean, dry air combined with proper inline lubrication extends the operational lifespan of all connected workshop equipment.
Emergency Alternatives and What to Do If Wrong Oil Was Used
Operators occasionally face emergency situations where a specialized air tool oil bottle runs completely dry during an active project. If you find yourself stranded without dedicated pneumatic lubricant, light non-detergent hydraulic fluid or lightweight spindle oil can serve as a short-term temporary substitute. You should avoid motor oil, automatic transmission fluid, thick compressor oil, and penetrating sprays like standard solvent penetrants. Penetrating sprays dissolve existing lubricating films, evaporate rapidly, and destroy delicate rubber O-rings within hours.
Accidentally putting heavy compressor oil into your pneumatic equipment does not mean the tool is permanently ruined if addressed promptly. The best corrective step involves flushing the tool motor with a light solvent or dedicated cleaning agent designed for pneumatic mechanisms. Adding five to ten drops of a cleaning lubricant like Marvel Air Tool Oil directly into the air inlet helps break down heavy petroleum residues. Running the tool unloaded at low pressure for thirty seconds allows the solvent action to loosen thick sludge and vent it through the exhaust.
After flushing the heavy residue, wipe away contaminated exhaust discharge with a shop rag to prevent staining your workspace. Follow the flushing procedure by administering several drops of quality air tool oil, such as CRAFTSMAN air tool oil or Freeman PTTO lubricant, directly into the intake. Cycle the tool again at low speed to establish a fresh protective film across all internal vanes and rotor surfaces. Repeating this flush process restores original rotational speed and prevents long-term varnish buildup inside delicate mechanical tolerances.
Recommended Lubrication Routines for Pneumatic Equipment
Establishing a consistent daily lubrication routine prevents wear and keeps pneumatic tools operating at maximum output. For tools without dedicated in-line lubricators, add three to five drops of genuine pneumatic oil into the air inlet fitting before each work session. If you run high-consumption tools like die grinders, impact wrenches, or orbital sanders continuously throughout the day, reapply two drops every four hours of continuous operation. This steady replenishment replaces oil droplets carried away by escaping exhaust air.
Storage procedures also require deliberate lubrication to prevent internal corrosion during seasonal downtime. Moisture trapped inside compressed air lines can settle against bare steel cylinders while tools hang on shop pegboards or sit in metal toolboxes. Before storing any pneumatic nailer, ratchet, or grinder for extended periods, place six drops of air tool oil into the air inlet and trigger the tool briefly. This step coats bare metal surfaces with a protective barrier that resists moisture pitting and internal rust formation.
Selecting the right bottle size and applicator tip makes routine maintenance fast and mess-free. Pint-sized shop bottles like Lucas Oil air tool lubricant provide economical bulk supplies for busy workshops, while smaller four-ounce bottles fit easily inside mobile toolboxes. Squeeze bottles with precision dropper tips allow mechanics to direct oil precisely past quick-connect fittings into the air passage without spilling fluid onto exterior grip surfaces. Keeping dedicated pneumatic oil within arm’s reach ensures maintenance occurs reliably before every pneumatic task.
Summary Takeaway: Keeping Compressors and Tools Properly Separated
Compressor pump oil belongs strictly in compressor pump crankcases, and air tool oil belongs strictly in pneumatic air motors. Conflating the two products risks robbing your pneumatic tools of torque, gumming internal exhaust mufflers, and deteriorating flexible synthetic seals. High-viscosity pump fluids cannot provide the fine misting action and moisture emulsification that rapid air motor vanes require. Investing in dedicated pneumatic lubricants guarantees that each component in your air system operates under optimal boundary protection.
Pairing proper lubrication with diligent line filtration creates a durable, high-performing pneumatic workshop environment. Combining a quality inline moisture separator with daily inlet oiling safeguards expensive impact wrenches, nail guns, and sanders against premature wear. Maintaining clean air delivery and using purpose-built fluids ensures your pneumatic setup delivers maximum power, dependable torque, and decades of reliable service.
About the author
Glenda Taylor has extensive experience in residential construction, remodeling, home improvement, and tool use. Her practical approach to equipment evaluation focuses on usability, performance, safety, and value—helping DIYers and workshop users make better-informed decisions about compressors and related tools.