
How Much to Replace Central Air Compressor: Practical Repair and Cost Guide for 2026
Wondering how much to replace central air compressor in your shop? Evaluate pump rebuild costs, valve plate replacements, and hardware options for October 2026.
 By Clint DeBoer
Updated October 7, 2026

Dynamic pressure loss and sluggish tank recovery times often indicate mechanical failure within a workshop compressed air pump. When a shop pump begins short-cycling, overheating, or leaking air past worn cylinder heads, pneumatic tools like impact wrenches and paint sprayers quickly suffer from severe air starvation. Determining how much to replace central air compressor equipment depends heavily on whether you need a complete pump assembly or targeted internal rebuild components. Many garage mechanics and workshop owners jump to replacing entire utility units when simple valve fatigue is the true culprit. Addressing localized component wear early protects downstream air delivery lines and prevents catastrophic motor burnout.
Standard central workshop pumps, such as Central Pneumatic utility models, rely on internal reed valves that endure intense cyclic heating and vibration. Replacing smaller components like reed valve plates, rigid aluminum exhaust tubes, or restrictive air intake silencer filters restores factory compression at a fraction of whole-unit replacement expenses. Knowing when to swap an inexpensive valve kit versus investing in an entirely new cast iron pump head keeps your garage operational without unnecessary downtime. By inspecting the pump assembly systematically, you can accurately budget for critical hardware fixes and maintain optimal dynamic line CFM across all your shop pneumatic attachments.
| Award | Product | ACR Score About ACR ScoreThe ACR Score is our own rating from 0 to 10, based on performance, design and build, ease of use, and value. It reflects independent research and is never influenced by manufacturers, retailers, or affiliate commissions. Learn more › | |
|---|---|---|---|
| Best Overall |
ZYAMY Air Compressor Reed Valve Plate Kit
|
9.1/10 | Buy |
| Best Value |
 WHYHKJ Air Compressor Valve Plate Kit |
8.6/10 | Buy |
| Best Budget |
 ZHONG AN 1/2" PT (20mm) Metal Air Compressor |
8.4/10 | Buy |
| Best Premium |
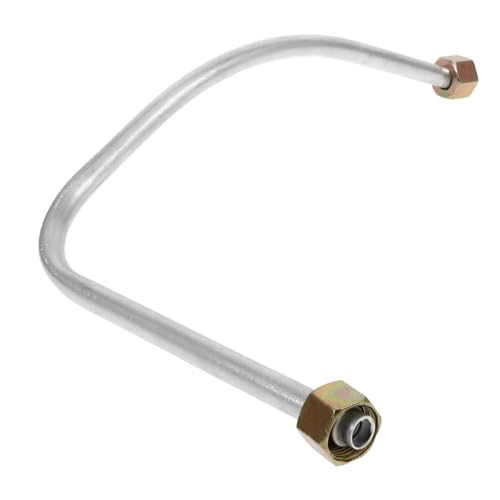 JECOMPRIS 16mm Aluminum Air Compressor Exhaust |
8.3/10 | Buy |
ZYAMY Air Compressor Reed Valve Plate Kit
Built for small oiled air pumps, this ZYAMY replacement set uses durable cast-iron components to help restore air compressor operating efficiency. The included tongue and V-plates feature a spring-loaded design engineered to withstand thermal fatigue and creep damage.
Pros
- Sturdy cast-iron build resists wear and tear
- Simple structure allows straightforward installation
- Includes both tongue valve plate and V-plate
- Spring-loaded design withstands high thermal fatigue
Cons
- Designed specifically for small oiled air pumps
- Restricted to tongue and V-plate configurations
WHYHKJ Air Compressor Valve Plate Kit
Built for repairing worn central pneumatic units, this replacement set provides cast iron tongue and V-shaped plates to help restore operating efficiency. The heavy-duty metal build holds up against mechanical creep along with low and high cycle thermal fatigue.
Pros
- Durable cast iron construction
- Resists thermal fatigue and creep stress
- Simple configuration allows straightforward installation
- Helps recover lost compressor pumping efficiency
Cons
- Restricted to tongue and V-shaped valve assemblies
ZHONG AN 1/2" PT (20mm) Metal Air Compressor
The ZHONG AN 1/2-inch PT (20mm male thread) Intake Silencer Filter pairs a sturdy metal housing with sound-absorbing paper media to quiet compressor suction noise and block airborne dust. It is an affordable, durable replacement for garage DIYers and workshop owners dealing with broken or brittle plastic factory intake filters.
Pros
- Heavy-duty metal canister withstands workshop bumps and high cylinder head temperatures
- Sound-dampening paper media noticeably softens harsh intake thump and suction resonance
- Protects compressor cylinders, piston rings, and reed valves from abrasive airborne debris
- Straightforward installation on compressors and blowers with matching 20mm intake bungs
Cons
- Uses a 1/2-inch PT (20mm diameter) male thread, which may require a thread adapter for compressors with domestic 1/2-inch NPT ports
- Internal paper filter element is non-washable and must be replaced as it collects fine shop dust
- Single-piece package does not include spare filter elements or pipe thread adapters
JECOMPRIS 16mm Aluminum Air Compressor Exhaust
A pre-bent rigid aluminum discharge tube engineered for metric piston air compressors with 16mm ports and 1HP to 3HP motors. Ideal for garage mechanics and DIYers needing a direct bolt-on replacement to stop discharge leaks between the pump and check valve.
Pros
- Pre-shaped 7-bend geometry clears compressor motor housings easily without custom bending tools
- Lightweight, heat-resistant aluminum construction withstands vibration and thermal discharge
- Integrated 2.00cm hex nuts allow straightforward wrench installation in under ten minutes
- Restores airtight transfer between pump and tank to prevent unnecessary motor strain
Cons
- Strict metric sizing will not fit standard 1/2-inch or 3/4-inch NPT compressor ports
- Rigid aluminum construction offers minimal flexibility if pump and check valve alignment is off
- Requires careful caliper measurement of existing pump ports prior to purchase to ensure a correct fit
Evaluating Central Workshop Air Compressor Replacement Costs and Rebuild Options
Assessing the total expense to repair or replace a central workshop air compressor requires identifying the exact mechanical bottleneck in your pneumatic supply system. While acquiring an entirely new stationary compressor pump or complete motorized tank unit can represent a substantial commercial investment, individual mechanical failures are often confined to specific sub-assemblies. Component breakdowns frequently stem from cracked cylinder reed valves, split aluminum discharge pipes, or clogged intake breathers that can be serviced independently at minimal expense. Pinpointing these localized wear points early prevents shop owners from prematurely discarding perfectly serviceable compressor machinery.
Complete Pump Assembly Replacement Versus Component-Level Overhauls
Investing in a brand-new pump head becomes necessary when continuous friction scorches cylinder walls or scores crankshaft bearings beyond recovery. Replacing an entire single-stage or two-stage central utility pump typically incurs significant equipment costs alongside several hours of workshop plumbing labor. Mechanics must account for unbolting the motor carriage, aligning drive pulleys, and retensioning the drive belt to match exact flywheel specifications. For small commercial setups and home garages, swapping the complete pump makes sense primarily when catastrophic crankcase failure or thermal seizing has compromised structural cast iron housings.
Targeted component replacement addresses the most common points of pneumatic pressure decay without discarding functional castings and electric motors. Inexpensive wear items, including cast iron gasket kits, reed tongue plates, and unloader fittings, restore volumetric efficiency when the underlying piston cylinders remain structurally sound. Choosing to rebuild the cylinder head yourself significantly reduces expenditure compared to commercial machinery replacement. A targeted repair approach keeps your workshop air system running at full dynamic pressure while preserving existing hardline plumbing and mounting brackets.
Diagnosing Valve Plate Wear and Thermal Reed Valve Fatigue
Piston compressors depend on thin, flexible spring-steel reeds to regulate the intake and exhaust cycles of each compression stroke. Over extended operating hours, these reed valves experience extreme low-cycle and high-cycle thermal fatigue alongside mechanical creep damage from intense cylinder head temperatures. When a reed valve cracks, warps, or accumulates heavy carbon fouling, compressed air leaks back into the cylinder or vents through the intake port instead of filling the storage receiver. You can readily detect this condition when the pump runs continuously without building pressure or when hot air backflows through the intake muffler.
Rebuilding the valve assembly requires matched components that mirror factory dimensions to maintain proper combustion-free seal pressure. Replacement sets, such as the ZYAMY 1 Set Air Compressor Parts Small Oiled Air pump kit, provide tongue-shaped valve plates, V-plates, and durable cast iron gaskets specifically designed for Central Pneumatic and compatible oiled compressor pumps. The durable cast iron cover gasket seals high-pressure cylinder passages securely, preventing dangerous micro-leaks between adjacent chambers. Installing fresh valve plates restores rapid tank recovery times and stops the continuous pump cycling that leads to electric motor overheating.
Valve Kit Compatibility and Head Gasket Rebuilding Expenses
Budgeting for a cylinder head overhaul remains remarkably economical compared to purchasing complete machinery assemblies. Hardware sets like the WHYHKJ Air Compressor Replacement Parts Central pneumatic kit supply the critical internal metal plates and gaskets needed to refresh worn small-capacity pumps. These kits provide direct replacement tongue valve plates and V-shaped plates engineered to resist repetitive cyclic shock under heavy workshop workloads. Because these metal parts are engineered for standard small oiled pump heads, they allow mechanics to execute routine maintenance without specialized machining equipment.
Installing new reed assemblies requires thorough cleaning of the valve seat mating surfaces to ensure an airtight seal. Any lingering carbon deposits, oil sludge, or degraded gasket residue will prevent the flexible tongue plates from seating flat against the cast plate orifice. Technicians should carefully clean the valve deck with a non-chlorinated solvent and inspect the cast iron plate for warping before torquing head bolts down evenly. Restoring these internal seals eliminates pressurized blow-by and ensures downstream lines receive full cubic feet per minute at rated operating pressure.
Exhaust Tube Ruptures and High-Temperature Transfer Line Replacement
Discharge piping between the compressor cylinder head and the tank check valve operates under brutal mechanical conditions. These lines endure intense thermal output from one to three horsepower motors while absorbing severe vibration from reciprocating pistons. Over time, rigid factory tubes can work-harden, crack near flare fittings, or develop pinhole leaks along stress points. A fractured exhaust line forces the compressor motor to run continuously while venting valuable pressurized air directly into the workshop atmosphere.
Replacing a broken transfer line requires a purpose-built conduit capable of managing rapid heat dissipation without kinking. The JECOMPRIS Air Compressor Hose Exhaust Tube offers a pre-bent seven-shape rigid aluminum build engineered to route safely around motor housings. Measuring 25.50 by 18.50 centimeters with a 400-millimeter transfer span, it features an unobstructed internal wall designed to eliminate pressure drop between the pump head and manifold check valve. Buyers must measure pump discharge ports carefully, as this pipe features a specific dual-port configuration with a 16mm internal diameter port, an 11mm internal step-hole, and 2.00cm outer diameter hex nuts that will not match standard half-inch pipe fittings.
Intake Silencer Filtration and Contaminant Prevention Costs
Clean intake air is vital for extending the operational lifespan of internal piston rings, valve plates, and cylinder sleeves. Workshop environments generate abrasive sawdust, metal shavings, and overspray mist that quickly degrade reciprocating components if drawn directly into the pump crankcase. An obstructed or damaged intake muffler starves the pump of necessary atmospheric volume, forcing longer run times and elevated cylinder head temperatures. Replacing intake silencer filters periodically is an inexpensive maintenance protocol that prevents premature pump failure.
Intake accessories like the ZHONG AN 1/2″ Thread Male Thread Diameter 20mm Air compressor silencer filter utilize a robust metal housing combined with sound-absorbing filter paper. Featuring a standard 1/2-inch PT male thread with a 20mm diameter, this unit muffles harsh intake suction noise while trapping airborne particulates before they enter the valve deck. Manufacturers recommend replacing paper filter elements monthly in dusty workshop conditions to maintain unimpeded airflow. Maintaining a clean intake filter reduces thermal strain across the pump head and protects newly installed reed valves from abrasive scouring.
Labor Expenses Versus DIY Workshop Compressor Overhauls
Hiring a commercial pneumatic technician or industrial repair service introduces substantial labor expenses that often exceed the purchase price of small shop compressors. Service centers typically charge minimum diagnostic bench fees and standard hourly rates that quickly escalate during valve teardowns or head resurfacing. For large stationary central compressors wired into 240-volt three-phase supplies, professional labor guarantees proper electrical disconnects and certified ASME pressure vessel compliance. However, for utility garage compressors running five-gallon to fifty-liter receiver tanks, professional service fees rarely justify the overall expenditure.
Executing a DIY pump overhaul requires only basic hand tools, such as metric sockets, a torque wrench, calipers, and a scraper for gasket cleanup. Because replacement reed valve kits and pre-bent exhaust tubes bolt directly onto existing compressor heads, most garage owners can complete a rebuild in under an hour. Taking the DIY route avoids lengthy repair turnaround times and keeps overall maintenance expenses confined entirely to component hardware. Careful attention to bolt torque sequences and thread engagement ensures reliable sealing without outside labor invoices.
Diagnostic Protocol Before Committing to System Replacement
Before purchasing replacement hardware or condemning a complete compressor pump, technicians must isolate the exact source of air loss. Begin by allowing the compressor to build maximum tank pressure until the pressure switch trips the unloader valve. Listen closely around the cylinder head, unloader line, and tank check valve for faint hissing sounds that indicate high-pressure leakage. Applying a non-corrosive soapy water bubble solution around pipe connections, head gaskets, and hex nuts will immediately expose escaping air bubbles without risking electrical shock.
If the compressor struggles to reach cut-out pressure or vents air continuously through the unloader valve when stationary, inspect the tank check valve before opening the pump head. A fouled check valve allows tank air to leak back into the unloader tube, mimicking a broken head gasket or defective reed valve. Furthermore, check the unloader line and pressure switch differential settings to verify proper mechanical cycling. Isolating external fitting leaks first prevents unnecessary pump disassembly and pinpoints exactly which sub-assemblies require replacement.
When external line fittings and tank check valves pass inspection, monitor the pump recovery speed against manufacturer timing benchmarks. An uncharacteristically slow pressure rise accompanied by an excessively hot cylinder head confirms internal valve leakage or worn compression rings. At this stage, disconnecting power, depressurizing the receiver tank completely, and removing the cylinder head bolts allows direct visual inspection of the reed plates. Visible cracks, broken tongue tabs, or heavy carbon buildup indicate that installing a replacement reed valve kit will successfully restore pump operation.
Mitigating Thermal Fatigue and Line Vibration in Shop Air Drops
Excessive heat buildup and harsh vibrations represent leading causes of premature valve failure and cracked exhaust tubes in central workshop compressors. When air compressors operate continuously beyond their rated duty cycle, cylinder temperatures rise rapidly, accelerating low-cycle thermal fatigue across internal spring valves. High operating temperatures also degrade synthetic pump oil, forming varnished carbon crusts that wedge reed valves open and compromise cylinder compression. Operating within recommended duty cycles allows adequate cool-down periods that extend the physical life of internal metal components.
Vibration management is equally critical when routing rigid transfer lines and connecting stationary compressors to workshop air manifolds. Heavy piston reciprocation creates harmonic oscillation that can loosen aluminum hex nuts or induce fatigue cracks in rigid transfer tubes. Mounting the compressor on dense rubber vibration isolation pads isolates pump motion from rigid workshop walls and flooring. Coupling the tank discharge port to your rigid workshop air distribution network via a flexible braided whip hose prevents vibration transfer that could otherwise crack downstream pneumatic filters and regulators.
Post-Repair Verification and Pressure Calibration Procedures
Once fresh replacement parts are securely bolted into place, conducting a disciplined pressure calibration procedure ensures leak-free workshop operation. Before reconnecting electrical power, double-check that all cylinder head fasteners are torqued down evenly in a crisscross pattern to prevent warping the cast iron plate. Ensure the new aluminum exhaust tube hex nuts are tightened securely without cross-threading the precision metric ports. Reattach the intake silencer muffler firmly to guarantee that only clean, filtered air enters the newly rebuilt cylinder head.
Power on the compressor unit and observe the tank pressure gauge as the pump climbs toward its preset cut-out pressure threshold. Verify that the unloader valve actuates with a sharp burst of exhaust air when the motor shuts off, indicating that head pressure has successfully vented. Allow the pressurized receiver tank to sit idle under full pressure for several hours to confirm that static pressure holds steady without decaying. Verifying these operating conditions guarantees that your targeted component replacement has completely restored factory pneumatic performance at a minimal overall investment.
Selecting the most economical repair path for your central workshop air compressor depends on accurately identifying whether internal valve fatigue or external line fractures are causing system pressure loss. By utilizing cost-effective reed valve kits, rigid aluminum transfer tubes, and high-efficiency intake silencer filters, you can successfully bypass the substantial expense of replacing entire pump assemblies. Regular inspection of these critical wear components preserves high CFM delivery, prevents unexpected tool starvation, and ensures your pneumatic workshop system performs dependably through years of demanding service. Taking a methodical, component-level approach to compressor maintenance keeps operating expenses low while providing the reliable air volume required for all your workshop projects.
About the author
Clint DeBoer is an experienced tool-industry specialist with decades of involvement in technical media, hands-on product evaluation, and testing methodology. His focus on performance, practical usability, and data-driven comparisons makes his expertise highly relevant to professional air compressors, pneumatic tools, and workshop equipment.